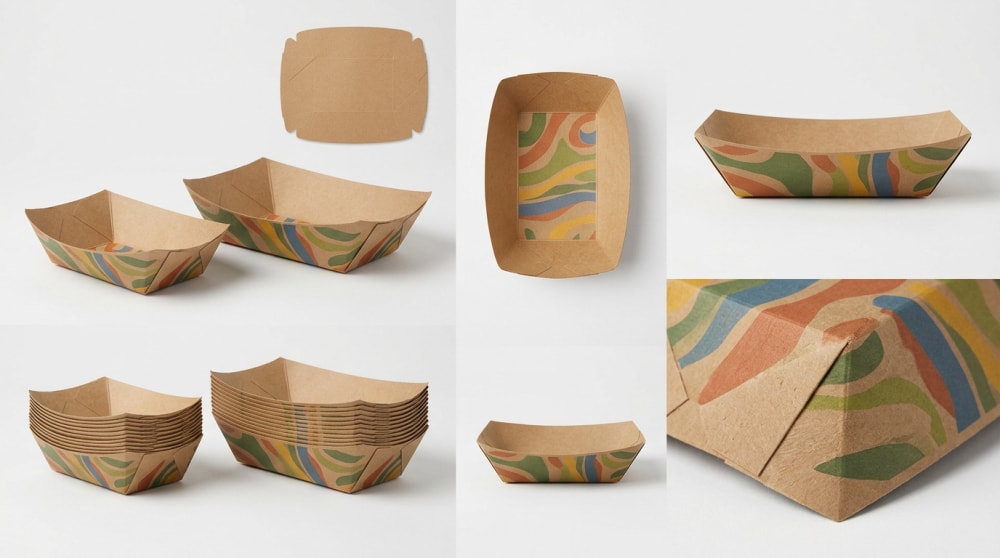
Canada Guide to Approving Kraft Concession Trays
Quick Answer: Set Measurable Quality Standards for Fast-Service Kraft Concession Trays

For Canadian venue operators, food-service distributors, stadium caterers and quick-service chains, kraft concession trays should be approved against a written specification rather than appearance alone. A tray that looks acceptable in a showroom can still fail during a short, high-volume service peak when it carries hot poutine, fries, nachos, chicken tenders, mini donuts or sauced snacks.
The practical approval standard should cover tray dimensions, board weight, coating coverage, forming accuracy, glue or fold integrity, print registration, odour, food-contact documentation, carton packing and real-use performance. Before bulk production begins, the buyer and supplier should agree on an approved reference sample, an inspection plan, defect classifications, acceptance limits, retained samples and a remedy for non-conforming production.
For fast-service kraft concession trays, the most important question is simple: can every tray open quickly, hold the specified food portion, resist grease and moisture long enough for consumption, stack efficiently, and maintain the brand presentation expected at busy Canadian events? The approval process should prove this under realistic operating conditions, not only through visual inspection.
Recommended approval sequence
- Confirm food type, fill weight, serving temperature, holding time and intended tray size.
- Approve a white sample or printed pre-production sample with signed specifications.
- Set measurable tolerances for dimensions, basis weight, coating, print and carton count.
- Inspect random cartons from different locations within the finished batch.
- Conduct real-food trials using hot, greasy, salty and moist menu items.
- Record defects with photos, lot numbers and retained physical samples.
- Define replacement, credit, rework or rejection rules in the purchase order.
Canadian buying context
Demand for disposable food trays rises sharply around hockey games, music festivals, university events, summer fairs and winter indoor venues. Buyers serving Toronto, Vancouver, Montréal, Calgary, Edmonton, Ottawa and Halifax often need packaging that performs consistently despite different distribution routes, humid kitchens, refrigerated storage areas and compressed serving windows. Import orders arriving through Vancouver, Prince Rupert, Montréal or Halifax should include lot identification and inspection records before onward delivery to regional warehouses.
| Approval item | What to measure | Typical control point | Why it matters in rapid service |
|---|---|---|---|
| Length and width | Finished inside and outside dimensions | Agreed tolerance, commonly ±2 mm | Ensures portion fit, stacking and dispenser compatibility |
| Tray depth | Wall height at all sides | Specified minimum depth | Reduces spillage of fries, toppings and sauces |
| Paperboard weight | Grams per square metre or tray weight | Target value with agreed tolerance | Supports stiffness and consistent food carrying capacity |
| Coating consistency | Coverage, smoothness and exposed-board checks | No uncoated food-contact zones | Helps manage grease, moisture and staining |
| Forming quality | Fold alignment, glued points and corners | No opening seams or crushed walls | Allows fast loading without tray collapse |
| Print tolerance | Colour, registration and legibility | Approved proof and Pantone reference | Protects sponsor, venue and restaurant branding |
| Carton quantity | Units per inner pack and master carton | Declared count verified | Improves inventory accuracy during event replenishment |
The table above creates a workable starting point, but values should be tailored to the tray format, food load and service time. A shallow fry boat requires different controls from a deep tray used for loaded nachos or poutine.
How to Inspect Kraft Concession Trays Before Approval

Inspection should start with the approved product specification and not with an unstructured visual review. The specification should identify the tray code, artwork revision, board type, coating type, size, target weight, pack count, lot format and test conditions. Canadian buyers should also confirm which food-contact and sustainability documents are needed for their province, customer program or retail channel.
Build an inspection plan before shipment
A useful plan checks samples from multiple master cartons, not only the top carton nearest the loading door. Select cartons from the front, centre and rear of pallets where possible. For a first order, a new artwork version, a new material grade or an urgent event program, increase the sample size and consider a third-party pre-shipment inspection.
During incoming inspection in Canada, allow trays to acclimatize to the warehouse environment before performing critical dimensional tests. Paper packaging can respond to temperature and humidity changes. This does not excuse production defects, but it helps the team distinguish transit or storage effects from genuine forming and material failures.
| Inspection stage | Sample action | Primary checks | Approval record |
|---|---|---|---|
| Artwork review | Examine digital proof | Logo position, copy, barcode, colours | Signed PDF revision |
| Structure review | Evaluate white sample | Size, folds, capacity, stacking | Sample code and measurements |
| Functional approval | Test production-intent sample | Heat, grease, moisture, handling | Test sheet and photos |
| Pre-production proof | Review printed sample | Registration, finish, readable graphics | Signed colour approval |
| In-process verification | Check first-off production units | Forming, glue, weight, print | Factory QC record |
| Final random inspection | Open selected cartons | Defects, count, packing, lot code | Final inspection report |
| Receiving inspection | Check delivered stock | Transit damage, odour, count, performance | Warehouse receiving report |
For buyers sourcing kraft food boats and concession trays, the product drawing should show internal dimensions as well as outside dimensions. The inside footprint determines whether a standard portion of fries, popcorn shrimp or loaded snacks fits without overflow.
Market outlook for Canadian concession service
Canadian food-service packaging demand is influenced by event attendance, travel, tourism, takeaway consumption and the continued need for efficient counter service. Kraft trays remain relevant because they are lightweight, printable, simple to store and available in formats suited to fries, bakery snacks, fried foods and shareable appetizers. The growth estimate below is an indicative planning model for concession-tray purchasing activity rather than a guarantee of market performance.
Define Critical, Major and Minor Defects for Kraft Concession Trays

Defect definitions prevent avoidable disputes. A supplier may consider a small print shift cosmetic, while a venue operator may consider it unacceptable if it cuts through a sponsor logo. Similarly, a slight crease may be minor on an outer wall but critical if it weakens a corner that can leak sauce or spill hot food.
Critical defects create a food-safety, consumer-injury, legal-compliance or unusable-product risk. Major defects interfere with normal food service, structure, food containment or brand presentation. Minor defects do not materially affect intended use but should remain within an agreed appearance standard.
| Defect class | Example | Operational effect | Recommended disposition |
|---|---|---|---|
| Critical | Foreign material or unacceptable odour | Potential food-contact and consumer concern | Reject affected lot; investigate immediately |
| Critical | Wrong food-contact material or missing mandatory information | Compliance risk | Hold shipment and verify documentation |
| Critical | Open seam causing food to fall through | Unsafe or unusable during service | Reject affected production batch |
| Major | Tray wall collapse under specified food load | Spills and slow service | Reject or sort according to agreed AQL |
| Major | Visible coating gaps in food-contact area | Grease soak-through or staining | Hold lot for functional testing |
| Major | Print registration beyond approved limit | Branding or promotional message impaired | Rework, credit or reject as agreed |
| Minor | Small non-food-contact scuff mark | Limited cosmetic effect | Accept within stated limit |
| Minor | Slight variation in natural kraft shade | No functional impact | Accept if within approved sample range |
The key is to agree not only on names but on consequences. A purchase order should state whether any critical defect causes automatic rejection, whether major defects are controlled by an agreed acceptance quality limit, and how minor defects are recorded. For event packaging, the operational cost of failure can exceed the unit cost of the trays, particularly where a concession stand has limited storage and no time to re-pack product.
Industry demand by food-service segment
Different Canadian food-service segments place different demands on kraft tray performance. Stadiums prioritize speed and bulk replenishment, while food trucks may prioritize compact storage and resistance to sauced foods. The following comparison can help purchasing teams prioritize validation tests.
Compare the Approved Sample With Random Cartons of Kraft Concession Trays
The approved sample is the physical and documented reference for production. It should carry a revision number, date, product code and signatures or written approval from both parties. For branded trays, retain the approved digital artwork together with the physical sample because colour and structural appearance must be evaluated as a combined result.
When checking random cartons, compare trays directly with the signed sample under consistent lighting. Evaluate natural kraft shade, surface finish, fold shape, tray opening, print position and overall stiffness. Do not compare one random tray with another random tray; compare both to the approval master.
Carton selection and lot traceability
Each master carton should show a product code, production date or lot number, quantity and destination mark. If a problem is identified at a warehouse in Mississauga, Surrey, Laval or Calgary, traceability allows the buyer to isolate the relevant pallet or lot instead of placing all inventory on hold.
A practical plan may select cartons across pallets and then pull units from the top, middle and bottom of each carton. This approach improves the chance of finding variation caused by packing, compression or process drift. It is especially useful for long sea-freight journeys into Vancouver or Montréal, followed by domestic transport across Canada.
| Carton comparison point | Approved sample standard | Random-carton check | Action if variation appears |
|---|---|---|---|
| Tray opening | Opens easily to intended shape | Open 10 consecutive units | Record sticking, cracking or distorted folds |
| Corner formation | Even, secure and symmetrical | Inspect all corners sampled | Classify weak or open corners as major |
| Board stiffness | Matches retained standard | Hand-feel and loaded comparison | Confirm with tray-weight checks |
| Grease barrier | No visible exposed area | Inspect inside base and walls | Conduct food or oil challenge test |
| Print appearance | Matches signed proof | Check logo, colour and registration | Measure or photograph deviation |
| Pack count | Declared quantity per sleeve/carton | Count selected sealed packs | Report shortage by lot and carton |
| Carton condition | Dry, closed and legibly marked | Check crush, moisture and damage | Separate transit damage from factory defect |
The approved sample should not be treated as a vague visual target. It becomes a controlled approval record that links the buyer’s requirements to routine production and final inspection.
Stress-Test the Pack for Rapid Snack Service During Short Demand Peaks
Real-use testing is essential for concession packaging. A tray may pass dry handling tests yet soften quickly under hot gravy, cheese sauce, oil or steam. Test the products that customers actually buy, using the intended serving weight and typical holding period. Include staff handling: filling, passing across the counter, carrying to seats, placing on a lap or tray table, and disposal.
Suggested food trials
- Hot fries with salt and ketchup, held for 15 and 30 minutes.
- Poutine with fries, gravy and cheese curds, checked for base softening and corner leakage.
- Loaded nachos with cheese sauce, salsa and protein, checked for oil and moisture migration.
- Chicken wings or tenders with sauce, checked for grease strike-through and fold stability.
- Mini donuts or churros, checked for oil resistance and print transfer.
- Cold snack combinations, checked for condensation and stack separation.
Use the test time that reflects actual conditions. A tray for immediate counter consumption may need only a 15-minute performance target. A tray used at arenas, outdoor festivals or drive-in events may need to hold food for 30 minutes or longer. The buyer should specify whether slight staining is acceptable, whether visible grease on the outside is a failure, and whether the loaded tray must remain stackable.
Future trends for 2026 and beyond
From 2026 onward, Canadian buyers are likely to place more emphasis on material transparency, practical end-of-life claims, fibre sourcing, reduced unnecessary plastic, lighter-weight structures that still meet performance targets, and digital batch traceability. Sustainability claims should be tied to the exact material construction and local waste-stream reality rather than used as generic marketing language.
Technology will also shape purchasing. Digital proofing, barcode-linked lot records, camera-assisted print inspection, automated weight checks and shared approval files can shorten the distance between a production line overseas and a distribution team in Canada. The strongest programs will combine sustainability objectives with repeatable performance testing, not trade one for the other.
Check Dimensions, Weight and Coating Consistency for Kraft Concession Trays
Dimensions, board weight and coating are measurable indicators of tray consistency. For every format, specify the nominal length, width, depth, acceptable tolerance and test method. If capacity matters, state the test fill volume or food portion weight rather than relying only on a product name such as “medium fry tray.”
Paperboard weight can be checked using a defined sample area or through finished-tray weight when the tray shape and board blank are fixed. Finished-tray weight is useful for receiving inspection because it is quick, although it should be interpreted with the approved construction and coating specification in mind.
| Test characteristic | Method | Example acceptance criterion | Inspection frequency |
|---|---|---|---|
| Inside length | Digital caliper or ruler | Nominal size within agreed ±2 mm | First article and final sample |
| Inside width | Digital caliper or ruler | Nominal size within agreed ±2 mm | First article and final sample |
| Wall depth | Depth gauge or ruler | At or above specified minimum | Per sampled carton |
| Finished tray weight | Calibrated scale | Within agreed target tolerance | At least 10 units per selected lot |
| Coating appearance | Visual examination under standard light | No bare spots, pooling or pinholes | Per sampled carton |
| Grease holdout | Specified food or oil exposure | No external soak-through at set time | Each approval or material change |
| Print registration | Measure against artwork marks | Within agreed registration tolerance | First-off and final sample |
Coating consistency should be inspected visually and functionally. Visual checks can identify streaks, pinholes, uneven gloss or uncoated areas. Functional tests determine whether the tray resists the specified menu item. A well-designed inspection plan uses both methods because a coating can look smooth while still underperforming with hot oil or sauce.
Document Failure Photos and Retained Samples for Kraft Concession Trays
Clear documentation makes defect resolution faster and fairer. When a failure occurs, photograph the full tray, the close-up defect, the carton label, the lot code and the food test setup. Include a ruler or measurement reference in dimension-related images. For leakage or grease strike-through, photograph the tray at the agreed time intervals and record food temperature, fill weight and holding time.
Retain both a buyer-approved sample and samples from each inspected batch. Store them in labelled bags or boxes away from sunlight, moisture and food contamination. The label should include product code, artwork revision, supplier lot, inspection date, inspector name and purchase order number.
Case example: arena poutine tray validation
A hypothetical concession distributor supplying an arena program in Ontario selected a kraft tray for poutine. The first sample looked satisfactory with dry fries but softened at the base after 18 minutes when filled with hot gravy. The team documented the result, retained the failed tray and compared it with the approved white sample. The supplier adjusted the material and barrier construction, then repeated the test using a defined portion weight and 30-minute hold. The revised sample met the agreed functional criteria before bulk production.
The lesson is not that every tray needs the heaviest possible board. It is that the structure and barrier must match the food, fill weight and real service window.
Case example: branded festival fry boats
For a seasonal festival order routed through Vancouver, a buyer noticed that one carton group had logo placement drifting closer to the tray edge. The product remained usable, but the sponsor mark was visibly inconsistent. By using the signed printed sample, carton lot codes and photo evidence, the parties identified the affected production range. The remedy was agreed before the next release, avoiding a repeat problem during the following event season.
Set a Replacement Rule Before the Purchase Order
The purchase order should define what happens if the supplied trays fail the agreed specification. This is particularly important for Canadian buyers with fixed event dates, limited warehouse space and non-refundable venue commitments. A remedy clause should state the inspection window, required evidence, defect threshold, response time and available outcomes.
Possible remedies include replacement production, replacement credit on a future order, partial credit, rework where feasible, sorting at supplier cost, or rejection of affected goods. The remedy should reflect the severity, the amount of usable stock, the timing of the claim and whether the defect affects food safety, service function or only appearance.
| Failure scenario | Evidence required | Recommended initial action | Potential remedy |
|---|---|---|---|
| Critical food-contact concern | Photos, lot code, documents, retained sample | Quarantine affected inventory | Reject, replace or issue full credit |
| Tray leakage during agreed test | Test record, timing, food load, photos | Stop use of affected lot | Replacement or proportional credit |
| Major forming defect | Carton count and defect sample | Inspect expanded sample | Sort, rework or replace affected quantity |
| Incorrect print or artwork | Approved proof and production photos | Hold branded stock | Reprint, replace or negotiated credit |
| Short carton quantity | Carton label, count sheet and photographs | Verify unopened cartons | Credit or replacement quantity |
| Transit carton damage | Delivery record, pallet images, carton labels | Separate damaged units | Assess carrier and packing responsibility |
| Minor cosmetic variation | Sample comparison and defect rate | Review against approved limit | Accept, partial credit or corrective action |
A practical rule is to require written notice within an agreed number of days after receipt, while allowing a longer period for hidden functional defects discovered during normal use. The clause should also explain who pays for independent inspection if a claim is substantiated. Clear rules support long-term supplier relationships because both parties know how problems will be assessed.
Fude Packaging: Manufacturing, Technology and Service for Canadian Buyers
Fude Packaging supports overseas B2B purchasers of paper food packaging with integrated development, manufacturing and export coordination. For Canadian distributors and venue programs, the value is not simply tray supply; it is the ability to connect sample approval, production controls, documentation and repeat-order consistency.
Technological capabilities
Technical support begins with the intended food application. Fude Packaging can review tray dimensions, board selection, grease-resistant or moisture-resistant material options, structural details, artwork placement and packing requirements before production. Digital proofs, white samples and printed pre-production samples help buyers validate layout, functionality and brand presentation. In-house testing capability supports practical checks for weight, dimensions, forming consistency and food-use performance.
For customized food-service programs, the team can review artwork and dielines, support Pantone colour matching and provide prototypes before release. This reduces the risk of discovering a capacity, stacking or print issue after containers have already arrived at a Canadian warehouse.
Manufacturing capabilities
With more than 20 years of packaging experience, a self-owned 30,000 m² production base and automated capacity of up to 120,000 units per day, Fude Packaging can support scheduled orders and scalable programs. The factory produces a broad range including cups, bowls, boxes, trays and multi-compartment meal packaging, allowing distributors to consolidate related paper-packaging categories.
Production control includes material selection, printing, die-cutting, forming, packing and batch identification. Full-batch traceability, incoming checks, production monitoring and final inspection provide a framework for consistent repeat orders. Buyers can also arrange independent pre-shipment inspection where their procurement policy requires it.
Service capabilities
For Canadian importers, Fude Packaging provides support from inquiry through export-ready packing. The team can clarify food type, serving temperature, destination requirements, branding needs, quantity, delivery deadline and shipping preference before recommending a solution. Documentation support may include food-contact, FSC, ISO 9001, LFGB, FDA-related or other applicable records based on the confirmed product and market requirement.
Buyers can explore related formats such as kraft paper fry cups when a more upright serving profile is needed. For project planning, review the available custom packaging services and learn more about the manufacturing background through Fude Packaging’s company information.
The comparison chart is a planning illustration. Buyers should evaluate each potential supplier using their own requirements for product compliance, lead time, minimum order quantity, test documentation, delivery terms and claim-handling procedures.
FAQ: Quality Standards for Canadian Concession Paper Trays
Which defects are critical for fast-service kraft concession trays?
Critical defects generally include foreign material, unacceptable odour, incorrect food-contact construction, missing required compliance information, sharp hazardous edges or open seams that make the tray unusable for the specified food. These defects should trigger immediate lot containment and investigation.
How many cartons should be inspected?
The correct number depends on batch size, risk level and agreement between buyer and supplier. At minimum, inspect cartons from several pallets and positions within the shipment. New products, new artwork, high-value event programs and first orders should receive broader sampling than established repeat orders.
Which real-food tests should be used?
Use the actual menu item or a realistic substitute with the same heat, grease, sauce and moisture characteristics. Canadian concession buyers commonly test fries, poutine, nachos, fried chicken, wings, mini donuts and sauced snack foods. Record portion weight, serving temperature and hold time.
How is the approved sample linked to production?
The sample should be labelled with a product code, artwork revision, date and written approval. It should be stored by both buyer and supplier together with the specification sheet. Final inspection samples are then compared against this retained reference before shipment.
What remedy should apply to a failed batch?
The remedy should be agreed in the purchase order. Depending on defect severity and timing, it may include replacement, credit, rework, sorting, return authorization or rejection. Critical food-contact and functional failures should receive the strongest remedy, while minor cosmetic issues may be resolved through an agreed allowance or credit.
Are kraft trays suitable for all hot foods?
No. Suitability depends on tray shape, paperboard weight, barrier construction, food temperature, oil content, sauce level and holding time. A tray intended for dry fries may not be suitable for gravy-heavy poutine. Always approve the exact format through a real-food test.
What should Canadian buyers request before confirming a bulk order?
Request a written specification, product drawing, approved sample process, food-contact documentation appropriate to the intended market, packing details, lot-traceability format, inspection standard, delivery terms and a defined non-conformance remedy. These records provide a repeatable basis for future reorders.
About the Author
Fude Packaging is a professional flexible packaging manufacturer serving global food brands, wholesalers, and distributors. Our team shares practical insights on custom packaging, printing technology, food-safe materials, and industry trends to help businesses build better packaging solutions.
Share
Product Category
Start Your Project With Fude Today
Related Post
-

Canada Packaging Purchase Contracts: Buyer Control Guide
A packaging purchase contract works best when it is more than a price sheet and purchase order. For Canadian food-service buyers, distributors, restaurant groups and private-label brands, it should be a documented cross-functional process that defines the approved product, measurable performance requirements, decision owners, acceptance thresholds, change controls and evidence to retain.In practical terms, the contract should connect procurement, packaging development, quality assurance, operations, finance, marketing and the supplier. Every party should know what must be approved before production, what happens if a paper bowl leaks or a printed cup colour shifts, who can authorize corrective action, and which documents are required before shipment to Canada.The most reliable approach is to validate the specification through digital proofs, white samples, printed pre-production samples and functional testing. A Canadian buyer importing packaging through Vancouver, Prince Rupert, Montréal or Halifax should also align the commercial agreement with shipping terms, lead times, import documentation and warehouse receiving procedures.Contract ControlWhat Must Be DefinedPrimary OwnerEvidence RequiredProduct scopeSKU, dimensions, capacity, material and coatingPackaging managerApproved specification sheetArtworkDieline, logo placement, Pantone reference and legal textMarketing and buyerSigned digital proofFood performanceHeat, grease, leak and lid-fit requirementsQuality assuranceSample test recordComplianceFood-contact and fibre-source documentationCompliance leadCertificates and declarationsProduction releaseApproved pre-production sample and production dateBuyerRelease email or signed formNonconformanceDefect classification, response timing and remedySupplier quality leadCAPA report and claim recordThis control table prevents a common procurement failure: a team assumes another person approved a detail, but no one can produce the evidence after a delivery problem occurs.Day-to-day purchasing requires a repeatable process. A contract should not be filed away after the first order; it should guide quotations, sampling, production releases, incoming inspection, claims and replenishment. For a Toronto quick-service restaurant chain, this may mean referencing one master agreement whenever stores reorder hot-food boxes. For a Vancouver distributor, it may mean using approved specifications to consolidate paper cups, bowls, trays and lunch boxes from one supplier.Begin with a master contract and create controlled order schedules for each SKU. The master document should establish payment terms, confidentiality, intellectual-property ownership, quality responsibilities, inspection rights, warranty terms, corrective-action expectations and governing commercial conditions. The order schedule should contain the current SKU data, quantities, ship dates, packaging configuration, delivery terms and approved revision number.Canadian buyers should avoid accepting vague descriptions such as “kraft bowl, premium quality” or “compostable cup.” The order must identify the exact material construction, capacity tolerance, coating type, colour standard, carton count, pallet arrangement and intended food application. If the package is designed for poutine, soup, oily noodles or hot beverages, testing conditions must reflect that use.Procurement StageRequired InputDecision GateOutput to Next StageDemand planningForecast, launch date, safety stockVolume confirmedRFQ packageSupplier quotationSpecification and destination portCommercial reviewQuoted price and lead timeTechnical reviewMaterial, drawings and food useFeasibility approvalSampling planSample approvalWhite, printed or functional sampleWritten sign-offProduction releaseMass productionApproved sample and quality planPre-shipment inspectionShipment authorizationReceiving reviewDelivery, count and defect findingsAcceptance or claimSupplier scorecard updateFor ongoing procurement, assign a revision code to every specification. A change in paperboard grade, coating, lid supplier, carton count or print colour should trigger review. This is especially important for multi-location businesses in Calgary, Edmonton, Ottawa and Montréal, where inconsistent packaging can disrupt store operations and brand presentation.Standardization reduces interpretation risk. The buyer’s technical specification should form an attachment to the packaging purchase contract, with each SKU controlled separately. Where multiple products use compatible lids or common carton sizes, link the related specifications so teams can identify system-level risks.At minimum, standardize product identity, material construction, dimensions, capacity, acceptable tolerances, performance tests, artwork, packing method, inspection method, certificates, delivery requirements and claim procedures. A supplier should not substitute materials or production methods without written approval from the authorized buyer representative.For food packaging imported into Canada, buyers should clarify applicable food-contact requirements and any provincial, municipal or customer sustainability expectations. The contract should require the supplier to provide relevant declarations and to notify the buyer before changing a material source, coating, adhesive, ink or manufacturing location.Specification CategoryExample StandardMeasurement MethodApproval EvidenceCapacity500 mL nominal capacityWater-fill testLaboratory recordTop diameter95 mm ± 1 mmCalibrated calliperInspection reportLeak resistanceNo leak after 30 minutesHot liquid hold testFunctional sample resultPrint colourApproved Pantone referenceVisual and instrument checkSigned printed proofCarton quantity500 units per master cartonCount verificationPacking list and inspectionOdour and cleanlinessNo foreign odour or visible contaminationVisual and sensory reviewFinal inspection recordMeasurements should be practical and repeatable. If a tolerance cannot be checked at the supplier, during third-party inspection or at the Canadian receiving warehouse, it is not a useful contractual requirement. The goal is not to create excessive paperwork; it is to make acceptance objective.Clear handoffs are essential when procurement, brand teams and operations work in different locations. A purchase contract should include a responsibility matrix showing who is responsible, accountable, consulted and informed at each stage. This prevents unclear responsibility after nonconformance, particularly when a problem emerges after packaging reaches restaurants or retail shelves.For example, marketing may own final artwork content, while packaging engineering owns dieline fit and procurement owns commercial release. Quality assurance should approve food-performance criteria, and operations should validate that cups fit dispensers, boxes stack correctly and cartons can be handled in the distribution centre. Finance may authorize payment only after shipping documents and inspection evidence are complete.Use a formal gate before tooling, before mass production and before shipment. Verbal approval from a sales representative or restaurant manager should not override the documented release process. If urgent changes are required, issue a controlled deviation authorization with the exact quantity, reason, risk assessment and expiry date.A strong contract converts quality expectations into measurable thresholds. Buyers should distinguish between critical, major and minor defects. Critical defects may include food-safety concerns, incorrect material, severe leakage, sharp edges or wrong legal information. Major defects may include widespread lid-fit failure, incorrect carton quantity or significant print variation. Minor defects may include small cosmetic variation that does not affect use or brand recognition.The contract should also define notification timing. A supplier may be required to report a suspected critical issue immediately, halt affected production, identify traceable batches and provide an initial containment report within 24 hours. A full corrective and preventive action report can follow after root-cause analysis.MeasureSuggested ThresholdEscalation TriggerRequired ResponseCritical defectsZero acceptedAny occurrenceStop shipment and notify buyerMajor defect rateAs agreed in inspection planAbove agreed acceptance levelSort, rework or replaceLeak test100% pass in sample testAny failure in validationReview material and forming processColour variationWithin approved visual standardVisible brand mismatchHold printed batch for reviewDelivery timingConfirmed shipping windowRisk to launch or stockoutRecovery plan within one business dayDocument completenessAll agreed documents before shipmentMissing certificate or inspection fileHold release until resolvedThe following illustrative trend chart shows why Canadian buyers increasingly formalize packaging controls as food-service demand and sustainability expectations rise. Figures are planning indicators, not market forecasts.var ctx=document.getElementById('lineChart').getContext('2d');new Chart(ctx,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Indexed Canadian food-service packaging demand',data:[100,106,112,118,125,133],borderColor:'rgb(44,123,182)',backgroundColor:'rgba(44,123,182,0.12)',fill:false,tension:0.3}]},options:{responsive:false,maintainAspectRatio:false}});Consider a Canadian meal-prep brand launching a 1,000 mL multi-compartment meal box for distribution in Greater Toronto Area stores. The buyer expects the box to hold hot rice, protein and sauce for up to 45 minutes without leakage or loss of structural integrity. The order will ship through the Port of Vancouver and then move by rail to Ontario.The project begins with a controlled brief: food type, serving temperature, microwave expectations, compartment layout, target capacity, stackability, branding, monthly forecast, destination requirements and launch date. Fude Packaging can support this stage through material recommendations, structural discussion, artwork and dieline checks, and sample options. Buyers can review food packaging product options while matching the format to real operating conditions.Next, the team approves a white sample to verify dimensions and lid fit, followed by a printed pre-production proof to confirm artwork and colour. The quality team performs functional testing with representative food. Procurement then issues the production release only after all requirements are recorded in the approval file.Project StepMeal Box RequirementOwnerAcceptance DecisionBrief creationThree compartments, 1,000 mL totalBuyer and operationsDemand and use case approvedMaterial selectionGrease-resistant food-contact constructionSupplier and quality teamDocuments reviewedWhite sampleFits store packing processOperations managerPhysical fit acceptedPrinted proofLogo and bilingual content placementMarketing leadArtwork signed offFunctional testNo leak or collapse with hot mealQuality assuranceTest record acceptedShipment releaseCorrect quantity and packing methodProcurement managerInspection evidence approvedThe example demonstrates why packaging contracts should combine commercial terms and technical execution. A lower unit price provides little value if the wrong structure causes food leakage, customer complaints or a delayed launch.Nonconformance management must be written before a problem occurs. The contract should define how the buyer reports defects, what information is needed, who assesses root cause, whether the supplier may inspect returned samples, how replacement stock is prioritized and how costs are allocated. Include batch and production-date traceability so the affected quantity can be isolated.A useful claim file includes photographs, receiving records, lot codes, sample quantities, defect counts, storage conditions, application details and customer impact. The supplier should provide containment, root cause, corrective action, preventive action and effectiveness verification. The buyer should document whether the corrective action worked on the next order.Fude Packaging operates with in-house laboratory testing, production monitoring and batch verification. Its manufacturing approach supports traceability from material selection through printing, forming, packing and shipment. For buyers who need additional assurance, third-party inspection or laboratory testing can be arranged before shipment.var ctx=document.getElementById('barChart').getContext('2d');new Chart(ctx,{type:'bar',data:{labels:['Quick-service restaurants','Coffee and beverage','Meal preparation','Retail food','Distributors','Institutional catering'],datasets:[{label:'Relative packaging demand index',data:[92,86,74,68,81,59],backgroundColor:['#2a9d8f','#457b9d','#f4a261','#e76f51','#6a4c93','#8ab17d']}]},options:{responsive:false,maintainAspectRatio:false}});This industry-demand comparison helps buyers prioritize which product families deserve the most rigorous approval records. High-volume cups, bowls and takeaway containers usually require tighter replenishment and inspection controls than occasional promotional packaging.Retained evidence makes repeat orders faster and safer. Keep one controlled digital folder per SKU and revision. Include the signed contract, approved drawings, digital proof, sample approvals, certificates, test results, inspection reports, packing specifications, shipping documents, batch records and corrective-action history.Review these records before every significant reorder, supplier change, material revision or market expansion. For example, a retailer adding Quebec distribution may need to reconfirm artwork, language content and operating requirements before releasing the next production batch.Document retention is also valuable during freight claims, warehouse disputes and customer audits. A complete approval trail can show whether the supplier met the approved requirement or whether the buyer changed a specification without issuing a controlled revision.var ctx=document.getElementById('areaChart').getContext('2d');new Chart(ctx,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Buyers requiring documented sample approval (%)',data:[48,55,63,70,77,83],borderColor:'rgb(42,157,143)',backgroundColor:'rgba(42,157,143,0.25)',fill:true,tension:0.3}]},options:{responsive:false,maintainAspectRatio:false}});The area chart illustrates the shift toward documented approval records. By 2026, buyers are expected to place greater emphasis on digital traceability, supplier-change notifications, sustainability declarations and performance validation.Fude Packaging supports overseas B2B customers with more than 20 years of packaging experience, a self-owned 30,000 m² production base and automated capacity of up to 120,000 units per day. Its manufacturing capabilities cover paper cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, trays and multi-compartment meal packaging.From a technological capability perspective, Fude Packaging combines material selection, printing, die-cutting, forming, inspection and laboratory testing within its controlled manufacturing process. Buyers can select digital proofs, white samples and printed pre-production proofs to confirm the product before mass production. This helps validate print accuracy, capacity, leak resistance, heat performance, grease resistance, structural strength and lid compatibility.From a manufacturing capability perspective, full-batch traceability and incoming-material inspection support consistent order control. Documentation can include BRC, FSC, ISO 9001, LFGB and FDA-related materials where applicable to the project. Buyers should still confirm the specific documents required for their product, destination and food-contact application.From a service capability perspective, Fude Packaging supports scheduled orders, export documentation, third-party inspection coordination and international shipping options. Standard production timing may be approximately 7–15 days depending on the product, customization and volume. Canadian customers can explore custom packaging services or contact the team for a project review through the Canadian buyer inquiry channel.var ctx=document.getElementById('comparisonChart').getContext('2d');new Chart(ctx,{type:'bar',data:{labels:['Customization','Batch traceability','Sample options','Product consolidation','Export support','Quality testing'],datasets:[{label:'Integrated manufacturer capability index',data:[92,90,95,88,86,91],backgroundColor:'rgb(106,76,147)'},{label:'Fragmented sourcing model index',data:[58,45,62,50,54,48],backgroundColor:'rgb(180,180,180)'}]},options:{responsive:false,maintainAspectRatio:false,scales:{x:{stacked:false},y:{beginAtZero:true,max:100}}}});This comparison highlights why many buyers prefer an integrated packaging manufacturer for multi-SKU programs. Consolidating cups, bowls, boxes and trays can simplify communication, reduce supplier-management workload and improve brand consistency.In 2026, packaging purchase contracts will increasingly include sustainability, traceability and digital-control clauses. Canadian buyers are likely to request clearer statements on fibre sourcing, coating composition, recyclability or compostability claims, and the documentation supporting those claims. Contracts should avoid broad environmental language unless the claim can be substantiated for the exact product and local waste-management context.Technology will also change procurement practice. Digital approval workflows, revision-controlled artwork portals, QR-linked batch records and automated supplier scorecards can reduce delays and improve accountability. Buyers should require written approval before a supplier changes a material, production line, critical subcontractor or design feature.Policy and customer expectations will continue to influence product design. Restaurant chains, retailers and institutional caterers may demand lower-plastic formats, responsibly sourced fibre, improved nesting efficiency and transport packaging that reduces damage. A purchase agreement should establish how such changes are tested, costed and approved before implementation.Local suppliers in Canada may offer short lead times for some standard products, while overseas manufacturers can provide stronger customization, category consolidation and scalable production for scheduled imports. The best sourcing model depends on order volume, storage capacity, launch urgency, landed-cost targets and risk tolerance. Learn more about the manufacturer’s background on the Fude Packaging company profile.It establishes the commercial and technical rules for a packaging supply relationship. It defines what will be supplied, how it will be approved, how quality will be measured, what records must be retained and how problems will be resolved.Procurement, quality assurance, operations, marketing, finance and the supplier should contribute. Inputs normally include the food application, expected temperature, dimensions, capacity, artwork, forecast, packing requirements, destination, compliance needs and delivery schedule.Place written gates before tooling or major setup expenditure, before mass production, before shipment and before any material or artwork change. For custom packaging, approve both the functional sample and the printed pre-production sample.It assigns owners, response times, defect categories, traceability requirements and corrective-action steps. The contract should identify who can stop production, approve concessions, authorize shipment and accept a corrective-action plan.Keep the contract, purchase order, approved specification, samples, artwork proof, certificates, test reports, inspection reports, packing lists, shipping documents, batch information, receiving results and nonconformance records. Review them before the next order to prevent repeat errors. -
Global Market School Meal Packaging Supply Strategy
A reliable school meal packaging supplier program for the Global market should use one controlled specification system across all schools, kitchens, distributors, and catering partners. Standardize the requirements that protect meal quality and operational consistency: approved materials, food-contact documentation, portion capacities, compartment geometry, print colors, allergen-label zones, case quantities, barcode formats, and replenishment rules. Then allow only documented local variations for menu format, student age group, regional regulations, language requirements, and school storage constraints.The most effective programs do not simply select a low-cost tray or lunch box. They connect packaging selection to the full food-service workflow: meal preparation, hot or cold holding, filling, sealing, labeling, transport, classroom handout, waste sorting, and reorder planning. A container that looks suitable in a sample room may fail during a 1,500-meal morning packing run if lids misalign, compartments overflow, or cartons cannot fit in the available storeroom.For multi-location buyers, the best operating model is a core-and-variant system. The core range may include approved paperboard grades, standard lid fits, fixed print layout, primary carton size, and central quality acceptance criteria. Controlled variants can include two-, three-, four-, or five-compartment meal boxes, special allergen label colors, regional recycling marks, and different case packs for urban or remote campuses. This approach gives procurement teams volume leverage without forcing every kitchen into an impractical one-size-fits-all format.School meal systems are expanding beyond traditional cafeteria service. They increasingly include central kitchens, outsourced caterers, meal-delivery programs, after-school nutrition initiatives, and emergency feeding plans. In global cities such as London, Dubai, Singapore, Sydney, Toronto, Los Angeles, and São Paulo, meal operators often manage different school calendars, supplier lead times, food-safety requirements, and municipal waste rules. Packaging specifications need enough discipline to remain comparable across sites, but enough flexibility to serve different menus and logistics conditions.A buyer should therefore approve packaging by use case rather than by appearance alone. Hot rice meals, chilled salads, sandwiches, fruit portions, pasta, soups, and culturally specific dishes each place different demands on grease resistance, moisture control, rigidity, closure security, and compartment volume. A documented school meal packaging standard makes sourcing, quality audits, staff training, and inventory forecasting materially easier.Specification areaWhat should be standardizedWhy it mattersPermitted local variationFood-contact materialApproved paperboard, coating, ink, and test documentationReduces compliance and migration riskDestination-market documentation setPortion capacityNominal volume and fill-line toleranceSupports nutrition and cost controlAge-group serving sizesAllergen labelingLabel position, contrast, font, and barcode logicImproves safe meal identificationLocal language and mandated symbolsContainer closureLid fit, locking points, and leak test criteriaProtects food in delivery and handlingSeal type for specific menu linesBrandingLogo placement, approved colors, print artwork processMaintains a consistent public imageSchool or district co-brandingCase packCarton dimensions, labeling, and pallet patternImproves warehouse and route efficiencySmaller cases for limited storageThis matrix should be owned jointly by procurement, nutrition, food safety, operations, and finance. It becomes the working document used for supplier quotations, samples, incoming inspection, and annual contract reviews.Portion control is one of the clearest ways packaging affects school meal economics. A compartment that is too large encourages over-serving; one that is too small creates spillover, poor presentation, or inconsistent nutrition portions. Specify usable capacity rather than nominal outside dimensions. For example, the relevant question is not whether a tray is “large”; it is whether the main compartment holds the approved serving of pasta or rice below the closure line without contacting the lid.Allergen management requires visible, repeatable information rather than informal staff knowledge. Packaging should provide a dedicated, unobstructed label panel. Avoid placing critical labels over folds, locking tabs, greasy surfaces, or curved areas where printers and scanners lose readability. Buyers should define a minimum contrast ratio, a label size, a barcode quiet zone, and a verification process before rollout. For schools serving pupils with severe allergies, use a clear visual hierarchy: student identification, allergen status, meal type, production date, and consumption deadline.Practical options include color-coded labels, printed allergen icons where locally accepted, tamper-evident stickers, and separate packaging streams for medically tailored meals. Color alone should never be the only control because labels can be misread, detached, or printed incorrectly. The safest system combines production records, staff checks, sealed container identification, and a documented exception process.Meal formatRecommended packaging featurePortion-control benefitAllergen-control considerationRice or grain bowlDeep main compartment with rigid baseConsistent scoop volumeKeep sauce label separate and legiblePasta mealWide compartment with secure lidLimits overfilling at the lineMark dairy and gluten information clearlySandwich mealShallow hinged box or trayProtects shape without excess spaceSeparate nut-free or special-diet unitsSalad mealCold-safe bowl with dressing cup areaSupports measured protein and vegetablesIdentify dairy, egg, sesame, and nutsSoup or curryLeak-resistant bowl and compatible lidDefines soup serving volumeUse durable labels resistant to condensationMixed bento mealMulti-compartment traySeparates prescribed food componentsPrevents accidental mixing during transportBefore approving a design, conduct a fill test with actual menu items at normal production speeds. Measure filling weight, headspace, lid contact, label adhesion, and post-transport appearance. Include both standard meals and high-risk meals such as oily pasta, wet curries, cut fruit, and sauce-heavy dishes.Hot and cold performance should be evaluated as a complete time-and-temperature journey. A hot meal may be packed at a central kitchen near Rotterdam, transported to several schools, held in insulated equipment, and distributed over a lunch period. A chilled meal may be prepared overnight, loaded at dawn, and exposed to warm loading areas before reaching schools. Packaging does not replace temperature control, but it must remain functional throughout the defined holding period.For hot applications, test resistance to softening, base deformation, grease penetration, lid warping, and steam accumulation. A fully sealed format can retain heat but may create condensation that weakens fried foods or makes labels unreadable. Venting, material selection, and serving window should be designed together. For cold meals, assess condensation, stacking compression, sauce leakage, and the ability of labels to remain attached after refrigeration.Specify a practical performance protocol: target food temperature at pack-out, expected maximum hold time, transport conditions, stacking height, and pass/fail criteria. A supplier should provide samples for functional testing, but school operators should also conduct a real route trial because local handling conditions cannot be replicated perfectly in a factory laboratory.var ctxMarketGrowth = document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctxMarketGrowth, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Indexed global demand for school meal packaging', data: [100, 108, 117, 126, 137, 149], borderColor: 'rgb(44, 117, 82)', backgroundColor: 'rgba(44, 117, 82, 0.12)', borderWidth: 3, fill: false, tension: 0.25 }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: false, title: { display: true, text: 'Demand index (2022 = 100)' } } } }});The demand index illustrates a realistic planning trend rather than a guarantee of market growth. The upward pattern reflects broader adoption of centralized meal service, stronger allergen labeling expectations, and the replacement of fragmented local purchasing with managed packaging programs.Compartment layout should follow the meal plan, not a generic tray template. Nutrition teams may need separation between protein, grains, vegetables, fruit, snack items, sauces, or dietary substitutions. A compartmentalized format can improve presentation, reduce cross-contact risk, and speed line assembly. However, additional compartments can increase unit cost, reduce usable capacity, and make stacking more difficult. The correct choice depends on menu complexity and operational value.Two-compartment formats work well for a main meal plus fruit or side dish. Three-compartment trays are common where starch, protein, and vegetables must remain distinct. Four- and five-compartment configurations provide better organization for bento-style meals, special diet sets, and diverse menus, particularly in Asia-Pacific school programs. Buyers can review custom four-compartment bento lunch boxes when evaluating structured meal formats with defined food separation.Each compartment must be evaluated for spoon access, filling accuracy, food movement, and cleanout. Very narrow sections may look efficient on a drawing but slow the packing line and frustrate younger children. Rounded internal corners are generally easier to fill and clean visually than sharp angles. If sauces are included, test whether liquid moves between compartments when the tray is tilted or stacked.Layout typeBest use caseOperational advantageWatchpointSingle compartmentPasta, rice bowls, saladsFastest filling processLimited food separationTwo compartmentsMain dish plus sideLow-complexity balanced mealSide section may be too small for fruitThree compartmentsProtein, starch, vegetablesSupports standard nutrition formatsRequires consistent scoop toolsFour compartmentsBento and varied lunch setsClear meal organizationMore complex filling sequenceFive compartmentsPremium catered mealsMaximum separation flexibilityHigher material and packing costTray plus sauce cupCold salads and sauced dishesKeeps textures separateExtra component must be controlledA multi-compartment design is particularly valuable where a central kitchen serves several dietary plans from the same line. For larger catering programs, buyers may compare bulk five-compartment catering trays to determine whether additional food separation offsets added handling time.Packing-line speed depends on more than labor. Packaging geometry, nesting consistency, opening force, lid orientation, label placement, and carton access all affect output. A box that requires two hands to open or a lid that must be aligned precisely may add seconds to every meal. Across a 3,000-meal production run, those seconds become a major staffing cost.Choose containers that denest cleanly, remain stable on conveyors, and have obvious front-to-back orientation. Standardize the location of labels and seals so staff do not need to rotate each meal repeatedly. If using hinged boxes, test the fold memory and closure strength after repeated opening. If using separate lids, confirm that the lid stack does not stick together under humid kitchen conditions.Line trials should measure not only units per minute but also rework. Track rejected containers, relidding, label replacement, food spills, and pauses for replenishment. The cheapest unit may become the most expensive served meal if it causes line congestion or waste.var ctxIndustryDemand = document.getElementById('industryDemandChart').getContext('2d');new Chart(ctxIndustryDemand, { type: 'bar', data: { labels: ['Primary schools', 'Secondary schools', 'Central kitchens', 'After-school programs', 'Emergency meal services', 'University feeders'], datasets: [{ label: 'Estimated packaging demand score', data: [84, 78, 96, 61, 54, 47], backgroundColor: ['#3c8d67', '#4aa47b', '#6db98f', '#8ccaa5', '#b3ddc2', '#d0ead8'] }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Demand score out of 100' } } } }});Central kitchens typically create the greatest demand for standardized packaging because they supply multiple sites, work to fixed dispatch times, and need reliable case-level replenishment. Primary schools also generate high demand because younger pupils often require more controlled portions and simple, secure formats.Case pack selection is an inventory and labor decision. Large cartons can lower handling cost and improve container utilization for sea freight, but they may be difficult for a small school storeroom to receive, move, or protect from moisture. Small case packs offer flexibility but can create more picking work and higher outer-carton use. The right answer often combines a master carton for central warehouses with smaller internally packed sleeves for school-level distribution.For Global market procurement, calculate cube utilization at every stage: factory pallet, container, import warehouse, distributor vehicle, central kitchen, and school storage room. A carton that is efficient in a 40-foot container may be inefficient in a narrow school storeroom. Buyers importing through ports such as Shanghai, Qingdao, Singapore, Jebel Ali, Rotterdam, Hamburg, Los Angeles, or Melbourne should also allow for local drayage, customs clearance, and seasonal warehouse capacity.Storage factorRecommended controlOperational outcomeAudit frequencyHumidityKeep cartons dry and off the floorProtects paperboard rigidityWeeklyFirst-expiry rotationApply batch and receipt-date labelsImproves traceabilityEvery deliveryCarton stackingFollow approved maximum stack heightPrevents crushed containersDailySchool stock levelSet minimum and maximum quantitiesReduces emergency ordersWeeklyDamage isolationQuarantine wet or crushed cartonsStops defective useAs neededBarcode scanningScan receipt and issue movementsImproves inventory accuracyEvery movementPackaging suppliers should provide outer-carton specifications, pallet patterns, gross weight, net weight, and recommended storage conditions before a purchase order is released. These details are essential for international buyers planning consolidated loads and warehouse labor.A school meal supply calendar should start with the academic year, not the factory production date. Map school opening days, holidays, menu changes, examinations, summer feeding programs, weather disruptions, and procurement approval cycles. Then work backward to set forecast locks, production windows, shipping lead times, customs allowances, warehouse receipt dates, and local delivery schedules.For ocean freight, buyers should protect the calendar with a realistic buffer. A shipment from eastern China through Qingdao or Shanghai to Rotterdam, Felixstowe, Dubai, Sydney, or Los Angeles is influenced by vessel schedules, port congestion, customs inspection, and inland transport. Fast-moving sites should not rely on one late container as their sole source of supply. A staged inventory model with central safety stock and local operating stock is usually more resilient.Use a monthly forecast for the next six to twelve months, a firm order window for the next two to three months, and a weekly consumption review during peak periods. Create escalation rules for enrollment increases, menu launches, extreme weather, labor shortages, and promotion-driven meal demand.var ctxTrendShift = document.getElementById('trendShiftChart').getContext('2d');new Chart(ctxTrendShift, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Share of programs using fiber-based meal packaging (%)', data: [38, 44, 51, 58, 65, 71], borderColor: 'rgb(40, 119, 155)', backgroundColor: 'rgba(40, 119, 155, 0.24)', fill: true, tension: 0.3, borderWidth: 3 }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Estimated share (%)' } } } }});The trend shift reflects growing interest in fiber-based formats, improved water- and grease-resistant coatings, stronger recyclability communication, and procurement policies that increasingly assess material choices alongside price and performance.Cost per served meal is a more useful buying metric than unit price. It includes the container, lid, label, outer carton, freight, customs, warehouse handling, line labor, spoilage, breakage, and rework. A procurement team should calculate total landed cost by serving format and compare it with operational results. This reveals whether a slightly higher-priced box reduces leakage, speeds packing, or lowers food waste enough to create a better overall outcome.Use the same calculation across all sites. Separate unavoidable local costs, such as import duty or last-mile delivery, from supplier-controlled costs such as carton efficiency, defect rate, print accuracy, and production lead time. This creates fair supplier comparisons and identifies where standardization can reduce total cost.Cost elementExample measureTypical ownerImprovement leverContainer and lidCost per approved setProcurementConsolidated purchasing volumeFreight and customsLanded cost per caseLogisticsContainer utilization and routingLine laborSeconds per packed mealKitchen operationsEasy denesting and closureFood lossSpill or leakage rateFood-service managerBetter fit and compartment designDefectsRejected units per 10,000Quality teamIncoming and batch inspectionInventory carrying costDays of stock heldWarehouse teamForecast and reorder disciplineAs a rule, buyers should use a 90-day pilot to establish a baseline. Measure units packed, time per meal, defects, complaints, food leakage, waste, on-time delivery, and stockouts. Then compare the pilot data against the existing package rather than relying only on supplier samples or catalog descriptions.Fude Packaging supports overseas B2B buyers seeking a scalable school meal packaging supplier for the Global market. Our approach is designed for procurement teams that need product consistency across multiple food formats without losing the flexibility required by regional menus, school storage limits, and local compliance needs.Our in-house laboratory and quality process support practical evaluation of paper-based food packaging performance, including strength, leak resistance, grease resistance, heat suitability, lid compatibility, print accuracy, dimensions, and batch consistency. Buyers can request white samples, printed samples, or functional prototypes to review packaging before full production. We also support artwork and dieline checks, Pantone color matching, material recommendations, and custom structural development for school meal trays, lunch boxes, bowls, and food containers.With more than 20 years of packaging experience, a self-owned 30,000 m² factory in Shandong, automated production lines, and capacity of up to 120,000 units per day, Fude Packaging can support planned volume programs and replenishment schedules. Our product range includes paper cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, food trays, and multi-compartment meal boxes. Buyers can explore the wider food container range when consolidating school meal packaging categories under one manufacturing partner.Fude Packaging works with importers, distributors, food-service operators, restaurant groups, and food brands across more than 50 countries. Our international service includes project clarification, sampling, production scheduling, export packing, inspection support, and shipping coordination by sea, air, full container, less-than-container, or express sample service. Standard orders may be completed in approximately 7–15 days, subject to product design and volume. We can assist with documents such as commercial invoices, packing lists, certificates, and inspection records for shipments routed through global trade hubs.var ctxSupplierComparison = document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctxSupplierComparison, { type: 'bar', data: { labels: ['Quality consistency', 'Customization', 'Export documentation', 'Multi-category supply', 'Pilot support', 'Replenishment planning'], datasets: [ { label: 'Managed manufacturing partner', data: [92, 90, 88, 94, 86, 89], backgroundColor: 'rgb(75, 120, 190)' }, { label: 'Fragmented spot purchasing', data: [61, 48, 54, 43, 39, 51], backgroundColor: 'rgb(180, 190, 205)' } ] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Program capability score' } } } }});This comparison chart is an operational illustration. It shows why school districts, caterers, and distributors often benefit from evaluating suppliers on program capability, not just quotation price. The ability to coordinate samples, specifications, quality checks, export documents, and replenishment can reduce hidden purchasing risk.By 2026, school meal packaging decisions will increasingly be shaped by three linked trends. First, digital traceability will expand through batch codes, scan-ready labels, and inventory systems that connect central warehouses to individual schools. Second, policy requirements will place greater emphasis on food-contact compliance, waste reduction, material transparency, and credible environmental claims. Third, sustainable packaging development will focus less on broad marketing language and more on verified material choices, local end-of-life infrastructure, coating performance, and total resource use.Buyers should avoid assuming that one sustainability claim applies in every country. Compostability, recycling access, labeling rules, and food-contact requirements differ by market. The right approach is to define the destination country, collection infrastructure, performance need, and documentation required before selecting materials. A qualified supplier can then recommend suitable paperboard, barrier treatment, certification pathway, and print design.Create a master specification covering material, food-contact requirements, dimensions, fill capacity, compartment layout, lid fit, branding, label position, case pack, carton marks, quality checks, and reorder rules. Use a controlled change process so no site changes a package without approval from procurement, operations, and food safety.Allow variations only where they serve a clear operational or regulatory need. Common examples include local-language labels, age-based portion sizes, regional recycling marks, different menu layouts, special-diet packaging, and smaller case packs for schools with limited storage. Record each approved variation in a site specification register.Test samples using actual foods, temperatures, fill weights, hold times, transport routes, stacking heights, and labeling equipment. Conduct a limited production pilot, inspect defects, collect staff feedback, and compare packing speed and waste against the existing package. Approve mass production only after documented pass criteria are met.Hold buffer stock centrally for supply resilience and maintain smaller operating stock at each school. Set reorder points based on average meal volume, peak-demand periods, shipping lead time, local delivery frequency, and the risk of disruption. Review consumption weekly during school terms and more often during launches or seasonal changes.Track on-time-in-full delivery, stockout frequency, inventory accuracy, defect rate, leakage complaints, line speed, seconds per packed meal, label scan success, food waste, packaging waste, and landed cost per served meal. Review KPI trends by school, central kitchen, meal format, and supplier batch to identify improvement opportunities early. -

Canada Guide to Kraft Paper Bowl Factory Visits
For buyers in Canada, visiting a kraft paper bowl factory is one of the fastest ways to verify product quality, food-safety control, production reliability, and export readiness before placing wholesale orders. A professional paper bowl plant is usually organized into clear production zones for raw material storage, printing, coating, die-cutting, bowl forming, inspection, packing, and warehouse dispatch. When you understand how these areas work together, it becomes much easier to evaluate whether a supplier can meet the expectations of restaurants, distributors, food delivery brands, and importers in Toronto, Vancouver, Montreal, Calgary, Edmonton, Ottawa, Winnipeg, and other Canadian markets.Canada’s food-service packaging market increasingly demands grease resistance, leak prevention, stackability, custom branding, and compliance with food-contact rules. For kraft paper bowls used in salads, noodles, soups, poke, desserts, and takeaway meals, the factory setup matters as much as the bowl design itself. A well-managed site should demonstrate traceable raw materials, stable lining adhesion, dimensional consistency, in-process testing, controlled packaging lines, and suitable warehousing conditions for international shipping through trade corridors linked to the Port of Vancouver, Port of Montreal, Port of Halifax, and inland logistics networks serving Ontario, British Columbia, Alberta, and Quebec.In this guide, you will find a practical explanation of how a kraft paper bowl manufacturing plant is organized, what equipment and testing systems matter most, what questions Canadian buyers should ask during a factory tour, and how to compare suppliers for long-term purchasing.A kraft paper bowl factory should have clearly separated zones for paper roll storage, coating or lining, printing, die-cutting, bowl forming, inspection, packaging, and finished goods warehousing. For Canada-bound orders, buyers should verify food-grade materials, coating performance, leak and grease tests, printing safety, production capacity, warehouse controls, and export packing suitability. A reliable manufacturer does not only show machines; it shows process discipline, quality records, traceability, sanitation, and practical answers about lead time, customization, certifications, and shipment support.In simple terms, if you are visiting a supplier for kraft bowls, soup bowls, salad bowls, or takeaway food containers, look for five signals:Clean and organized material flow from incoming paper to final dispatch Stable production equipment with visible in-process quality checks Documented food-contact and performance testing Packaging and warehousing suited for long-distance export to Canada Transparent communication on customization, MOQ, lead times, and after-sales support For Canadian importers and distributors, this matters because packaging must travel well, remain consistent across repeat orders, and support local branding requirements. Bowls that look fine in a sample but fail under hot soup, oily meals, or frozen storage can create costly problems across restaurant chains and takeaway operations.The layout of a kraft paper bowl plant reveals how seriously a manufacturer manages efficiency and contamination risk. In a well-run facility, people, raw materials, semi-finished goods, and finished cartons move in a logical one-way direction. This reduces errors, improves hygiene, and makes output more predictable.Typical production zones include inbound material receiving, raw paper storage, pre-press and printing, coating or lamination, die-cutting, sidewall and bottom blank preparation, bowl forming, rim curling, visual and functional inspection, packaging, palletizing, and warehouse dispatch. Some factories also separate sample development, mould storage, maintenance workshops, and quality laboratories into dedicated rooms.For Canadian buyers, the ideal layout is not necessarily the largest factory, but one with disciplined zoning. If forklifts, scrap, inks, food-contact paper, and packed cartons are mixed in the same aisle, it may indicate weaker process control. If the plant uses marked floor lanes, labeled stations, batch identification cards, and documented quality checkpoints, that is usually a stronger sign.Production ZoneMain FunctionWhat Buyers Should CheckRisk If WeakIncoming Material AreaReceives paper, PE or PLA film, inks, lids, cartonsBatch labeling, inspection records, moisture protectionWrong material use or damaged stockPaper Roll StorageStores kraft and white paper reelsHumidity control, FIFO handling, clean floor conditionsWarping, print defects, reduced forming qualityPrinting AreaApplies brand graphics and product informationColour consistency, food-safe ink controls, plate managementOff-colour branding or contamination concernsCoating/Lining AreaAdds PE or PLA barrier for leak and grease resistanceAdhesion stability, thickness control, cleanlinessLeaks, delamination, poor heat resistanceDie-Cutting SectionCuts blanks for bowl walls and bottomsDimensional precision, scrap handling, blade conditionInconsistent bowl fit and weak sealingForming AreaShapes bowls and seals componentsMachine speed, seam quality, operator checksDeformed rims or seam leaksPacking AreaCounts, bags, boxes, labels productsCleanliness, barcode and carton accuracyWrong pack quantities or transit damageThe table above shows how each factory zone contributes directly to bowl performance. For Canada, where products may travel by sea and then inland truck or rail, process consistency is especially important. Long transit times test the durability of both the bowl and the export carton.Many buyers from Canada also look at layout efficiency because it affects lead time. If a plant has a fragmented workflow, sample approval may be easy but mass production may be slow or inconsistent. Factories serving chain restaurants or distribution centres in Mississauga, Surrey, Laval, or Calgary often need disciplined scheduling and fast reordering capabilities.var ctx1 = document.getElementById('lineChartGrowth').getContext('2d');var chart1 = new Chart(ctx1, {type: 'line',data: {labels: ['2021', '2022', '2023', '2024', '2025', '2026'],datasets: [{label: 'Estimated Canada Demand Index for Paper Bowls',data: [78, 84, 91, 99, 108, 118],borderColor: 'rgb(75, 192, 192)',backgroundColor: 'rgba(75, 192, 192, 0.15)',fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The growth trend above reflects why factory visits are becoming more important. As paper bowl demand grows across Canadian food delivery, casual dining, and retail prepared meals, buyers need dependable manufacturing partners rather than opportunistic traders.Raw material handling is one of the most overlooked parts of paper bowl manufacturing, yet it strongly influences final product quality. Kraft paper bowls begin with paperboard, and paper reacts to moisture, temperature, pressure, and storage duration. If paper rolls are badly stored, even the best machines later in the process may struggle to produce stable bowls.A strong paper bowl factory stores parent rolls or sheets in a dry, clean, ventilated area with controlled humidity. Rolls should be elevated off the ground, protected from direct wall contact, and identified by lot number, GSM, supplier, coating type, and receiving date. PE-lined paper, PLA-coated paper, and uncoated kraft stock should be separated to avoid mixing errors.Canadian buyers should also ask about winter and summer material behaviour. Bowls shipped to Canada may encounter cold weather in Montreal, Ottawa, Quebec City, Winnipeg, Saskatoon, or Regina, and warmer warehousing in indoor food-service storage. Material stability matters across these shifts.MaterialTypical UseStorage RequirementInspection FocusKraft paper rollOuter body for natural-look bowlsDry area, humidity monitoredSurface strength, colour consistencyWhite paperboardPremium printed bowlsDust-free stacking and wrap protectionBrightness, print suitabilityPE-coated stockHot soups and general takeawayTemperature-stable covered storageCoating uniformity, odour, adhesionPLA-coated stockCompostable application linesControlled temperature and batch separationHeat sensitivity, barrier integrityFood-grade inkBrand printingSealed containers, controlled handlingCertification, shelf lifeCorrugated cartonsExport packagingDry storage away from floor moistureCompression strength, print marksThe table explains how different materials require different controls. A supplier that stores all inputs the same way may not be managing risk properly. During a tour, ask whether they use FIFO or FEFO systems, whether incoming paper is tested before release, and whether moisture records are documented.Material handling equipment also matters. Larger plants often use roll clamps, hydraulic lifters, pallet jacks, and barcode systems to reduce damage and misidentification. Manual handling may be acceptable in smaller custom runs, but it must still be controlled. Torn wrappers, dented roll edges, and unlabeled pallets are all warning signs.Another useful point for Canadian importers is traceability. If a restaurant group in Toronto reports an issue with one shipment, can the factory trace the paper lot, production date, machine line, and operator? Good factories can. Weak traceability can turn a small complaint into a large claim.For buyers sourcing not only bowls but also related packaging, it is useful to review the supplier’s full product family. For example, some importers combine bowls with Custom Paper Food Container products to build one coordinated takeaway range for urban markets such as Vancouver and Toronto.The coating or lining area is critical because it determines whether a paper bowl will resist grease, liquid, and heat. Kraft paper alone is not enough for most food-service uses. Bowls for ramen, pho, soup, curry, poutine, salad with dressing, frozen desserts, or oily rice meals need a barrier layer that performs under real use conditions.Most factories use PE coating for broad food-service applications because it offers good liquid resistance and heat performance. Some buyers prefer PLA-lined structures where compostability goals or local brand positioning require a plant-based lining. The right choice depends on use case, policy direction, composting infrastructure, and price expectations.The coating process may occur in-house or the factory may source pre-coated rolls from approved mills. During a visit, ask which model the supplier uses. In-house coating gives greater control but also requires strong process discipline. Sourced coated paper may be fine if supplier qualification is solid and testing is rigorous.Key process factors include coating thickness, adhesion, surface uniformity, heat sealing behavior, and compatibility with forming speed. If coating is too thin, bowls may leak. If too thick, forming and curling may become unstable or cost may increase unnecessarily. For Canadian food-service use, barrier consistency matters particularly for hot soups, takeaway gravies, and chilled salads with acidic dressings.Process ElementWhy It MattersQuestions to AskCommon DefectCoating TypeAffects leak resistance and end-of-life claimPE or PLA? Single or double side?Wrong fit for applicationCoating WeightControls barrier level and sealingHow is thickness measured?Pinholes or weak sealAdhesion StrengthPrevents delamination during useDo you test peel strength?Layer separationHeat Sealing WindowSupports bowl side seam and bottom sealWhat machine settings are validated?Inconsistent seam bondingSurface CleanlinessPrevents sealing and print issuesHow is dust controlled?Leaks and visual marksFood Contact ComplianceRequired for export marketsWhat migration and safety documents are available?Import risk or customer rejectionThis table helps buyers connect technical details to commercial outcomes. If a supplier cannot explain coating control in simple terms, that can be a concern. Good factories usually show samples of different structures for soup bowls, salad bowls, freezer-safe bowls, and microwave-use variants.When assessing equipment, look for stable unwind systems, edge control, temperature monitoring, and regular calibration. In the forming area, inspect side seam integrity and bottom crimping. Leak tests should be routine, not performed only for visitors.In Canada, restaurants and chains often want bowls that can handle mixed-use conditions: hot contents, delivery transit, and short hold times. This means the lining must support not just one test point but realistic daily use. Buyers serving meal-prep companies, quick-service brands, and delivery kitchens in cities like Brampton, Burnaby, Richmond, and Longueuil should align the bowl structure with actual menu temperature and hold-time conditions.var ctx2 = document.getElementById('areaChartShift').getContext('2d');var chart2 = new Chart(ctx2, {type: 'line',data: {labels: ['2021', '2022', '2023', '2024', '2025', '2026'],datasets: [{label: 'PE-Lined Share',data: [72, 69, 66, 63, 59, 55],borderColor: 'rgb(54, 162, 235)',backgroundColor: 'rgba(54, 162, 235, 0.18)',fill: true,tension: 0.3},{label: 'PLA/Alternative Lining Share',data: [18, 21, 24, 28, 33, 38],borderColor: 'rgb(255, 159, 64)',backgroundColor: 'rgba(255, 159, 64, 0.18)',fill: true,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The area chart illustrates a realistic market shift toward broader adoption of alternative linings through 2026. PE remains important, but policy pressure and sustainability branding are pushing more buyers to evaluate compostable or lower-impact structures.A serious kraft paper bowl manufacturer should have more than a visual inspection desk. It should have a quality control laboratory or at least a structured testing room with documented procedures. This is essential for Canada because importers, wholesalers, and branded food-service operators need consistency across repeat shipments.Typical tests include basis weight checks, thickness measurement, burst strength, stiffness, coating adhesion, seam strength, leak testing, heat resistance, grease resistance, odour checks, print rub resistance, drop performance for packed cartons, and dimensional accuracy. Advanced factories may also conduct migration-related verification through internal protocols and third-party coordination.When touring a factory, do not ask only whether they have a lab. Ask what they test at incoming, in-process, and pre-shipment stages. Also ask for sample retention practice. Reliable factories often keep retained samples by batch for complaint investigation.Test ItemPurposeStageImportance for CanadaLeak TestChecks liquid retention over timeIn-process and finalCritical for soup and sauce bowlsGrease ResistanceVerifies oil barrier performanceMaterial and finalImportant for poutine, noodles, fried foodsSeam StrengthConfirms sidewall integrityIn-processPrevents failure during deliveryRim Curl QualityChecks lid fit and user comfortIn-processImportant for stackability and sealingCompression TestEvaluates carton shipping strengthPackaging stageUseful for ocean and inland transitPrint Adhesion/RubConfirms branding durabilityFinalProtects retail presentation and label clarityThe table above explains why laboratory capability is closely tied to customer satisfaction. A bowl factory serving export markets should be able to show records, not only verbal assurances. If a factory says “we check everything,” ask to see the form, the frequency, and the acceptance range.For Canada, quality expectations may vary by sector. Independent restaurants may focus on cost and leak resistance, while chain operators often require stricter print tolerances, audit readiness, and traceability. Retail meal brands may additionally care about freezer performance, window presentation, and shelf consistency.Demand is also diversified across packaging categories. Buyers who source bowls frequently also review matching lines of Custom Paper Bowl products and beverage companions such as Custom Paper Cup products to create a unified branded takeaway system.var ctx3 = document.getElementById('barChartDemand').getContext('2d');var chart3 = new Chart(ctx3, {type: 'bar',data: {labels: ['Restaurants', 'Delivery Kitchens', 'Cafes', 'Caterers', 'Retail Meal Prep', 'Wholesalers'],datasets: [{label: 'Estimated Canada Demand Index by Segment',data: [92, 106, 74, 68, 88, 97],backgroundColor: ['rgb(255, 99, 132)','rgb(54, 162, 235)','rgb(255, 206, 86)','rgb(75, 192, 192)','rgb(153, 102, 255)','rgb(255, 159, 64)']}]},options: {responsive: true,maintainAspectRatio: false}});The segment demand chart shows why testing priorities differ by customer type. Delivery kitchens may put more stress on leak prevention and lid fit, while cafes may emphasize print appearance and lightweight stackability.The final packaging line is where a large amount of value can either be protected or lost. Even well-made bowls can arrive damaged if counting, bagging, carton loading, or palletization is poorly managed. For Canada-bound shipments, export packaging must withstand marine humidity, port handling, container stacking, and inland transport.At a minimum, a paper bowl factory should have counting controls, sealed inner bags or sleeves where needed, clear carton labels, pallet stretch wrapping, and a clean finished goods warehouse. The warehouse should be dry, organized by batch, and arranged for FIFO shipment. Climate control is a plus, especially for printed and coated products.Factories with strong export experience often design cartons around container utilization while balancing compression performance. If cartons are overfilled, bowl rims may deform. If underfilled, products can shift during transport. Good packaging engineering saves money and reduces claims.Warehouse/Packing ElementBest PracticeWhy It MattersBuyer CheckpointInner PackingFood-contact protective sleeves or bagsPrevents dust and handling contaminationIs packing sealed and counted accurately?Carton LabelingSKU, quantity, batch, destination marksSupports inventory and claims handlingCan labels match your PO system?PalletizationStable stack pattern and stretch wrapProtects goods in transitDo pallets stay secure under movement?Humidity ControlDry warehouse with ventilationReduces carton weakening and paper distortionAre records or monitoring devices visible?Container LoadingBalanced, documented loading planPrevents collapse and shipment lossDo they have export loading photos?Finished Goods TraceabilityBatch-coded stock separationImproves recall and complaint responseCan one pallet be traced back to one run?This table shows why warehouse management deserves as much attention as production equipment. In Canadian distribution, where goods may move from port to 3PL to regional distribution to store or restaurant, every packaging layer matters.Warehouse location relative to ports and trade lanes also affects buyer decisions. Suppliers experienced in exports understand container timing, documentation accuracy, and lead time planning around shipping peaks. Buyers importing to Vancouver may prioritize west-coast arrival planning, while Montreal and Halifax importers may focus on east-coast routing and seasonal weather considerations.A good supplier should also be able to support mixed orders. For example, many distributors want bowls, cups, lids, and food containers in coordinated shipments. Suppliers offering Custom and Wholesale food Paper packaging can help simplify sourcing, artwork management, and production scheduling.Environmental and safety compliance has become a central purchasing criterion in Canada, especially for brands targeting sustainability-conscious consumers and institutional buyers. During a factory visit, do not limit your review to product claims. Assess how the site handles waste, worker safety, emissions, sanitation, and responsible sourcing.For paper bowl manufacturing, major compliance topics include food-contact material control, waste segregation, scrap recovery, ink and chemical handling, ventilation, machine guarding, worker protective equipment, emergency exits, fire systems, and documentation of certifications. For sustainability-focused procurement, FSC-certified sourcing, compostable material options, and reduced-waste production practices are increasingly relevant.Canada’s market is also evolving under growing public scrutiny around single-use packaging. That means suppliers should be able to discuss not just today’s options, but also their 2026 readiness: lightweighting, alternative linings, better recyclability pathways, compostability claims with evidence, and clearer environmental communication.Compliance AreaFactory IndicatorWhy It Matters in CanadaFuture 2026 TrendFood Safety ManagementDocumented SOPs and batch recordsSupports importer confidenceMore audit-driven procurementSustainable Paper SourcingFSC or equivalent chain documentationImportant for eco-positioningStronger retailer scrutinyCoating OptionsPE and compostable alternatives availableSupports policy adaptationGrowth in low-impact structuresWaste ManagementScrap sorting and reduction programsAligns with ESG expectationsMore lifecycle-focused buyingWorker SafetyPPE, machine guards, training logsSignals responsible operationsSupplier audits becoming stricterWarehouse HygieneClean, controlled finished goods areaProtects product integrityDigital monitoring expansionThe explanation from the table is straightforward: Canadian buyers increasingly value factories that combine compliance with practical product performance. Certifications are useful, but they should be supported by visible operating discipline.Looking ahead to 2026, three trends are especially important:More demand for packaging with lower environmental impact and transparent sourcing claims Stronger buyer focus on auditability, digital traceability, and supply chain resilience Greater need for packaging engineered for delivery, microwave convenience, and brand differentiation These trends are likely to shape purchasing decisions across restaurant chains, meal subscription services, universities, hospitals, and specialty retailers throughout Canada.A factory tour is most useful when buyers ask targeted, practical questions. Many visits fail because the discussion stays too general. Instead of only asking, “Can you make this bowl?” ask how the factory controls the process from paper intake to shipment.Here are essential questions Canadian buyers should ask:What paper grades and coating structures do you recommend for hot soup, salad, frozen dessert, and oily meals? Are coating and printing completed in-house or outsourced? How do you control humidity and material aging in storage? What are your standard leak test conditions and acceptance limits? How often do you check seam strength, dimensions, and rim quality during production? Can you provide batch traceability for each shipment? What certifications and food-contact compliance documents are available? How do you pack export orders for long-distance ocean transport to Canada? What is your usual lead time for custom printing and repeat orders? How do you handle complaints, replacements, or technical follow-up after delivery? It is also useful to ask for a live demonstration. Request that the factory produce or show recent samples close to your specification and explain what process settings were used. Good suppliers are usually comfortable discussing real production details.For buyers comparing multiple factories, a scorecard helps. Rate each supplier across material control, machine capability, testing discipline, packaging quality, communication speed, documentation, and service flexibility. This reduces the chance of choosing only on price.var ctx4 = document.getElementById('comparisonChartSuppliers').getContext('2d');var chart4 = new Chart(ctx4, {type: 'bar',data: {labels: ['Traceability', 'Leak Control', 'Customization', 'Export Packing', 'Lead Time', 'Documentation'],datasets: [{label: 'Supplier A',data: [90, 93, 88, 92, 80, 89],backgroundColor: 'rgba(153, 102, 255, 0.8)'},{label: 'Supplier B',data: [76, 82, 79, 75, 86, 72],backgroundColor: 'rgba(75, 192, 192, 0.8)'},{label: 'Supplier C',data: [84, 88, 91, 87, 78, 85],backgroundColor: 'rgba(255, 159, 64, 0.8)'}]},options: {responsive: true,maintainAspectRatio: false}});The comparison chart demonstrates a practical way to evaluate suppliers beyond unit cost. Canadian importers often find that the most economical long-term supplier is the one with fewer defects, stronger documentation, and smoother reorder execution.Case studies from the market show this clearly. A food distributor serving restaurants in Greater Toronto may prefer a supplier with stronger carton performance to reduce warehouse breakage. A poke bowl brand in Vancouver may prioritize premium print consistency and leak-tested lids. A soup and noodle chain in Montreal may care most about hot-fill resistance and seam integrity during winter delivery conditions. The best supplier depends on the end application, not just the sample price.Shandong Fude Packaging Co., Ltd. supports buyers seeking a dependable manufacturing partner for disposable food-grade paper packaging. For Canadian customers, our value is built around three practical strengths: technological capability, manufacturing capability, and service capability.Technological capabilities: our production system integrates flexographic printing, die-cutting, bowl and cup forming, and quality testing processes that support stable branding, dimensional consistency, and functional food packaging performance. We work with kraft and white paper structures as well as food-grade lining options suited to takeaway, soup, salad, dessert, and beverage applications. This allows us to help customers evaluate the right structure for market needs rather than offering one generic solution.Manufacturing capabilities: operating from a modern 30,000 square meter facility in Shandong, we maintain automated production capacity and organized workflow for food-service packaging export. Our experience includes serving customers across North America, Europe, Southeast Asia, the Middle East, and other regions. We support custom manufacturing for bowls, cups, and containers with attention to leak resistance, grease performance, stackability, and print presentation. Buyers looking to extend product lines can also explore related ranges such as Custom Paper Food Container products, Custom Paper Bowl products, and Custom Paper Cup products.Service capabilities: we provide end-to-end support from packaging selection and artwork preparation to sampling, production coordination, and delivery planning. This is especially useful for Canadian importers, wholesalers, restaurant groups, and new food brands that need both customization and practical order management. Through our Custom and Wholesale food Paper packaging service model, we help clients move efficiently from requirement review to sample confirmation and scaled production.Our approach is shaped by a simple belief: packaging should be safe for food, reliable for operations, attractive for brands, and more responsible in material choice. Buyers who want to learn more about our manufacturing background can also visit our company profile.Start with material traceability, coating suitability, leak testing, and warehouse discipline. These four areas directly affect whether the bowls will perform reliably after shipping and during actual food-service use in Canada.Yes. PE-lined bowls remain widely used because of reliable liquid and grease resistance. However, many buyers are also exploring PLA-lined or other lower-impact options as sustainability expectations and policy discussions continue to evolve toward 2026.Look for batch records, test reports, organized packing lines, export carton quality, palletization standards, and clear answers on shipment documentation and lead times. Experienced exporters usually have established routines for container loading and destination labeling.Popular categories include soup bowls, salad bowls, noodle bowls, poke bowls, dessert bowls, deli bowls, and combo takeaway bowls with matching lids. Demand is strong among restaurants, delivery kitchens, food trucks, caterers, and wholesale distributors.Paper is sensitive to moisture. Poor humidity control can affect print quality, die-cut accuracy, forming stability, and carton strength. This can lead to leaks, deformation, or shipping damage.It can simplify artwork management, production scheduling, loading efficiency, and brand consistency. Many Canadian buyers prefer coordinated sourcing of bowls, cups, and food containers to reduce complexity.Both are essential. Machines produce the bowl, but the lab proves whether the bowl meets specification consistently. Without testing, even a modern production line can produce unnoticed defects.Watch for stronger sustainability requirements, growth in compostable or lower-impact linings, more digital traceability, lightweight structural optimization, and packaging designed specifically for delivery performance and premium branding.Absolutely. It helps verify whether the supplier can move from sample quality to repeatable production. This is especially valuable for emerging restaurant brands and private-label distributors entering competitive Canadian markets.For a meaningful evaluation, allow enough time to inspect materials, production flow, testing, packaging, and management discussion. A rushed visit focused only on finished samples usually misses the most important operational details.