Verify Packaging Supplier Capacity for Canada Growth
Verify Packaging Supplier Capacity for Canada Growth
Quick Answer: What a Reliable Packaging Capacity Supplier Must Prove

Before scaling a packaging program in Canada, buyers should verify more than a supplier’s website, catalogue, price list, or stated daily output. A reliable packaging supplier must prove that it can manufacture the specific food-service packaging required, maintain material consistency, test product performance, trace each batch, respond to defects, and reserve production capacity when demand increases.
For restaurant chains, distributors, grocery programs, meal-kit companies, cafés, and institutional buyers, supplier capacity verification should be evidence-based. Ask for machinery lists, production records, quality-control reports, material specifications, sampling records, batch codes, lead-time history, and corrective-action examples. Then validate the information through white samples, printed pre-production samples, pilot orders, and measurable acceptance criteria.
A supplier may claim it produces 120,000 units per day, but that figure is useful only if it relates to the product category, material construction, printing coverage, order mix, shift arrangement, and quality standard that your Canadian business needs. A factory that runs plain paper cups at high speed may have very different output for custom printed bowls, compostable trays, grease-resistant burger boxes, or multi-compartment meal containers.
Canadian importers should also assess port planning and domestic delivery needs. Orders entering through Vancouver, Prince Rupert, Montréal, Halifax, or Toronto-area distribution networks require dependable documentation, realistic production scheduling, and packing configurations suited to container utilization and inland transport. Capacity is therefore a combination of machines, people, quality systems, logistics discipline, and communication.
| Verification Area | What the Buyer Should Request | Why It Matters |
|---|---|---|
| Factory role | Business licence, factory address, production photos and audit access | Confirms whether the supplier controls manufacturing |
| Product-specific equipment | Machine list, tooling details and production video | Shows whether equipment matches your packaging format |
| Capacity records | Shift plans, monthly output and production schedules | Tests whether claimed volume is repeatable |
| Materials | Paperboard, coating, ink and food-contact documentation | Reduces compliance and consistency risks |
| Quality control | Inspection plans, laboratory reports and defect records | Demonstrates that output is controlled, not merely produced |
| Traceability | Lot codes, material records and shipment batch files | Supports investigations, recalls and claim resolution |
| Sampling | White samples, printed samples and functional prototypes | Confirms real performance before scale-up |
The table above gives a practical starting point. A buyer should not treat every item as a document-only exercise. The strongest approval process combines paperwork, a factory review, samples, independent inspection where appropriate, and a pilot shipment that tests the supplier’s actual execution.
How to Evaluate a Packaging Capacity Supplier

Supplier evaluation should begin with the product requirement, not the supplier’s marketing profile. Define the food type, filling temperature, intended hold time, capacity, dimensions, print design, coating preference, lid compatibility, carton pack quantity, annual demand, seasonal peaks, destination province, and required compliance documents. This specification becomes the benchmark used to evaluate every supplier.
For Canada, packaging requirements can vary by end use and customer expectations. A quick-service restaurant in Toronto may need high-volume branded hot-drink cups with stable lid fit. A meal-prep company in Calgary may prioritize microwave suitability, grease resistance, compartment integrity, and stackability. A seafood distributor in Halifax may focus on moisture performance and cold-chain durability. A Vancouver café group may request FSC-related material documentation and lower-plastic packaging options.
Evaluate suppliers across six linked areas: actual manufacturing role, equipment fit, demonstrated capacity, material and laboratory controls, communication during development, and performance after approval. A low unit price cannot compensate for missed launches, ink variation, leaking containers, incomplete certificates, or inconsistent replenishment.
Buyers should distinguish between nominal capacity and available capacity. Nominal capacity is the theoretical maximum output under ideal conditions. Available capacity is the volume the supplier can commit to after existing orders, changeovers, maintenance, labour shifts, yield loss, and quality inspection. For a Canadian chain rollout, available capacity is the more relevant number.
This market-growth chart is an illustrative demand index for planning purposes. It highlights why supplier verification matters: as food-service packaging demand rises, suppliers with weak scheduling, limited tooling, or fragmented subcontracting may struggle to maintain delivery and quality during peak seasons.
Factory, Trader or Converter: Identify the Actual Role

A supplier can play several roles in the supply chain. A factory owns and operates core production processes. A converter may purchase paperboard or printed roll stock and transform it into finished packaging. A trader may coordinate products from several factories. None of these models is automatically unsuitable, but buyers must understand who controls each step and who remains accountable for quality, delivery, and corrective action.
A direct factory relationship can provide stronger control over custom tooling, production schedules, in-process quality checks, and rapid troubleshooting. A trader may be useful when a buyer needs many unrelated product categories, but the trader should clearly disclose factory sources and maintain consistent documentation. A converter can be capable where specialized forming or finishing is required, provided incoming materials and finished goods are controlled effectively.
| Supplier Role | Typical Strength | Primary Risk | Verification Method |
|---|---|---|---|
| Direct factory | Control of production, tooling and schedule | May have a narrower range of products | Review facility, machines, shift records and batch files |
| Converter | Specialized forming, finishing or assembly | Dependency on upstream material suppliers | Check incoming-material inspection and supplier approvals |
| Trader | Broader sourcing and consolidated purchasing | Limited direct production control | Request factory disclosure and traceable source records |
| Printing specialist | Advanced print management and colour matching | May outsource forming and packing | Confirm who owns final product accountability |
| Packaging assembler | Flexible mixed-SKU packs | Possible inconsistency between component suppliers | Audit incoming checks and final assembly procedures |
| Local distributor | Canadian stockholding and local service | Limited influence on overseas production | Review source factory approval and inventory practices |
The table shows why a supplier’s role should be documented before quotation approval. If a supplier presents itself as a factory but cannot provide plant information, machinery evidence, production records, or batch control documentation, the buyer should treat the relationship as a trading arrangement until proven otherwise.
For high-volume Canadian programs, ask one direct question: “Which legal entity produces this exact item, and which entity is responsible if the approved specification is not met?” The answer should be reflected in the purchase agreement, sample approval sheet, inspection standard, and claim process.
Check Equipment Against the Product You Need
Product-specific equipment determines whether capacity claims are meaningful. Paper cup production requires different equipment and control points than burger box converting, salad bowl forming, tray production, or compartment meal-box assembly. Buyers should request machine information that connects directly to their product specification rather than accepting a generic statement about automated lines.
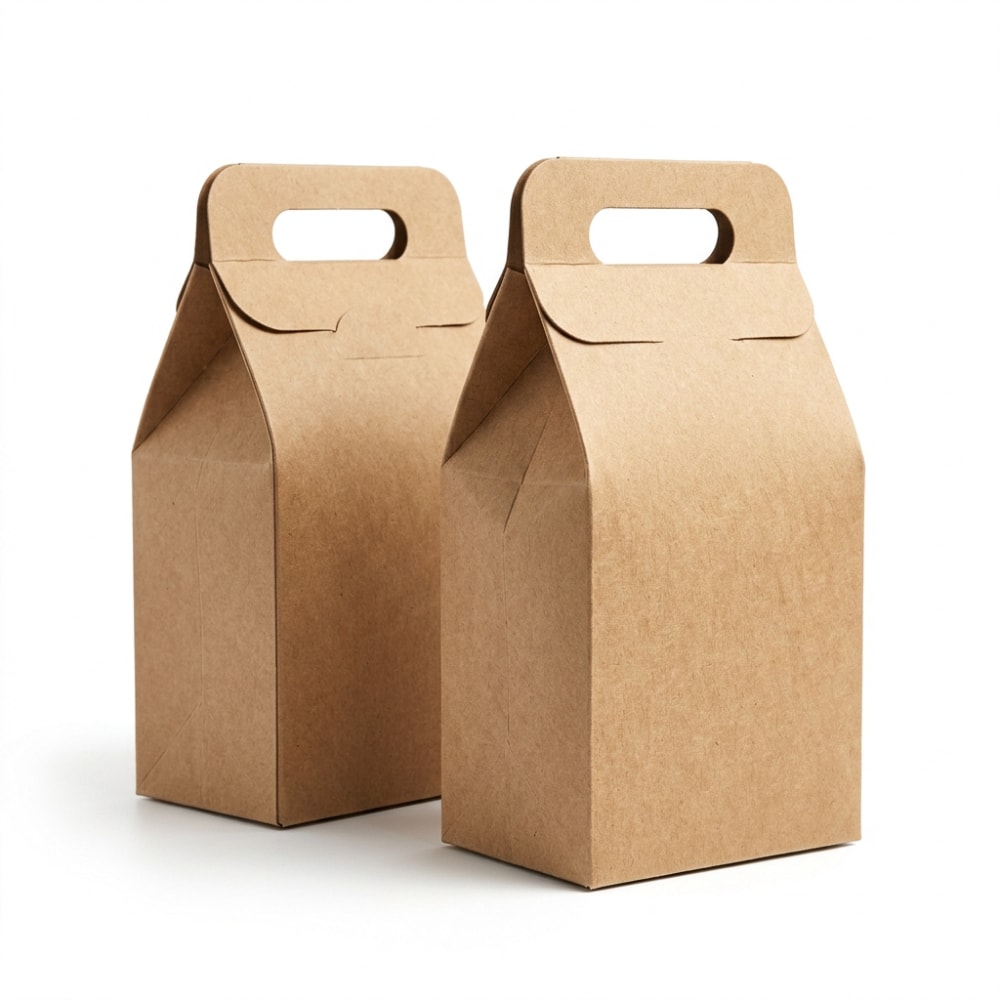
For example, a custom paper cup program may require cup-forming machines sized for the selected diameter and height, bottom knurling controls, side-seam sealing capability, roll-fed printing, inspection systems, and compatible lid testing. A kraft lunch-box program may require die-cutting equipment, creasing control, folding and gluing capability, food-safe adhesive management, compression-strength testing, and carton packing lines.
Equipment verification does not require a buyer to become an engineer. The objective is to establish whether the supplier has appropriate machinery, enough tooling, documented maintenance, trained operators, backup options, and inspection controls. A video call from the production floor, dated machine photos, maintenance records, and sample runs are often more useful than a long marketing presentation.
| Packaging Product | Key Equipment to Verify | Critical Performance Check | Useful Sample Test |
|---|---|---|---|
| Hot paper cups | Cup-forming, sealing and rim rolling machines | Side seam and bottom leak resistance | Hot-water hold test and lid-fit check |
| Paper bowls | Bowl-forming line and curling equipment | Rim strength and coating continuity | Soup or noodle holding test |
| Burger boxes | Die-cutting, creasing and folding machines | Grease resistance and closure accuracy | Warm food compression test |
| Salad containers | Forming equipment and lid-matching tooling | Stackability and moisture resistance | Cold-food transport test |
| Noodle boxes | Die-cutting, folding and adhesive application | Leak prevention at folds | Sauce retention and carry test |
| Food trays | Press forming and trimming machines | Load bearing and nesting consistency | Weight-load and stacking test |
| Meal boxes | Multi-cavity forming and compartment tooling | Compartment separation and lid fit | Mixed-food transport test |
This equipment-to-product matrix helps procurement teams ask focused questions. It is especially important for buyers developing custom food packaging for multi-location operations, where a small dimensional deviation can affect automated filling, lid supply, carton packing, or store-level inventory.
Fude Packaging supports packaging categories including cups, bowls, boxes, trays, and multi-compartment meal packaging. Buyers can review the available food packaging product range when building a multi-SKU sourcing plan. Consolidating compatible categories under one verified manufacturing partner can simplify colour management, inspection standards, shipment consolidation, and replenishment planning.
Verify Capacity With Production Records
Real capacity is verified through records, not declarations. Request monthly production output for similar products, machine utilization information, current production schedules, lead-time performance, planned maintenance dates, order backlog, and available tooling. If seasonal demand is expected, ask how the supplier will reserve capacity for promotions, restaurant openings, or annual chain rollouts.
A useful verification method is to compare claimed output with the supplier’s schedule. If a factory claims high daily production but has limited machines, long changeover times, or a full backlog, the available capacity may be much lower than expected. Likewise, a factory may have substantial output but insufficient printing capacity for a complex branded order.
For Canadian buyers importing by sea, capacity needs to be planned backwards from required arrival dates. Consider production time, inspection, export packing, container loading, port departure, ocean transit, customs clearance, rail or truck movement, and delivery to warehouses in the Greater Toronto Area, Montréal, Edmonton, Calgary, or Vancouver. A supplier that completes products quickly but cannot document readiness accurately can still disrupt the launch schedule.
The industry-demand chart illustrates why capacity planning must reflect the buyer’s market segment. Quick-service restaurants and coffee programs often require frequent replenishment, while grocery prepared-food programs may require stronger packaging performance, retail-ready carton packing, and more stringent print consistency.
| Production Record | What to Look For | Warning Sign |
|---|---|---|
| Monthly output report | Consistent volumes for similar SKUs | Unexplained spikes or incomplete data |
| Production plan | Defined order sequence and delivery dates | Orders listed without machine allocation |
| Machine utilization | Reasonable capacity reserve for urgent demand | Constant operation with no maintenance allowance |
| Changeover history | Time required for size, print or tooling changes | Assumptions that ignore custom setup time |
| On-time delivery record | Performance over several recent months | Only selective examples are provided |
| Yield and scrap data | Stable conversion yield and defect management | High scrap with no corrective-action evidence |
| Peak-season plan | Reserved machines, materials and labour | No strategy for promotional or holiday demand |
The records in this table should be reviewed together. A supplier can have sufficient machinery but still be unreliable if material shortages, changeover delays, poor yield, or weak planning prevent it from producing conforming goods when needed.
Review Laboratory and Traceability Systems
Food packaging capacity includes quality capacity. A supplier that can produce large volumes but cannot test, identify, isolate, and correct nonconforming product exposes the buyer to significant operational risk. Canadian buyers should review incoming-material controls, in-process inspections, finished-product testing, batch records, retained samples, and complaint-handling procedures.
Testing should match the product application. Depending on the packaging format, relevant checks may include basis weight, thickness, dimensions, compression strength, hot-water resistance, leak resistance, grease resistance, odour, print adhesion, colour accuracy, lid fit, stacking behaviour, and carton drop resistance. Food-contact documentation should align with the intended material system and destination-market requirements.
Traceability should allow a supplier to identify the paperboard, coating, ink, production date, machine, operator group, inspection result, packing lot, and shipment linked to a specific customer batch. This is important when products are distributed through Canadian warehouses or supplied to hundreds of restaurant locations. If a complaint occurs, the supplier should be able to identify affected lots without recalling unrelated stock.
The trend-shift chart reflects a growing procurement focus on traceability, responsible fibre sourcing, documented food-contact compliance, and measurable performance. By 2026 and beyond, buyers are expected to demand more digital records, faster lot-level investigations, and clearer sustainability evidence rather than broad environmental claims.
Fude Packaging operates a self-owned manufacturing base of approximately 30,000 m² in Shandong and uses in-house quality and performance testing to support controlled production. Its manufacturing approach includes incoming material review, production monitoring, finished-goods inspection, and full-batch traceability. For Canadian buyers, this type of documented control can help support consistent procurement across cups, bowls, boxes, trays, and meal-packaging formats.
Test Communication During Sampling
Sampling is not simply a product test; it is also a service test. The supplier’s responsiveness, technical questions, artwork review, change control, sample labelling, and problem-solving approach during sampling often predict how the supplier will perform after the purchase order is issued.
Send a structured sample brief that includes artwork, dieline, dimensions, paperboard preference, coating expectation, Pantone references if applicable, food type, temperature, hold time, expected stacking, lid requirement, order forecast, and destination. The supplier should identify unclear points before making a sample. A supplier that says “no problem” to every request without asking technical questions may not understand the application risk.
Canadian buyers should test samples under realistic conditions. Fill cups with hot coffee, cold beverages, soup, gravy, noodles, salads, fries, or oily foods as applicable. Check leakage after the expected hold time. Assess carton strength after warehouse handling. Test printed packaging under store lighting. Confirm that lids fit consistently and that packaging stacks correctly on shelves, service counters, and delivery vehicles.
| Sampling Stage | Buyer Check | Supplier Capability Indicator |
|---|---|---|
| Initial inquiry | Does the supplier ask about food and temperature? | Application-focused communication |
| Artwork review | Are bleed, dieline and colour issues identified? | Print-control discipline |
| White sample | Are dimensions and structure correct? | Tooling and forming accuracy |
| Printed sample | Are colours, text and registration acceptable? | Brand-consistency capability |
| Functional prototype | Does it pass use-condition testing? | Material and structural understanding |
| Pre-production approval | Is the approved standard documented? | Repeatable mass-production control |
| Pilot order | Does shipment match the approved sample? | Execution under commercial conditions |
The sampling process should end with an approval record, not an informal email alone. The record should state the approved material, dimensions, artwork version, colour tolerance, packing configuration, defect limits, test requirements, sample date, and authorized buyer contact. This creates a repeatable standard for future purchase orders.
Fude Packaging offers digital proofs, white samples, printed pre-production proofs, and functional sample options for customized projects. Its custom packaging service can support artwork and dieline review, material recommendations, prototype development, testing discussions, export packing, and production scheduling for Canadian import programs.
Use a Weighted Supplier Scorecard
A weighted scorecard creates a practical way to compare suppliers objectively. It is especially useful when procurement teams are evaluating a local Canadian distributor, an overseas manufacturer, a converter, and a trading company at the same time. Weight the factors according to business risk rather than choosing solely by lowest quoted price.
For a chain with strict brand standards, printing, batch consistency, traceability, and lead-time reliability may deserve high scores. For a distributor purchasing stock packaging, inventory availability, minimum order quantities, domestic freight, and warehouse service may receive more weight. The scorecard should be updated after sampling and again after the first commercial shipments.
| Evaluation Criterion | Suggested Weight | Evidence Required | Target Score |
|---|---|---|---|
| Product performance | 20% | Functional samples and test reports | 90/100 or above |
| Available production capacity | 15% | Schedules, output records and contingency plan | 85/100 or above |
| Quality and traceability | 15% | Inspection system, lot records and complaint process | 90/100 or above |
| Compliance documentation | 15% | Food-contact and material documentation | 90/100 or above |
| Commercial competitiveness | 10% | Total landed-cost comparison | 80/100 or above |
| Communication and development | 10% | Sampling response and technical clarity | 85/100 or above |
| Delivery reliability | 10% | On-time records and logistics plan | 85/100 or above |
| Corrective-action capability | 5% | Documented root-cause and closure examples | 80/100 or above |
The scorecard above ensures that total procurement risk is visible. A supplier with a slightly higher unit price but stronger traceability, reliable production capacity, and better communication may reduce overall cost by preventing stock-outs, product failures, reprints, emergency air shipments, and customer complaints.
This comparison chart demonstrates the difference between a verified manufacturing partner and an unverified general supplier. The values are planning benchmarks, not a substitute for an individual supplier audit. Buyers should use their own scorecard results, samples, records, and inspection findings when making a sourcing decision.
Fude Packaging: 20+ Years, 30,000 m² Factory, 120,000 Units per Day
Fude Packaging supports overseas B2B buyers with more than 20 years of packaging experience, a self-owned production base of approximately 30,000 m², and automated capacity of up to 120,000 units per day, depending on product specification and production mix. The company serves food-service packaging programs requiring cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, food trays, and multi-compartment meal packaging.
Its technological capabilities include automated production lines, in-house laboratory support, material evaluation, printing controls, forming processes, and functional testing. Customers can request digital proofing, white samples, printed pre-production samples, and prototype evaluations to confirm structure, dimensions, capacity, print appearance, heat performance, grease resistance, leak prevention, and lid compatibility before mass production.
Its manufacturing capabilities are based on direct control from material selection and printing through die-cutting, forming, inspection, packing, and shipment preparation. Full-batch traceability supports lot-level investigation, while documented systems can support BRC, FSC, ISO 9001, LFGB, FDA-related, and other project-specific documentation needs. Buyers should confirm the exact documentation required for their materials, end use, and Canadian market channel.
Its service capabilities include OEM and ODM support, artwork and dieline checking, Pantone matching, custom-size development, scheduled-order planning, export packing, and coordination for sea, air, full-container, less-than-container, and express sample shipments. Fude Packaging has served more than 500 business clients and can support programs that require repeat ordering, multi-SKU consolidation, and production planning.
For buyers seeking a direct manufacturing partner, learn more about Fude Packaging’s factory and quality approach. For a Canadian import project, the most useful first step is to provide product drawings, forecast volume, sample requirements, expected arrival dates, and the destination port or warehouse location.
FAQ: Verifying Packaging Supplier Capacity Before Scaling
1. How can I verify that a packaging supplier is a real factory?
Request the legal factory name, production address, business registration, product-specific machine list, facility photos, production videos, quality records, and batch-control examples. Where the purchase risk is substantial, arrange a remote audit, in-person audit, or third-party inspection. Confirm that the entity issuing the quotation is connected to the entity producing the goods.
2. Which production records should Canadian buyers review?
Review monthly production output, current order schedules, machine allocation, utilization, tooling availability, maintenance plans, on-time delivery history, yield reports, inspection records, and peak-season planning. Ask for records relevant to similar products rather than generic factory totals.
3. How is real available capacity confirmed?
Compare the supplier’s stated capacity with its existing production backlog, machine count, shift system, changeover time, material availability, and planned maintenance. Confirm how much output can be reserved for your order and how the supplier will respond if demand increases unexpectedly.
4. What should be tested during sampling?
Test dimensions, volume, print quality, colour accuracy, stacking, lid fit, leak resistance, grease resistance, heat performance, compression strength, carton integrity, and suitability for the intended food. Use actual serving conditions whenever possible, including holding time, transport, refrigeration, and reheating requirements.
5. Which supplier KPIs matter after approval?
Track on-time delivery, defect rate, complaint response time, corrective-action closure, batch traceability accuracy, print consistency, sample-to-production conformity, order-fill rate, documentation completeness, and response time for replenishment requests. Review these KPIs quarterly for high-volume or multi-location programs.
6. Should I use a Canadian supplier or an overseas manufacturer?
The best choice depends on order volume, customization, lead-time needs, warehousing strategy, and total landed cost. Canadian suppliers can offer fast domestic replenishment and local stock. Overseas direct manufacturers can offer stronger customization, scale, and category consolidation for planned volume. Many buyers use both: domestic inventory for urgent demand and direct import programs for core, forecastable SKUs.
7. What are the key 2026 packaging supplier trends?
Key trends include more digital batch records, stronger demand forecasting, automated visual inspection, material traceability, lower-plastic packaging designs, responsible fibre sourcing, improved recyclability or compostability claims verification, and tighter alignment between sustainability statements and real product performance. Buyers should prioritize suppliers that can document these capabilities rather than relying on broad promotional language.
To discuss packaging capacity, custom samples, product specifications, or a Canada-focused shipping plan, contact Fude Packaging’s international packaging team. A structured inquiry with product type, order quantity, artwork, application, destination city, and required delivery date will support a faster and more accurate evaluation.
About the Author
Fude Packaging is a professional flexible packaging manufacturer serving global food brands, wholesalers, and distributors. Our team shares practical insights on custom packaging, printing technology, food-safe materials, and industry trends to help businesses build better packaging solutions.
Share
Product Category
Start Your Project With Fude Today
Related Post
-

Starting Sustainable Packaging in the United States
The United States food service market is changing quickly. Restaurants, ghost kitchens, meal-prep brands, grocery delis, convenience stores, campuses, and delivery platforms are under pressure to reduce waste, meet stricter packaging expectations, and protect food quality at the same time. That is why many entrepreneurs are asking whether 2026 is the right time to enter sustainable food packaging. The short answer is yes, but only if the business is built on practical compliance, realistic sourcing, strong logistics, and customer education rather than green claims alone.A sustainable packaging company in the United States must solve real operating problems. Buyers in New York, Los Angeles, Chicago, Houston, Atlanta, Seattle, Miami, and Phoenix are not just looking for products labeled eco-friendly. They want leak resistance, stackability, insulation, print quality, lead-time reliability, and documentation for food-contact safety. They also want packaging that fits their menu, shelf life, and branding. This makes the opportunity attractive, but it also means the winning business model must combine market intelligence with disciplined execution.In 2026, the strongest entrants will focus on product categories with recurring demand such as paper food containers, paper bowls, paper cups, deli boxes, noodle bowls, fries cups, and compartment meal boxes. They will target industries with immediate purchasing cycles, such as QSR chains, regional restaurant groups, catering companies, takeout specialists, and wholesale distributors. They will build trust by offering samples, clear technical specifications, custom print support, and a steady supply chain linked to major U.S. import and distribution corridors such as Los Angeles/Long Beach, Savannah, New York/New Jersey, Houston, and Seattle-Tacoma.If you want a quick answer on how to start a sustainable food packaging business in the United States in 2026, begin with a narrow category, validate demand with local buyers, secure compliant material sourcing, and choose a manufacturing model that protects margins without risking delivery performance. Focus first on one or two high-volume product families such as bowls and takeaway containers, then expand into cups, lids, and specialty items after you establish repeat customers.The most effective path usually follows seven steps. First, identify a customer segment with a measurable packaging pain point, such as grease leakage, poor print quality, unstable carton supply, or lack of compostable options. Second, build a product line matched to actual food applications, not abstract sustainability trends. Third, confirm regulatory requirements including food-contact safety, labeling, claims substantiation, and state-level rules. Fourth, source materials that balance functionality, cost, and environmental positioning. Fifth, develop a dependable manufacturing and logistics setup. Sixth, sell through a mix of direct outreach, distributor relationships, and digital lead generation. Seventh, keep accounts through service, customization, and replenishment planning.For most founders, the safest launch strategy is not to build a giant product catalog on day one. Instead, create a focused offer around packaging used every day by restaurants and food retailers. Examples include soup bowls for delivery, window-lid lunch boxes for grab-and-go merchandising, hot and cold beverage cups, and multi-compartment meal boxes for prepared foods. This lets you learn customer buying behavior, improve forecasting, and manage inventory risk while building authority in one profitable niche. Recommended Launch Priorities for a New Sustainable Packaging Business Priority What to Do Why It Matters Time Horizon 1 Pick one customer segment Improves positioning and speeds up product-market fit Month 1 2 Select 3 to 5 core SKUs Controls inventory complexity and sampling cost Month 1-2 3 Validate compliance documents Prevents sales delays and legal risk Month 1-2 4 Test sourcing and lead times Protects margins and customer trust Month 2-3 5 Run pilot orders with local accounts Creates case studies and repeat business Month 3-4 6 Build distributor and e-commerce channels Supports scale after initial traction Month 4-6 The table above shows why a staged rollout is usually better than a broad launch. Sustainable packaging is a repeat-order business, and repeat orders depend on consistency more than hype. A buyer who experiences one failed delivery or one mismatched lid size may not return, even if the sustainability message is strong.Before investing in products, founders should understand where demand is strongest in the United States. The biggest opportunities usually come from sectors where packaging is operationally essential and publicly visible. Quick-service restaurants, delivery-first brands, university dining, grocery prepared foods, and convenience retail all face demand for packaging that is functional, brandable, and more environmentally responsible than traditional foam or low-grade plastic alternatives.Demand also varies by geography. Coastal states and major metro areas often move faster on packaging changes because of local waste regulations, sustainability reporting pressure, and consumer expectations. California remains important because of its policy environment and large concentration of restaurant and retail chains. New York and New Jersey matter because of dense foodservice activity and major port access. Illinois, Texas, Georgia, and Florida are valuable because of distribution reach, regional chains, and large populations. Washington and Oregon are important for premium sustainability-driven buyers. A good market-entry plan ranks locations not only by buyer count, but by shipping economics, warehousing access, and category fit.Founders should also analyze the difference between end users and channel buyers. A restaurant owner may care about presentation and leak resistance. A wholesaler may care about carton efficiency, palletization, reorder rates, and SKU rationalization. A regional food chain may require artwork consistency, compliance documentation, and stable replenishment. Each audience responds to a different value proposition, so market research should include interviews, sample testing, competitor benchmarking, and a pricing map for comparable items.var ctx1 = document.getElementById('lineChartMarket').getContext('2d');var chart1 = new Chart(ctx1, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027', '2028'], datasets: [{ label: 'U.S. Sustainable Food Packaging Demand Index', data: [82, 89, 97, 108, 121, 134, 148], borderColor: 'rgb(75, 192, 192)', backgroundColor: 'rgba(75, 192, 192, 0.15)', fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart illustrates a realistic growth pattern for U.S. demand, showing why 2026 is a good entry point. Growth is not driven only by consumer preference. It is also driven by chain standardization, food delivery expansion, institutional procurement changes, and state-level packaging regulation. High-Potential U.S. Customer Segments for Sustainable Food Packaging Segment Main Need Best Products Typical Buying Driver Quick-service restaurants Low-cost, high-volume packaging Meal boxes, cups, bowls Consistency and price Delivery kitchens Leak-proof transport packaging Noodle bowls, compartment containers Food integrity in transit Grocery deli programs Display-friendly grab-and-go packs Window-lid boxes, deli containers Shelf appeal Cafes and beverage chains Branded cup programs Hot cups, cold cups, lids Brand visibility Caterers and meal prep brands Portion control and stackability Compartment boxes, trays Operational efficiency Wholesalers and distributors Reliable mixed-SKU supply Full product line Availability and margin The table shows that one product line does not fit every segment. Founders who tailor the product range to buyer needs usually close business faster and reduce sample waste.Another key part of market research is competitor mapping. In the United States, you will compete with domestic converters, importers, broadline distributors, local print shops, and low-cost commodity sellers. Your advantage may come from better customization, more flexible MOQs, stronger technical support, or better alignment with premium branding. It may also come from serving underserved mid-sized buyers who need more than a standard catalog but less than a national account program.Product development in sustainable packaging should begin with food application. A soup concept needs different barrier performance than a salad bowl. A fried snack requires oil resistance, while a fruit pack needs moisture control and visual presentation. If you build products around real menu use, you will naturally make better decisions on board weight, coatings, lid types, and structural design.In the U.S. market, the most commercially useful materials include responsibly sourced paperboard, kraft paper, bleached paperboard, food-grade PE-lined substrates, and PLA-based compostable options where local composting infrastructure and customer demand support them. Sustainable positioning should be matched with operational truth. For example, a compostable coating may sound attractive, but if the buyer needs long hold times for hot liquid foods, performance must come first. A failed package creates waste too.For a startup, a practical range may include paper bowls for soups, salads, and grain dishes; takeaway boxes for burgers, rice meals, and fried foods; and hot or cold cups for beverage programs. A brand can later extend into custom sleeves, lids, trays, and seasonal packaging. To evaluate product opportunities, compare annual demand, reorder frequency, freight efficiency, print area, customization appeal, and complaint risk.If you are building a catalog, it is useful to review proven product types already accepted by global food service buyers, including Custom Paper Food Container products, Custom Paper Bowl products, and Custom Paper Cup products. These categories reflect the kinds of high-turn items that work well across U.S. restaurants, takeout operators, and distributors. Product Categories and Material Selection Guide Product Type Common Food Use Material Option Key Performance Requirement Lunch box Rice meals, sandwiches, combo meals Kraft or white paperboard with PE or PLA option Leak resistance and structure Paper bowl Soup, noodles, salads Heavy paperboard with food-grade lining Heat tolerance and sealing Paper cup Coffee, tea, cold drinks Single, double, or ripple-wall cup stock Insulation and print quality Fries cup Fried snacks and sides Oil-resistant kraft paper Grease control Deli box Bakery, salads, ready meals Paperboard with clear window lid options Visibility and portability Compartment meal box Prepared meal programs Rigid food-grade paperboard Portion separation This table matters because product-market fit in packaging is driven by performance details. Buyers usually reorder based on whether the item survives storage, filling, transport, and customer use without complaints.When sourcing materials, ask suppliers to document paper origin, coating specifications, migration safety, certification status, and quality-control procedures. U.S. buyers increasingly ask for FSC-related sourcing assurance, food-contact declarations, and supporting documentation for compostability claims. Price is still important, but professional buyers increasingly evaluate total landed value: product performance, defect rate, customs predictability, lead time, and support responsiveness.Another product development best practice is to create a testing matrix before launch. Test for hot-fill, cold-fill, stacking pressure, grease penetration, lid fit, microwave suitability where relevant, print rub resistance, and shelf presentation. Even simple side-by-side field testing with local restaurants can reveal issues that never show up on a technical drawing.Compliance is one of the most misunderstood parts of the packaging business. In the United States, sustainable packaging is not just about using paper instead of plastic. A seller must think about food-contact safety, truth in environmental marketing, state-specific restrictions, customs documentation, and customer procurement standards. Without this foundation, it is hard to win contracts with serious buyers.The baseline requirement is food-contact safety. Packaging materials that come into direct contact with food should be supported by appropriate documentation showing compliance with relevant food-contact standards. U.S. buyers commonly ask for FDA-related conformity information. Internationally recognized systems such as ISO 9001 can also support quality credibility because they show consistent process control. If paper sourcing is part of your sustainability value proposition, FSC-related documentation is often requested. If a product is marketed as compostable, buyers may ask for BPI or OK Compost documentation depending on the target application and disposal stream.Beyond certifications, founders need to watch how they describe products. Terms such as recyclable, compostable, biodegradable, and plastic-free should be used carefully. Some products contain functional linings or components that affect disposal routes. If a claim is too broad or vague, it can create legal and reputational risk. Strong businesses train their sales teams to describe packaging accurately, including real disposal limitations in the target market. Key Compliance Areas for Selling Sustainable Food Packaging in the United States Compliance Area Why Buyers Care Typical Evidence Needed Risk if Missing Food-contact safety Protects consumers and purchasing approval FDA-related declarations and test reports Account rejection Quality management Shows process consistency ISO 9001 certificate or equivalent records Low trust in supplier control Responsible fiber sourcing Supports sustainability procurement FSC-related documentation Loss of institutional buyers Compostability claims Required for some programs and tenders BPI or OK Compost support Claim challenge or delisting Import documentation Reduces customs delays Commercial invoice, packing list, HS coding Shipment holds State and local policy fit Some cities or states restrict materials Product specification and claim review Unsellable inventory The table highlights that compliance is a sales tool, not just an administrative burden. Buyers often compare two suppliers with similar pricing and choose the one who provides complete, organized documents faster.In 2026, policy trends are expected to tighten further. More states and municipalities are likely to clarify packaging claims, increase recycled-content discussions, and push foodservice operators to document environmental commitments. Founders should design their compliance workflow early by keeping technical sheets, declarations, carton labels, sample retention records, and customer-specific specification files in one organized system.One of the biggest decisions for a new sustainable packaging business is whether to produce in-house or work with a manufacturing partner. In-house production offers greater direct control over production scheduling, quality routines, and proprietary tooling. However, it also requires high capital expenditure, labor management, factory compliance, raw-material procurement discipline, and time to reach efficient utilization.A manufacturing partnership is often the better path for early-stage businesses entering the U.S. market because it lowers startup risk and allows faster category testing. You can launch with private-label or OEM models, sample multiple SKUs, and learn actual order patterns before investing heavily in equipment. This is especially useful if you are targeting several applications such as bowls, cups, and takeaway boxes with different converting requirements.Still, not all manufacturing partners are equal. You want a supplier with technical depth, consistent capacity, and a record of serving global buyers. A strong packaging manufacturer should offer automated production, flexo printing quality, die-cutting precision, forming capability, documented QC, and warehousing that protects product integrity. It is also helpful if the partner has experience shipping into North America and understands lead-time planning around U.S. seasonality.var ctx2 = document.getElementById('comparisonChartSupplier').getContext('2d');var chart2 = new Chart(ctx2, { type: 'bar', data: { labels: ['Startup Cost', 'Speed to Launch', 'Product Flexibility', 'Margin Control', 'Operational Complexity', 'Scale Readiness'], datasets: [ { label: 'Manufacturing Partner', data: [30, 90, 85, 68, 35, 82], backgroundColor: 'rgb(153, 102, 255)' }, { label: 'In-House Production', data: [92, 45, 70, 84, 88, 76], backgroundColor: 'rgb(54, 162, 235)' } ] }, options: { responsive: true, maintainAspectRatio: false }});The comparison chart shows a realistic tradeoff. A partner model usually wins on speed and lower initial cost, while in-house production can improve direct margin control after scale. For most new entrants, the partnership route makes more sense until demand is proven. Manufacturing Model Comparison for New Packaging Businesses Factor Manufacturing Partner In-House Production Best Fit Startup investment Low to moderate High Partner for early stage Speed to market Fast Slow to moderate Partner for testing demand Customization range High if supplier is capable Depends on equipment Either, depending on setup Quality control Shared oversight Direct oversight In-house at larger scale Capacity expansion Faster if partner has equipment Requires investment Partner initially Operational complexity Lower Higher Partner for new entrants For founders who use a partner model, supplier selection becomes the core strategic task. You need to examine sampling speed, print consistency, MOQ flexibility, lead times, freight support, and willingness to co-develop new structures. It is also wise to audit how the manufacturer handles quality issues and whether it can support both small trial orders and larger wholesale replenishment programs.Marketing sustainable packaging to U.S. business customers is different from marketing consumer products. Buyers are not primarily emotional shoppers; they are operational and financial decision-makers. They care about sustainability, but they also care about usage cost, complaint rates, case pack efficiency, and whether the packaging supports their brand image. Your marketing must connect environmental value with business outcomes.The best messaging usually combines four points: food performance, compliance confidence, brand presentation, and supply reliability. For example, instead of saying only that a bowl is eco-friendly, explain that it is designed for hot soups and grain dishes, available with strong print branding, supported by food-contact documentation, and capable of stable repeat supply. That message speaks directly to procurement managers, restaurant operators, and distributors.Channel strategy matters too. LinkedIn outreach works well for chains, procurement teams, and distributor contacts. Search-focused content helps restaurants and wholesalers actively looking for alternatives. Trade shows in Chicago, Las Vegas, New York, and regional foodservice events can generate samples and buyer conversations quickly. Direct outbound sales is still important, especially for regional chains and wholesalers that want negotiated programs rather than simple online checkout.var ctx3 = document.getElementById('barChartDemand').getContext('2d');var chart3 = new Chart(ctx3, { type: 'bar', data: { labels: ['QSR', 'Delivery Kitchens', 'Grocery Deli', 'Cafes', 'Caterers', 'Distributors'], datasets: [{ label: 'Estimated 2026 U.S. Demand Potential', data: [92, 88, 79, 74, 67, 95], backgroundColor: 'rgb(255, 99, 132)' }] }, options: { responsive: true, maintainAspectRatio: false }});The bar chart shows where a startup may find the best near-term commercial returns. Distributors and QSR-related accounts often generate the highest repeat volume, while delivery kitchens can be especially attractive for specialized leak-resistant items.Sampling should be central to your marketing. Packaging is tactile and operational. Buyers want to see print, stackability, sealing, and real food performance. A disciplined sampling process with clear specifications, application notes, and follow-up feedback can outperform generic advertising. Case studies also help. If a deli chain reduces sauce leakage or improves shelf appearance after switching to a window-lid box, turn that into a sales asset.Your website should present solutions by application, not only by product name. Organize pages around takeout meals, soup and noodle service, coffee and beverage programs, and retail-ready prepared foods. That helps U.S. buyers immediately identify whether you understand their business. If you provide design support, OEM options, and wholesale programs, communicate that clearly through service-focused pages such as Custom and Wholesale food Paper packaging.It is also smart to localize your messaging around U.S. operations. Mention freight planning to West Coast and East Coast ports, support for distributors serving Dallas, Atlanta, or Philadelphia, and case-pack efficiencies for warehousing near inland hubs like Chicago or Kansas City. This makes your brand feel operationally grounded, not generic.Once a sustainable packaging company begins generating repeat orders, the next challenge is scaling without losing service quality. Packaging buyers often reorder on a schedule linked to menu cycles, store counts, and seasonal peaks. If you scale too fast without inventory planning, you risk stockouts. If you hold too much inventory, cash flow becomes strained. Good scaling depends on data, channel discipline, and logistics design.For U.S. operations, distribution strategy should balance import efficiency with regional responsiveness. Many businesses start by importing into West Coast or East Coast ports and then using third-party warehouses to serve nearby regions. For example, Los Angeles/Long Beach can be efficient for Western states, while Savannah or New York/New Jersey can support Eastern distribution. Houston can be useful for Southern coverage, and Chicago offers strong inland reach.Forecasting should be based on SKU velocity, customer reorder rhythm, case dimensions, and seasonality. Coffee cup demand may rise in colder months for some regions. Salad bowl demand may increase during spring promotions. Meal-prep businesses may spike in January. A scaling company should classify SKUs into core stock, flexible stock, and special-order items. This improves working capital and service levels.var ctx4 = document.getElementById('areaChartTrend').getContext('2d');var chart4 = new Chart(ctx4, { type: 'line', data: { labels: ['2023', '2024', '2025', '2026', '2027', '2028'], datasets: [{ label: 'Shift from Generic Packaging to Customized Sustainable Solutions', data: [28, 35, 43, 55, 66, 76], fill: true, backgroundColor: 'rgba(75, 192, 192, 0.25)', borderColor: 'rgb(75, 192, 192)', tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The area chart reflects a major trend for 2026 and beyond: buyers are moving from generic commodity packaging toward customized and more sustainability-oriented solutions. This shift creates room for companies that combine supply discipline with customization expertise. Scaling Framework for U.S. Packaging Distribution Stage Primary Sales Channel Inventory Approach Main Risk Launch Direct local accounts Low inventory, sample-heavy Slow conversion Early traction Regional restaurant groups Stock top 3-5 SKUs Forecast errors Growth Wholesalers and distributors Multi-SKU replenishment planning Margin compression Expansion Multi-state programs Regional warehousing Service inconsistency Maturity Chain and contract accounts Forecast-based stocking Large-account dependency Optimization Balanced channel mix Demand-classified inventory Complexity overload The table shows that scale is not just about more sales. It requires channel strategy and inventory governance. Many packaging startups fail because they confuse revenue growth with supply-chain maturity.Technology can support this scaling phase. In 2026, expect more buyers to request digital proofs, reorder dashboards, artwork version control, and more precise carton-level traceability. Businesses that invest in structured data, customer-specific spec management, and clear reorder workflows will be easier to do business with. Sustainability reporting may also become more integrated into procurement, so packaging suppliers should be ready to share material and certification information in a standardized way.In packaging, the first order is not the main win. The real value comes from repeat business over years. Long-term customer relationships are built through consistency, communication, and product evolution. A restaurant chain, distributor, or food retailer wants to know that you can support them as their menu, store count, and sustainability goals change.One of the best retention tools is proactive account management. Do not wait for a customer to complain. Check reorder patterns, ask about usage issues, review seasonality, and offer packaging optimization ideas. A simple adjustment such as changing the bowl lid fit, upgrading grease resistance, or improving carton labeling can strengthen the relationship significantly. Customers remember suppliers who solve problems before they become expensive.Another retention driver is co-development. Businesses that help customers improve branding, optimize pack sizes, or launch new menu items become harder to replace. This is especially true for buyers that value OEM and private-label packaging. Custom printing, structural refinement, and application-specific recommendations add value beyond unit price.Case studies can be built into account management. For example, a regional salad chain may switch to stronger paper bowls with clear branding and improve both delivery performance and social-media presentation. A deli retailer may adopt window-lid meal boxes that increase grab-and-go appeal. A coffee chain may move to double-wall cups that improve handling and reduce sleeve usage. These outcomes strengthen both sales and customer loyalty.To keep customers long term, create a service model that includes sample refreshes, artwork file support, reorder reminders, QC communication, and freight visibility. Strong service often decides renewals when prices across the market become more competitive.For U.S. buyers looking for a dependable packaging partner rather than a simple trader, Shandong Fude Packaging Co., Ltd. offers a practical combination of technical capability, manufacturing depth, and responsive service. The company has been serving the global food service packaging market for more than two decades and supports restaurants, chains, wholesalers, distributors, and emerging brands across multiple regions, including North America.From a technological capability perspective, Fude has built expertise around food-grade paper and plastic packaging development with attention to structural performance, print execution, and eco-material options. Its production environment supports flexo printing, die-cutting, forming processes, and quality-lab inspection, helping customers achieve packaging that is not only sustainable in positioning but also usable in demanding takeaway, delivery, and retail settings. This matters in the United States, where buyers increasingly want packaging that performs well in transit, stacks neatly in storage, and carries clear brand graphics.From a manufacturing capability perspective, the company operates a modern factory of about 30,000 square meters with automated lines and climate-conscious warehousing support. Its scale allows it to handle both routine wholesale demand and customized projects without relying on unstable small-batch operations. Product lines include kraft and white lunch boxes, trays, bowls, beverage cups, deli boxes, fries cups, and compartment meal packaging, making it easier for buyers to consolidate sourcing. This breadth is useful for importers and distributors who want a one-stop supplier for foodservice packaging categories rather than managing multiple fragmented vendors.From a service capability perspective, Fude supports customers through packaging selection advice, artwork preparation, sampling, customization review, and delivery coordination. The process is built around requirement confirmation, sample and design approval, then production and shipment. Flexible MOQs and typical lead times suited to both trial orders and ongoing wholesale replenishment help reduce entry risk for U.S. businesses. Buyers exploring a long-term sourcing relationship can learn more through the company overview at our company profile and service resources that explain custom development and order support.For startups and established buyers alike, a partner with experience in FDA-related, FSC, ISO 9001, and compostability-oriented documentation can simplify onboarding and procurement review. Just as important, a capable manufacturer can support private-label growth as a U.S. customer moves from testing a small number of SKUs to launching broader packaging programs across bowls, cups, and containers.1. What is the best niche to start with in the United States?For most new entrants, the best starting niche is high-turn foodservice packaging with repeat demand, such as paper bowls, takeaway meal boxes, or branded paper cups. These categories are used frequently and support repeat ordering.2. Should I focus on compostable products only?Not necessarily. Compostability can be attractive, but the right product depends on food application, local disposal realities, and customer expectations. Some buyers prioritize durability and cost first, then want the most responsible material option within those constraints.3. How much product variety should I launch with?Start with a narrow range, usually 3 to 5 core SKUs. A focused launch improves forecasting, simplifies sampling, and helps you learn faster which items create repeat business.4. Is importing sustainable packaging into the United States viable for a new business?Yes, if you control documentation, freight planning, and supplier quality. Many successful businesses use overseas manufacturing with regional U.S. warehousing to maintain balance between cost and service.5. What certifications matter most?Food-contact compliance support is essential. Beyond that, buyers often value ISO 9001 for quality systems, FSC-related documentation for responsible paper sourcing, and BPI or OK Compost evidence when compostability claims are relevant.6. How do I win buyers away from existing suppliers?Lead with a clear commercial advantage: better print quality, improved leak resistance, flexible MOQs, faster sample support, stronger compliance documents, or more reliable delivery. Sustainable messaging helps most when paired with measurable business benefits.7. Which U.S. regions are best for early expansion?California, Texas, New York/New Jersey, Illinois, Georgia, and Florida are often strong starting points because they combine foodservice scale, distribution infrastructure, and access to major logistics corridors.8. Do I need custom printing from the beginning?Custom printing is not mandatory at launch, but it is a powerful growth lever. Many restaurants and beverage brands want packaging that reinforces their identity, especially on cups, bowls, and takeaway containers.9. How important is warehouse strategy?Very important. Packaging is bulky, and freight economics strongly affect margins. A good U.S. warehouse plan improves lead times, lowers shipping friction, and supports repeat ordering.10. What trends will shape 2026 and beyond?Expect stronger policy scrutiny, growing demand for verified sustainability claims, increased customization, smarter inventory systems, and more buyer interest in suppliers that can combine compliance, design, and dependable replenishment.Starting a sustainable food packaging business in the United States in 2026 is a real opportunity, but success depends on building a business that works in the field, not just on a sales deck. The market rewards founders who understand food applications, respect compliance, choose the right supplier model, and create trust through service. If you align products with buyer operations, use realistic sustainability claims, and plan for scale through disciplined distribution, you can build a packaging brand that grows with the changing U.S. food service economy. -

Canada Kraft Concession Tray Pricing: Buyer Guide
Pricing for fast-service kraft concession trays in Canada is shaped by much more than the quoted cost per piece. Paper grade, board weight, grease-resistant coating, tray size, folding structure, printing coverage, order quantity, carton density, shipping mode, customs handling, storage space and performance risk all affect the real landed cost. A small plain fries tray may appear inexpensive, but the cost difference can quickly narrow if it nests poorly, transfers grease to customers’ hands, collapses under loaded fries, or occupies excessive warehouse space.For Canadian venue operators, food-service distributors, stadium concessionaires, cinemas, quick-service restaurants and event caterers, the most reliable buying method is to compare equivalent specifications. Request samples, record measurable acceptance requirements, test denesting speed and grease resistance, confirm carton dimensions, and separate tooling or print-plate costs from recurring unit costs. This approach helps buyers in Toronto, Vancouver, Montréal, Calgary, Edmonton and Halifax avoid choosing a lower headline price that creates higher operating costs later.A practical quotation should identify the tray’s dimensions, paper GSM, food-contact coating, print colours, packing format, pieces per carton, carton cube, production lead time, Incoterms, shipment method and documentation. Buyers should also verify whether the price includes a digital proof, white sample, printed pre-production sample, testing, inspection support and export packing.Cost ElementWhat It CoversEffect on Total CostBuyer CheckPaperboardKraft paper grade, fibre quality and board weightHighConfirm GSM and food-contact suitabilityCoatingGrease, moisture or heat resistanceMedium to highTest with fries, poutine and sauced foodsFormingDie-cutting, folding, gluing and nesting designMediumMeasure denesting and tray stabilityPrintingInk coverage, number of colours and finishMediumCheck Pantone and artwork requirementsMOQMinimum production quantity and run lengthHigh for custom ordersAsk for price breaks by volumeFreight cubeCarton volume, pallet use and container utilizationHigh on lightweight traysCompare cost per 1,000 landed piecesFailure costLeaks, weak laps, slow service and customer complaintsPotentially very highApprove samples against defined criteriaThe table shows why a unit-price-only comparison is incomplete. Paper trays are lightweight products, so freight cube can become proportionally important, especially when shipping to inland Canadian markets such as Winnipeg, Regina, Saskatoon or Ottawa. A tray that packs more efficiently may cost slightly more at the factory but reduce ocean freight, domestic drayage, warehouse handling and storage costs.The base price begins with the material specification. Natural kraft board can vary in fibre composition, strength, colour consistency and surface smoothness. Heavier board often improves rigidity, but it also increases raw-material consumption. Food-service trays intended for fries, chicken tenders, nachos, poutine, onion rings or loaded snacks typically require a balance between stiffness and grease resistance. Over-specifying board can increase cost unnecessarily; under-specifying it can lead to soggy bottoms, weakened corners and poor customer experience.Tray geometry is another major factor. A shallow open boat tray is generally simpler to produce than a high-wall tray with reinforced folds, locking tabs or divided compartments. Larger trays require more paperboard, while complex structures may require slower forming, higher die-cutting precision and additional quality inspection. Rounded corners, deep sidewalls, double-fold lips and anti-splay structures may improve service performance, but they should be selected because they solve an actual application problem.Canadian buyers should describe the intended food use in the request for quotation. A tray for dry popcorn at a cinema does not need the same barrier properties as a tray for poutine at a hockey arena. Similarly, a tray for hot fries served in a busy Toronto stadium needs reliable denesting and enough bottom strength to withstand rushed handling during intermission peaks.var ctx = document.getElementById('lineChart').getContext('2d');new Chart(ctx, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Estimated Canadian Demand Index for Kraft Concession Trays', data: [100, 108, 117, 126, 137, 148], borderColor: 'rgb(74, 108, 74)', backgroundColor: 'rgba(74, 108, 74, 0.12)', borderWidth: 3, fill: false, tension: 0.3 }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: false, title: { display: true, text: 'Demand Index' } }, x: { title: { display: true, text: 'Year' } } } }});The chart reflects a realistic directional trend rather than a fixed market forecast. Demand for fibre-based food-service packaging is expected to continue rising as Canadian food operators seek practical alternatives to hard-to-recycle formats, expand delivery and takeaway menus, and standardize packaging across multiple locations. However, purchasing teams should plan for paper-price volatility, freight changes and seasonal demand peaks.Paper weight is normally expressed in GSM. In general, a higher GSM board has greater stiffness and puncture resistance, but paper quality matters as much as nominal weight. A well-engineered lighter board can sometimes outperform a heavier low-quality board when fibre strength and forming are controlled. For this reason, buyers should request both the stated GSM and sample-based performance validation.Coating selection should match food exposure. Uncoated kraft may suit dry bakery items, popcorn or lightly seasoned snacks. Grease-resistant treatment may be necessary for fries, fried chicken, mozzarella sticks and poutine. For high-moisture or heavily sauced foods, buyers should assess whether an open tray is suitable at all, or whether a more enclosed food box is needed. Fude Packaging can recommend related kraft boat tray options based on portion size, food temperature and holding time.Specification ChoiceTypical UsePrice DirectionPerformance ConsiderationLightweight uncoated kraftPopcorn, dry snacks, pastriesLowerLimited grease protectionMedium-weight kraft boardFries, chicken bites, snack combosModerateGood balance of cost and rigidityHeavyweight kraft boardLoaded fries, larger sharing portionsHigherImproved bottom strengthGrease-resistant treated boardFried foods and poutineModerate to higherReduces grease migrationDeep-wall formed trayNachos, mixed snacks, larger servingsHigherBetter containment but more complex formingCompartment trayMeal sets and sampling eventsHigherMore material and tooling complexityReinforced rim designHigh-volume venue serviceModerateImproves handling and shape retentionThis comparison is useful when preparing an RFQ. Instead of asking only for “kraft trays,” describe the food, serving temperature, portion weight, expected hold time and service environment. A distributor supplying summer festivals in Vancouver may need a compact tray that performs outdoors in variable weather, while a Montréal cinema may prioritize fast denesting, branded printing and consistent case counts.Plain kraft concession trays usually have the lowest recurring unit cost because they avoid artwork preparation, printing plates, ink consumption, colour controls and proofing steps. They are often a sensible choice for wholesalers, independent snack bars, temporary events and operators that use generic packaging across several brands.Custom-printed trays can support brand recognition, promotional campaigns, venue sponsorships and menu positioning. The print cost depends on the number of colours, total ink coverage, artwork complexity, registration tolerance and required print finish. A simple one-colour logo normally costs less than a full-coverage design with several Pantone colours. If the tray is used in a public-facing concession environment, printing quality is not merely decorative: inconsistent colour, blurred logos and misaligned artwork can undermine brand presentation.For Canadian chains, it can be efficient to use one standard structural tray with seasonal print changes. This can reduce tooling changes while allowing campaigns for hockey playoffs, film launches, music festivals or regional promotions. Buyers should ask whether print plates are reusable for repeat orders and how long the supplier retains approved artwork files.var ctx = document.getElementById('barChart').getContext('2d');new Chart(ctx, { type: 'bar', data: { labels: ['Stadiums', 'Cinemas', 'Quick Service', 'Food Trucks', 'Universities', 'Festivals'], datasets: [{ label: 'Relative Demand for Concession Trays in Canada', data: [92, 74, 88, 63, 69, 81], backgroundColor: [ 'rgba(166, 113, 48, 0.8)', 'rgba(74, 108, 74, 0.8)', 'rgba(204, 145, 72, 0.8)', 'rgba(111, 84, 61, 0.8)', 'rgba(91, 132, 141, 0.8)', 'rgba(185, 98, 81, 0.8)' ] }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Demand Index' } } } }});The demand comparison highlights why application-specific specifications matter. Stadium and quick-service users frequently require trays that dispense quickly and handle substantial volumes during short service windows. Food trucks may value carton compactness and low storage requirements, while universities may place stronger emphasis on sustainability statements, consistency and campus procurement standards.MOQ is especially important for custom-printed food trays. A manufacturer must set up printing, prepare materials, calibrate equipment, schedule production and pack the finished trays. These fixed activities are spread across the total number of trays produced. As order volume rises, the fixed cost per unit generally declines. The relationship is not linear forever, however; large orders can create additional storage, financing and shipping considerations.For a first Canadian import order, buyers often benefit from asking for multiple quantity scenarios. For example, a quotation can show pricing at 50,000, 100,000, 250,000 and 500,000 pieces. This reveals the threshold at which better unit pricing outweighs the carrying cost of extra inventory. For a distributor in Mississauga or Surrey, pallet storage and warehouse turnover may be more important than the lowest theoretical factory price.Order ScenarioTypical Unit Cost PatternSetup Cost AllocationInventory RiskBest FitSample orderHighest per pieceVery highLowTesting and approvalSmall custom runHighHighLow to moderateLaunches and local eventsMedium production runBalancedModerateModerateRegional distributorsLarge production runLowerLow per unitHigherMulti-site restaurant groupsFull-container planningPotentially lowest landed costLow per unitHigherHigh-volume importersScheduled release orderStable planning costShared over planned volumeControlledSeasonal or recurring usersMixed product consolidationImproved freight efficiencyDepends on product mixModerateDistributors needing varietyMOQ planning should include future repeat purchases. A buyer that expects quarterly replenishment may negotiate a scheduled order rather than placing isolated small runs. Fude Packaging supports planned production scheduling for customers who need continuity without holding all inventory at once. This is useful for concession distributors managing different tray sizes, kraft fries cups, bowls and meal packaging in the same program.Freight cube is often underestimated because kraft trays are light. Ocean and domestic transport charges are affected by volume as well as weight, and bulky carton packing can increase the landed cost substantially. Carton dimensions also influence pallet patterns, warehouse slots, loading efficiency and the number of cases that can move through a distribution network.Canadian import logistics may involve arrival through the Port of Vancouver, Port of Montréal, Port of Halifax or Prince Rupert, followed by rail or truck to regional warehouses. A tray shipment destined for Greater Toronto can have a different logistics profile from one serving British Columbia or Atlantic Canada. Buyers should request carton length, width, height, gross weight, net weight, pieces per carton and cubic metres per carton before comparing offers.var ctx = document.getElementById('areaChart').getContext('2d');new Chart(ctx, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Share of Buyers Prioritizing Compact Carton Packing (%)', data: [38, 45, 53, 61, 68, 74], borderColor: 'rgb(166, 113, 48)', backgroundColor: 'rgba(166, 113, 48, 0.28)', borderWidth: 3, fill: true, tension: 0.3 }] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Buyer Priority Share (%)' } } } }});The trend shift toward carton efficiency is likely to continue through 2026 and beyond. Rising warehouse costs, pressure on transportation budgets and the need for lower emissions per delivered unit make compact packing increasingly valuable. Buyers should not ask suppliers to compress trays so tightly that denesting becomes difficult, however. Proper packing must protect shape retention while preserving rapid separation at the service counter.A reliable quote comparison places every supplier on the same specification basis. One quotation may include a heavier grease-resistant board, export cartons and proofing, while another may only state a tray size and unit price. Without normalization, the lower quote may not represent equivalent quality or scope.Create a comparison sheet that includes physical dimensions, board GSM, coating type, print colours, sample option, carton count, carton cube, packing method, production lead time, payment terms, Incoterms and compliance documentation. For imported products, also clarify whether the price is EXW, FOB, CIF, DDP or another agreed term. Canadian buyers should coordinate with a customs broker or freight forwarder to understand duties, taxes, terminal charges and inland delivery before making a final decision.Quote Comparison ItemSupplier ASupplier BWhy It MattersTray dimensionsSpecify inside and outside sizeSpecify inside and outside sizePrevents capacity mismatchBoard weightGSM statedGSM statedSupports strength comparisonGrease resistanceTest method listedTest method listedReduces food-service failure riskPrinting scopeColours and coverage listedColours and coverage listedSeparates recurring and setup costPieces per cartonExact count shownExact count shownImproves receiving accuracyCarton cubic volumeCBM confirmedCBM confirmedSupports freight comparisonSample approvalWhite and printed optionsWhite and printed optionsControls quality before mass productionCompliance documentsAvailable on requestAvailable on requestSupports Canadian procurement reviewThe best normalized comparison uses a landed-cost measure such as cost per 1,000 usable trays delivered to the buyer’s warehouse. “Usable” matters because rejected trays, crushed cartons, print defects and inconsistent forming all reduce the number of saleable units. Set an acceptable defect threshold, document it in the purchase agreement and retain the approved sample as a reference record.A first-order budget should include both recurring and one-time expenses. Recurring expenses include trays, packing, freight, insurance, customs clearance, local delivery and warehouse handling. One-time expenses may include sampling, artwork adaptation, print plates, tooling changes, third-party inspection and laboratory testing. Not every project needs every item, but every item should be considered before approval.For a custom program, budget flexibility is important. Paper prices and international freight can change during the quotation period. A sensible purchasing plan includes a contingency allowance, particularly for seasonal event programs that cannot tolerate late delivery. If trays are required for Canada Day events, summer festivals or a fall sports season, production and shipping schedules should be planned backward from the in-warehouse date.Budget CategoryTypical First-Order StatusHow to Control ItCommon OversightTray unit priceRecurringCompare equivalent specificationsIgnoring board and coating differencesPrinting platesOne-time or periodicConfirm ownership and reuse termsAssuming they are includedSamplesOne-timeTest before production approvalSkipping functional evaluationOcean or air freightRecurringUse carton cube and route estimatesComparing factory price onlyCustoms and deliveryRecurringConfirm with freight partnerMissing local destination chargesWarehouse storageRecurringPlan order quantity and releasesBuying too much for unit-price savingsInspection and testingProject-dependentDefine acceptance plan earlyTesting only after complaints occurTo reduce cost without weakening performance, standardize tray sizes where possible, choose practical print coverage, order at sensible volume breaks, optimize carton dimensions, consolidate compatible packaging categories and approve materials through samples. Avoid reducing board weight or barrier treatment simply to lower price unless the application has been tested. A low-cost tray that fails with hot poutine can create waste, refunds and reputational damage that far exceed the original saving.Fude Packaging combines manufacturing scale with project-level customization for overseas B2B buyers. With more than 20 years of packaging experience and a self-owned 30,000 m² production base in Shandong, the company can manage paper selection, printing, die-cutting, forming, inspection, packing and export preparation within a controlled manufacturing system. Automated capacity of up to 120,000 units per day supports ongoing supply planning for distributors, food brands and multi-location operators.Technological capability is centred on controlled production and performance verification. In-house laboratory testing supports evaluation of key characteristics such as strength, grease resistance, leak prevention, print quality and batch consistency. Buyers can use digital proofs, white samples and printed pre-production proofs to verify tray dimensions, artwork, folding, colour appearance and real food performance before full production begins.Manufacturing capability also means practical product consolidation. In addition to tray programs, Fude Packaging supplies cups, bowls, boxes and multi-compartment meal packaging. This can help Canadian distributors reduce supplier fragmentation, align branding across categories and improve container utilization. Learn more about the company’s production approach on the Fude Packaging company profile.Service capability is designed for international procurement. The team supports OEM and ODM projects, artwork review, Pantone matching, functional sampling, export carton planning, inspection coordination and shipping documentation. Food-contact and quality documentation may include FSC, ISO 9001, FDA-related food-contact support and other applicable records depending on material and destination requirements. Buyers can review available custom packaging and export services when building a Canada-focused supply program.var ctx = document.getElementById('comparisonChart').getContext('2d');new Chart(ctx, { type: 'bar', data: { labels: ['Material Control', 'Custom Printing', 'Sample Approval', 'Carton Optimization', 'Export Support', 'Traceability'], datasets: [ { label: 'Structured Manufacturing Program', data: [92, 88, 95, 84, 90, 91], backgroundColor: 'rgba(74, 108, 74, 0.8)' }, { label: 'Basic Unit-Price Purchase Model', data: [58, 52, 45, 49, 54, 47], backgroundColor: 'rgba(166, 113, 48, 0.75)' } ] }, options: { responsive: false, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Capability Index' } } } }});The comparison illustrates the difference between buying trays solely as a commodity and managing them as a food-service packaging program. The latter emphasizes repeatability, documented approval, dependable delivery and reduced operational risk. For a national customer, consistency between shipments can be just as important as a competitive initial quote.In 2026, Canadian buyers are likely to place greater emphasis on fibre sourcing, material transparency, reduced plastic content, compostability claims, efficient transportation and lifecycle considerations. Sustainability communication should be specific and documented. Buyers should not make broad environmental claims without verifying the actual material construction, local recovery pathways and relevant certification scope.Technology will also influence packaging procurement. Digital proofing, traceability records, barcode-enabled batch management and more efficient production planning will help buyers control brand consistency across multiple locations. Automated forming and inspection can improve repeatability, while design optimization can reduce fibre usage without compromising practical strength.Policy and procurement standards may continue to encourage lower-impact food-service packaging, particularly among universities, municipalities, major venues and national brands. The strongest approach is to select a tray that meets real operational requirements first, then match its material and documentation to the customer’s sustainability objectives and applicable Canadian market expectations.1. What is the usual cost structure for fast-service kraft concession trays?Typical costs include paperboard, coating, forming, printing, packing, quality control and freight. For custom projects, add samples, printing plates, artwork work and possible tooling costs. The most meaningful measure is landed cost per 1,000 usable trays.2. Which specification changes affect price most?Paper GSM, grease-resistant treatment, tray size, structural complexity, printing coverage, carton packing and order quantity are usually the largest drivers. A deeper tray or a high-coverage multi-colour print can affect pricing more than a minor dimensional change.3. How does MOQ change the unit price?MOQ spreads setup costs across more units. Small custom orders often have a higher price per tray because production preparation is divided among fewer pieces. Ask for tiered quotations to identify the best balance between unit cost and inventory exposure.4. Which quote items are commonly excluded?Common exclusions include print plates, samples, third-party inspection, ocean freight, customs clearance, local delivery, taxes, storage and destination charges. Always confirm the Incoterm and request carton specifications before comparing suppliers.5. How can Canadian buyers reduce cost without weakening tray performance?Standardize sizes, select suitable rather than excessive board weight, use practical print coverage, optimize carton density, consolidate related packaging items and plan replenishment schedules. Maintain sample testing for denesting, grease resistance, lap stability and food-contact performance.6. What should be included in a tray approval record?The record should include approved artwork, dieline, dimensions, board specification, coating requirement, colour standard, carton pack count, sample photos, test results, acceptance criteria, inspection method and production batch reference. This creates a repeatable quality baseline for future orders. -

Global Market Corporate Catering Packaging Playbook 2026
A successful food packaging program for corporate catering in the Global market is built around a clear principle: standardize what affects food safety, operating speed, purchasing control, brand consistency, and replenishment reliability, while allowing limited, documented flexibility for local menus and site conditions. Corporate catering teams often serve different office locations, campuses, hospitals, event venues, airports, and production facilities, yet they must deliver a consistent guest experience every day.The core packaging specification should define container format, material grade, capacity, coating or barrier requirement, lid fit, branding zone, label position, case quantity, pallet configuration, approved suppliers, and reorder trigger. Local teams should not independently substitute packaging simply because a nearby distributor has stock. Instead, they should choose only from an approved SKU list, supported by a controlled exception process for climate, menu, delivery distance, local regulation, or customer-specific requirements.For most B2B buyers, the most practical operating model is a core-and-flex range. The core range covers the highest-volume applications: hot meal boxes, salad bowls, soup containers, beverage cups, dessert cups, sandwich packs, trays, lids, cutlery kits, and tamper-evident labels. The flex range covers site-specific needs, such as larger portions for factory canteens, premium presentation for executive meetings, insulated packs for outdoor events, or certified compostable formats for locations with organics collection.Packaging should be tested with real menu items before rollout. This means filling containers at normal serving temperatures, closing them with the approved lid, stacking them in realistic delivery bags, holding them for the expected transit period, and checking leakage, grease strike-through, condensation, deformation, label adhesion, and customer presentation. A specification that appears correct on paper may fail when filled with curry, oily noodles, hot soup, dressed salads, or sauces.In practice, the best corporate catering packaging programs are measurable. Procurement can see approved price bands and minimum order quantities; operations can reorder without guessing; quality teams can audit lots and documents; site managers can receive the correct packaging before peak service; and brand teams can maintain a coherent visual identity from London and Dubai to Singapore, Los Angeles, Rotterdam, Sydney, and Johannesburg.Control AreaWhat Should Be StandardizedAllowed Local VariationOwnerReview FrequencyFood contact materialsApproved paperboard, coating, inks, food-contact documentationDestination-market compliance documentsQuality and procurementAnnual or regulation changeContainer dimensionsCore capacities, lid interfaces, stacking footprintOne approved premium or large-size optionOperationsQuarterlyBrandingLogo placement, color targets, artwork approval processLocal language campaign messageBrand teamPer artwork revisionLabelingAllergen field, production date field, label locationLocal legal language and dietary iconsFood safety teamPer marketCase packCase count, carton markings, barcode structureOuter carton languageSupply chainAnnualReorderingSafety-stock rule, approved SKU codes, reorder pointSite consumption forecastSite managerWeeklyThis matrix prevents a common corporate catering problem: a centrally negotiated package is approved, but individual kitchens order visually similar alternatives with different lids, inconsistent print colors, unsuitable heat resistance, or unplanned case quantities. Standardization is not about removing all choice; it is about making the approved choice simple and operationally dependable.Start with a menu and site map before selecting containers. Corporate catering demand is not uniform. A financial-services office in Canary Wharf may require polished executive lunch packaging, while a manufacturing site in São Paulo may need high-volume, durable meal trays for staggered shifts. A technology campus in Bengaluru may serve vegetarian curries and rice bowls at scale, while a conference venue in Frankfurt may require compact, branded grab-and-go packs that fit service counters and transport trolleys.Map every location by meal type, service style, daily cover count, food temperature, delivery radius, storage space, waste stream, and receiving schedule. The map should also record local procurement restrictions and destination regulations. For international programs, shipping routes matter. Packaging entering Europe through Rotterdam or Hamburg, the Middle East through Jebel Ali, North America through Los Angeles or New York/New Jersey, and Southeast Asia through Singapore may require different lead-time buffers and document handling.Site ProfileTypical MenuRecommended Pack FormatKey Performance NeedPlanning PriorityCity office cateringSalads, sandwiches, hot bowlsSalad bowls, hinged lunch boxes, sandwich packsBrand presentation and stackabilityFast lunch peakIndustrial canteenRice meals, stews, protein mealsCompartment trays and large meal boxesStrength and portion separationHigh daily volumeExecutive boardroomPremium plated-style mealsRigid kraft boxes, clear-lid trays, dessert cupsPremium appearanceLow defect toleranceHospital or healthcare siteDiet-specific meals, soupsLabel-ready trays, sealed bowls, soup cupsTraceability and leakage preventionClear identificationUniversity campusNoodles, snacks, beveragesNoodle boxes, cups, food traysSpeed and valueVariable demandEvent and convention venueBoxed lunches, canapés, beveragesLunch boxes, catering trays, drink carriersTransport resilienceShort peak windowsThe site map should lead to a menu-to-pack matrix. For example, dry sandwiches may perform well in a standard kraft clamshell, but dressed salads may require a coated bowl with a secure lid. Hot curries may need a more robust bowl and lid system than cold pasta salads. A box intended for a 20-minute internal office handoff may not survive a 75-minute external delivery through summer heat in Dubai or rain in Manchester.Demand data should be separated into predictable catering orders, recurring workplace meal programs, promotional events, seasonal peaks, and emergency replenishment. This makes it easier to decide which items belong in local stock, which can be held centrally, and which should be made to order.(function(){var ctx=document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctx,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Illustrative corporate catering packaging demand index',data:[100,108,117,126,137,149],borderColor:'rgb(33,112,165)',backgroundColor:'rgba(33,112,165,0.12)',borderWidth:3,fill:false,tension:0.3}]},options:{responsive:true,maintainAspectRatio:false,scales:{y:{beginAtZero:false,title:{display:true,text:'Demand index (2022 = 100)'}},x:{title:{display:true,text:'Year'}}}}});})();The chart shows an illustrative planning index rather than a universal market forecast. Buyers can use a similar index based on their own order history, new-site pipeline, menu expansion, and seasonal event calendar. The important point is to forecast packaging demand separately from food sales, because packaging usage can change when portion sizes, menu formats, delivery patterns, or sustainability policies change.A core SKU standard reduces complexity without creating food-service bottlenecks. Most multi-site programs can begin with 12 to 20 primary packaging SKUs, then add controlled accessories. The goal is not to force every menu into one box. It is to create a small approved system where containers, lids, labels, and transport trays work together.A practical core range may include paper cups for hot and cold beverages, paper bowls for soup and grain bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, food trays, multi-compartment meal boxes, lids, cup carriers, napkins, and labels. Buyers sourcing multiple formats can review Fude Packaging’s food container range for corporate catering when building an initial approved list.Core SKUTypical Capacity or SizeBest UseRequired TestStandardization RuleSingle-compartment lunch box700–1,000 mlHot meals and mixed bowlsHeat, grease, compressionOne primary footprintTwo-compartment meal box800–1,200 mlMain meal plus sidePartition integrityOne lid closure systemFive-compartment catering trayLarge shared formatBuffets and group mealsLoad and stacking testApproved for event sitesSalad bowl with lid500–1,000 mlCold salads and grain bowlsLid fit and condensationTwo standard capacitiesNoodle box500–750 mlNoodles and stir-fryLeakage and steam holdOne folding structureSoup cup and lid350–700 mlSoup, sauces, porridgeHot liquid leakageMatched lid onlyHot beverage cup250–450 mlCoffee and teaInsulation and rim curlCommon lid diameterEach SKU should have a specification sheet that includes internal dimensions, nominal capacity, material construction, coating type, weight tolerance, approved print areas, lid code, packing configuration, pallet arrangement, storage conditions, and quality acceptance criteria. Photographs alone are not sufficient. Procurement teams need technical identifiers that distinguish, for example, a 750 ml salad bowl from a visually similar bowl with a different rim diameter.For high-volume meal programs, compartment trays are valuable because they keep components separate and support portion control. Buyers planning workplace meals or large meetings can evaluate a five-compartment catering tray option where menu composition and transport stability require clear separation.Food performance testing should reproduce the actual service chain, not just laboratory conditions. A container may pass a simple water-hold test but fail after being filled with oily food, stacked under other meals, transported in a thermal bag, and opened by a customer after 45 minutes. Test protocols should be written in measurable terms so different sites can compare results.For hot foods, measure leakage after filling, lid displacement during transport, bottom softness, sidewall deformation, and heat transfer to the customer’s hands. For cold food, assess condensation, lid fogging, loss of crispness, and label adhesion. For foods with oil or sauce, inspect exterior grease migration and corner leakage. For beverages, test rim integrity, lid compatibility, and resistance to squeezing during movement.Test ScenarioMethodSuggested ConditionPass CriterionOperational ValueHot meal holdFill with normal hot menu item60 minutes at service temperatureNo leakage or major deformationProtects delivery qualityGrease resistanceFill with oily or fried food45 minutes in closed packNo visible strike-throughMaintains hand feelSoup leak testFill, close, tilt and invertHot liquid, 30 minutesNo drip from lid or seamReduces claimsStack compressionStack filled packsThree to five layersLower packs remain stableSupports dispatchTransport vibrationPlace in delivery crate or trolley15–30 minute route simulationClosure remains secureTests real movementLabel adhesionApply operational labelCold, warm, and humid surfacesReadable label remains attachedSupports traceabilityDocument results by SKU, food type, temperature, fill weight, holding time, and failure mode. Do not approve a container merely because it worked for one dry menu item. A proper approval pack includes photos, completed test forms, sample batch details, and a signed decision from operations, food safety, procurement, and brand representatives.Testing should also cover pack opening. Corporate catering guests may eat at desks, on commuter trains, in meeting rooms, or outdoors. Packs should open intuitively without tearing, spilling, or requiring tools. If tamper evidence is used, the feature must be visible but not frustrating to remove.Corporate catering packaging is a mobile brand asset. It travels through office reception areas, conference halls, elevators, client meetings, delivery vehicles, and shared dining spaces. A controlled brand system protects visual recognition while leaving room for local language, dietary information, recycling guidance, and customer-specific event details.Create one master artwork guide. It should define logo size, safe areas, approved color values, ink coverage limits, print position, barcode location, lot-code field, label zones, and prohibited alterations. For food-contact packaging, printing choices should also account for ink suitability, rubbing resistance, and production tolerances. Brand teams should approve artwork before samples are printed, not after cartons are already in production.Labels deserve the same discipline as printing. A label template can include dish name, allergen information, dietary code, preparation date, use-by time, site code, order number, customer name, and reheating guidance where relevant. Local requirements may differ, but the data structure should stay consistent. That supports digital ordering systems, incident investigation, and operational audits.(function(){var ctx=document.getElementById('industryDemandChart').getContext('2d');new Chart(ctx,{type:'bar',data:{labels:['Office campuses','Healthcare','Universities','Events','Industrial sites','Airports'],datasets:[{label:'Illustrative packaging demand intensity',data:[88,72,81,76,85,68],backgroundColor:['#1f77b4','#2ca02c','#ff7f0e','#9467bd','#d62728','#17becf']}]},options:{responsive:true,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:100,title:{display:true,text:'Demand intensity score'}}}}});})();This comparison helps buyers prioritize specification depth. Office campuses and industrial sites often need robust replenishment and large-volume pack formats. Healthcare locations need stronger labeling control. Universities may require economical, fast-service formats. Event venues often value transport-ready trays and highly visible branding.Minimum order quantity and contract pricing should be designed around total program economics, not only the lowest piece price. A custom-printed package usually has higher setup requirements than an unprinted stock item because artwork approval, printing plates, color matching, and production scheduling are involved. However, consolidating volumes across multiple sites can often improve pricing, reduce color variation, and simplify replenishment.Use a tiered contract structure: a standard price for core SKUs, volume breaks based on annual consolidated demand, separate terms for custom print, agreed material-change notification rules, and a clear treatment of freight, duties, sampling, and urgent orders. For Global market programs, buyers should also specify whether pricing is factory basis, FOB port, CIF destination, or delivered warehouse basis. Ports such as Qingdao, Shanghai, Ningbo, Rotterdam, Jebel Ali, and Los Angeles can materially affect landed-cost planning.Commercial ElementRecommended Contract RuleBuyer BenefitSupplier ObligationRisk if UndefinedCore SKU pricingFixed period with review formulaBudget visibilityMaintain quoted specificationUnexpected increasesCustom print MOQSet by format and print complexityRealistic ordering planConfirm before artwork releaseExcess inventoryAnnual volume tierAggregate approved site demandBetter total costApply earned price tierLost buying powerFreight termNamed Incoterm and portClear landed-cost modelProvide export-ready documentsFreight disputesMaterial substitutionWritten approval requiredProtects performanceNotify before changeUncontrolled quality changeUrgent replenishmentDefined lead time and surchargeEmergency optionState capacity limitsService interruptionWhen comparing quotations, ask for the full technical and commercial basis: unit size, board weight, coating, printing method, pieces per carton, cartons per pallet, gross weight, cubic volume, lead time, certification availability, and defect-handling process. A lower unit price can become more expensive if cartons contain fewer usable pieces, pallets load inefficiently, or the pack fails during service.For custom meal presentations, a buyer may consider custom printed two-compartment takeaway boxes to separate main dishes from sides while preserving a consistent brand experience across catered events.Central and local inventory should work as one system. Central stock is best for common, high-volume core SKUs and printed items with longer replenishment lead times. Local stock is best for fast-moving items required for daily operations, site-specific menu formats, and emergency coverage. The correct balance depends on demand volatility, warehouse space, supplier lead time, import route, and the cost of a stockout.Set a reorder point for every SKU using average weekly usage, expected lead time, safety stock, and known demand events. For example, a conference venue with a major quarterly event should not rely solely on average daily consumption. Its event forecast must be added before the order trigger is calculated.Inventory CategoryStock LocationTypical CoverageReorder TriggerControl MethodHigh-volume meal boxesCentral warehouse plus local buffer4–8 weeksForecast demand during lead time plus safety stockWeekly dashboardPrinted cupsCentral warehouse6–12 weeksArtwork-specific minimum balanceMonthly reviewSoup cups and lidsLocal site stock2–4 weeksMatched cup-and-lid balanceWeekly countEvent catering traysRegional hubEvent calendar basedConfirmed event order plus bufferEvent planner sign-offLabels and sealsLocal site stock2–6 weeksPackaging usage ratioDaily visual checkContingency plain packsCentral reserve2–3 weeksReleased only during disruptionProcurement approvalUse matched inventory logic. A site does not truly have 10,000 usable soup packs if it has 10,000 cups but only 3,000 compatible lids. The same rule applies to meal boxes and tamper labels, trays and sleeves, or cups and carriers. A simple ERP system, spreadsheet dashboard, or supplier-managed report can flag these mismatches before service is affected.For imported packaging, include ocean transit, port clearance, inland delivery, customs documentation, and seasonal congestion in lead-time assumptions. A replenishment schedule that works during normal conditions may fail during peak shipping periods or weather disruption. Maintain approved contingency SKUs that preserve food safety and functionality even if branded stock is temporarily unavailable.(function(){var ctx=document.getElementById('trendShiftChart').getContext('2d');new Chart(ctx,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Standardized core SKU share',data:[48,54,61,67,73,78],borderColor:'#2e8b57',backgroundColor:'rgba(46,139,87,0.22)',fill:true,tension:0.3},{label:'Uncontrolled local SKU share',data:[52,46,39,33,27,22],borderColor:'#c85a54',backgroundColor:'rgba(200,90,84,0.10)',fill:true,tension:0.3}]},options:{responsive:true,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:100,title:{display:true,text:'Share of packaging spend (%)'}}}}});})();The area chart illustrates the intended direction of a mature program: a growing share of spend is assigned to approved core formats, while uncontrolled local variation declines. This typically improves forecast accuracy, purchasing leverage, quality consistency, and training efficiency.A supplier service-level agreement should turn expectations into measurable commitments. Packaging availability is a food-service continuity issue, not merely a procurement matter. The SLA should define order confirmation time, sampling milestones, production lead time, shipment documentation, quality acceptance standard, corrective-action timing, and escalation contacts.For international sourcing, the SLA must also describe export documentation, carton marking, pallet standards, loading controls, inspection access, and communication during shipment. A supplier should provide early warnings if raw-material availability, production capacity, artwork approval, port congestion, or regulatory documentation could affect the agreed schedule.SLA KPITarget StandardMeasurement MethodWhy It MattersCorrective ActionOrder acknowledgementWithin 1 business dayTimestamped confirmationProtects planning speedEscalate to account leadOn-time production95% or higherReady-date versus confirmed dateSupports replenishmentRecovery plan requiredOrder accuracy99% or higherSKU and quantity verificationAvoids operational mismatchReplacement or credit processQuality acceptanceAgreed AQL or specification levelPre-shipment inspectionControls defectsRoot-cause reportDocument completeness100% before shipmentChecklist reviewSupports customs clearanceDocument escalationClaim responseInitial response within 48 hoursCase logLimits service disruptionCAPA and resolution timelineA good SLA includes agreed quality definitions. Terms such as “acceptable print quality” or “good lid fit” are too vague. Define measurable samples, approved artwork, acceptable color tolerance where relevant, seam condition, dimensions, pack count, carton integrity, and food-performance requirements. Retain a signed golden sample for each custom SKU.Fude Packaging supports corporate catering buyers that need consistent paper-based food packaging across multiple locations and destination markets. Our approach is built around scalable standardization: selecting core formats, confirming functional requirements, developing custom visual identity where needed, and supporting repeat replenishment without losing control of the specification.With more than 20 years of packaging experience, Fude Packaging uses in-house product development and laboratory testing to assess practical performance before mass production. Our technical team can support material and coating recommendations, structural development, custom sizing, artwork and dieline review, Pantone color matching, prototype development, and functional evaluation. Samples can be prepared as plain white samples, printed samples, or application-focused prototypes so buyers can verify capacity, dimensions, heat resistance, grease resistance, leakage prevention, lid fit, and print quality with their own foods.For Global market customers, documentation requirements are considered early in the project. Depending on the destination and product specification, our team can help align packaging programs with relevant food-contact, FSC, ISO 9001, compostability, and market documentation expectations. The correct material solution depends on the food, end-of-life route, local collection infrastructure, transit time, and buyer sustainability target.Fude Packaging operates a self-owned 30,000 m² factory in Shandong, China, within an established paper and packaging supply region. Advanced automated lines support production capacity of up to 120,000 units per day, with control over material selection, printing, die-cutting, forming, inspection, packing, and shipment preparation. In-house manufacturing helps corporate catering buyers consolidate packaging categories under one supplier and maintain consistency across paper cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, trays, and compartment meal boxes.Incoming-material inspection, production monitoring, laboratory testing, final inspection, and batch verification are used to support stable quality. Buyers may also appoint third-party inspection companies or laboratories before shipment. This is useful for programs serving multiple countries where quality records and shipping documentation must be shared with central procurement teams.Our multilingual export team works with importers, distributors, restaurant groups, caterers, takeaway platforms, retailers, and food brands in more than 50 countries. We clarify food type, serving temperature, capacity, forecast volume, branding requirements, destination regulations, delivery deadline, and preferred shipping mode before recommending a solution. Standard production orders can generally be completed in approximately 7–15 days, depending on specification and volume.Fude Packaging supports T/T and L/C payment methods as well as sea freight, air freight, full-container, less-than-container, and express sample shipments. We can assist with commercial invoices, packing lists, certificates, inspection documents, and other export paperwork. After shipment, confirmed manufacturing or quantity concerns are handled through defined quality assurance, replacement, return, and claim procedures. This service model helps corporate catering teams reduce risks from fragmented sourcing, print inconsistency, leakage complaints, incomplete documents, and unpredictable replenishment.(function(){var ctx=document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctx,{type:'bar',data:{labels:['SKU consolidation','Customization','Quality control','Export support','Replenishment planning','Food testing'],datasets:[{label:'Integrated manufacturer model',data:[92,90,91,88,86,89],backgroundColor:'#5b7cfa'},{label:'Fragmented multi-supplier model',data:[55,62,58,49,53,52],backgroundColor:'#b9c3d3'}]},options:{responsive:true,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:100,title:{display:true,text:'Illustrative capability score'}}}}});})();The comparison chart is an operational planning illustration. It highlights why an integrated manufacturing partner can be valuable when a corporate catering program requires multiple product formats, consistent print control, technical testing, export documentation, and coordinated replenishment rather than a one-time purchase of a single container.Standardize the core specification: food-contact material, container size, lid interface, performance requirement, artwork rules, label location, case pack, SKU code, and reorder logic. Build an approved core range for the most common menus, then require local sites to choose from that range. Use a formal exception process for menu-specific or regulation-specific needs so the central team retains visibility.Allow controlled variation for local menu style, serving temperature, delivery time, portion size, local language, allergen requirements, waste-stream rules, climate, and customer-facing event presentation. For example, an outdoor catering operation in a hot climate may require stronger cold-drink condensation control, while a hospital site may need more detailed meal identification labels. Variation should be approved, coded, and forecasted rather than purchased informally.Test with actual food and actual service conditions. Fill the pack at normal temperature, apply the approved lid and label, hold it for the expected time, stack it, transport it in the normal crate or bag, and inspect leakage, grease migration, deformation, temperature impact, closure security, and presentation. Test multiple menu types, particularly soups, sauces, fried foods, salads with dressing, and hot rice meals. Retain documented results and approved samples.Keep high-volume, common, longer-lead-time, and custom-printed SKUs centrally, with local buffers for daily service. Hold site-specific and urgent-use items closer to the point of consumption. Calculate reorder points from average demand, lead time, safety stock, seasonal events, and known customer bookings. Track matched components such as bowls and lids together. Maintain a controlled contingency stock of approved plain packaging for disruption recovery.Track approved-SKU adoption rate, stockout frequency, packaging waste percentage, on-time supplier delivery, order accuracy, customer complaints per thousand meals, leakage incidents, packaging cost per meal, emergency freight spend, inventory turns, artwork error rate, and local exception volume. A healthy program generally shows fewer unapproved purchases, lower emergency orders, more reliable availability, stable food presentation, and clearer traceability across sites.In 2026, corporate catering packaging programs will increasingly combine sustainability, digital control, and operational resilience. Buyers are expected to use more QR-enabled traceability, digital artwork approvals, consumption forecasting, packaging-to-menu analytics, and supplier performance dashboards. Sustainability requirements will continue shifting from broad claims toward evidence-based decisions: material sourcing, food-contact safety, recyclability or compostability conditions, local collection infrastructure, and practical reduction of unnecessary material.Policy changes will remain market-specific. A pack that is suitable for one region may need different documentation, labeling, or recovery guidance in another. Global buyers should avoid assuming that one environmental claim works everywhere. The stronger strategy is to define the intended use, local disposal route, regulatory needs, and brand objective for each market, then select a packaging structure supported by documentation and real-world performance testing.For corporate caterers, the future is not simply “more sustainable packaging.” It is better-controlled packaging: fewer unnecessary SKUs, better food protection, accurate labels, efficient case packs, predictable replenishment, documented compliance, and a supply partner capable of supporting growth across markets.