Global Market Guide to Paperboard Caliper and GSM Control
Quick Answer — How to Evaluate Paperboard Caliper and GSM Packaging Reliably

A reliable paperboard caliper and GSM packaging evaluation requires more than checking a supplier’s material declaration. Global market buyers should use a repeatable method covering controlled samples, board grade, coating type, food or simulant, contact temperature, holding duration, stacking load, humidity exposure, and measurable pass/fail limits. The final result should be written into the approved product specification, purchase order, supplier quality agreement, and incoming inspection plan.
GSM measures the mass of paperboard per square metre. Caliper measures the thickness of the material, usually in microns or millimetres. Neither value alone guarantees container strength. A higher-GSM board can be compressed and have a lower caliper, while a lower-GSM board with bulkier fibre structure can show more thickness but not necessarily better wet strength, stiffness, or crease durability. Coating, fibre composition, converting method, fold geometry, and food conditions also influence performance.
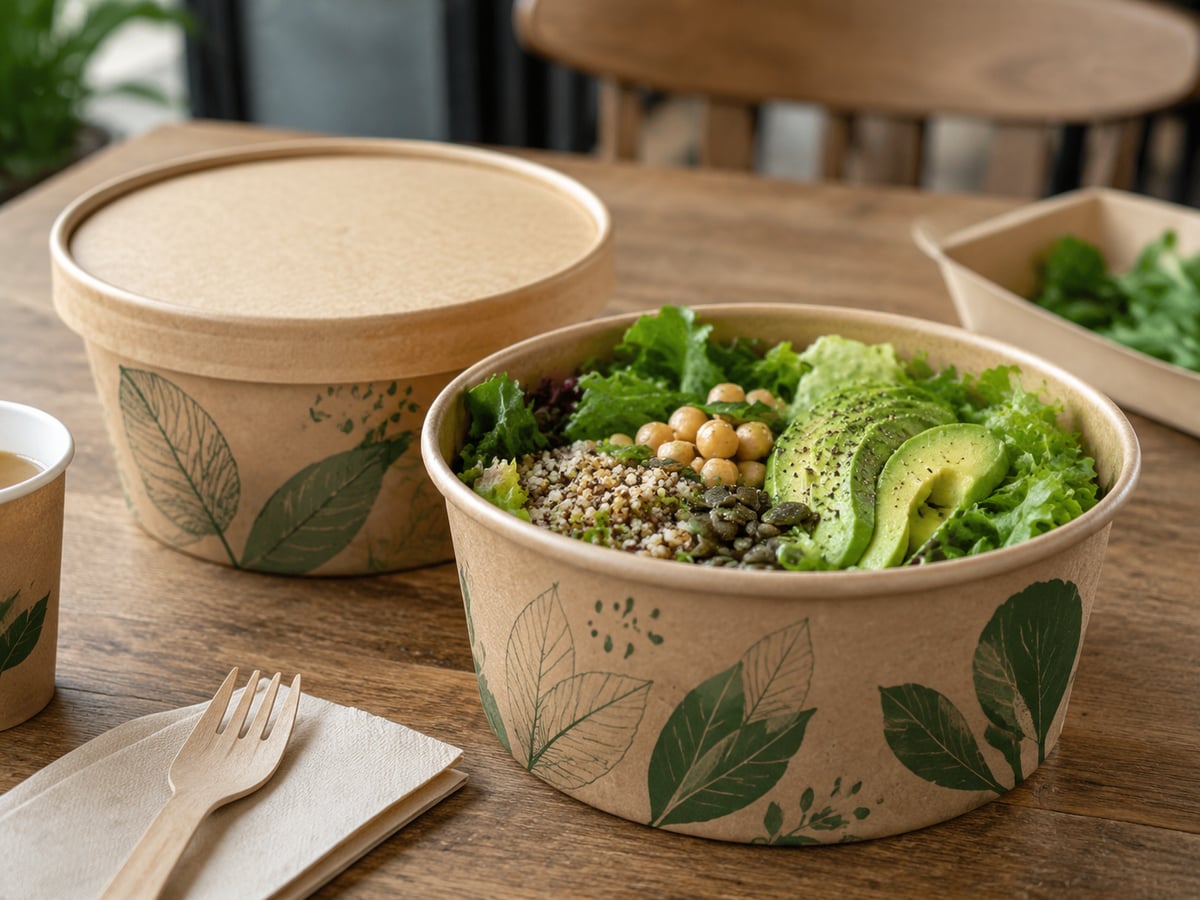
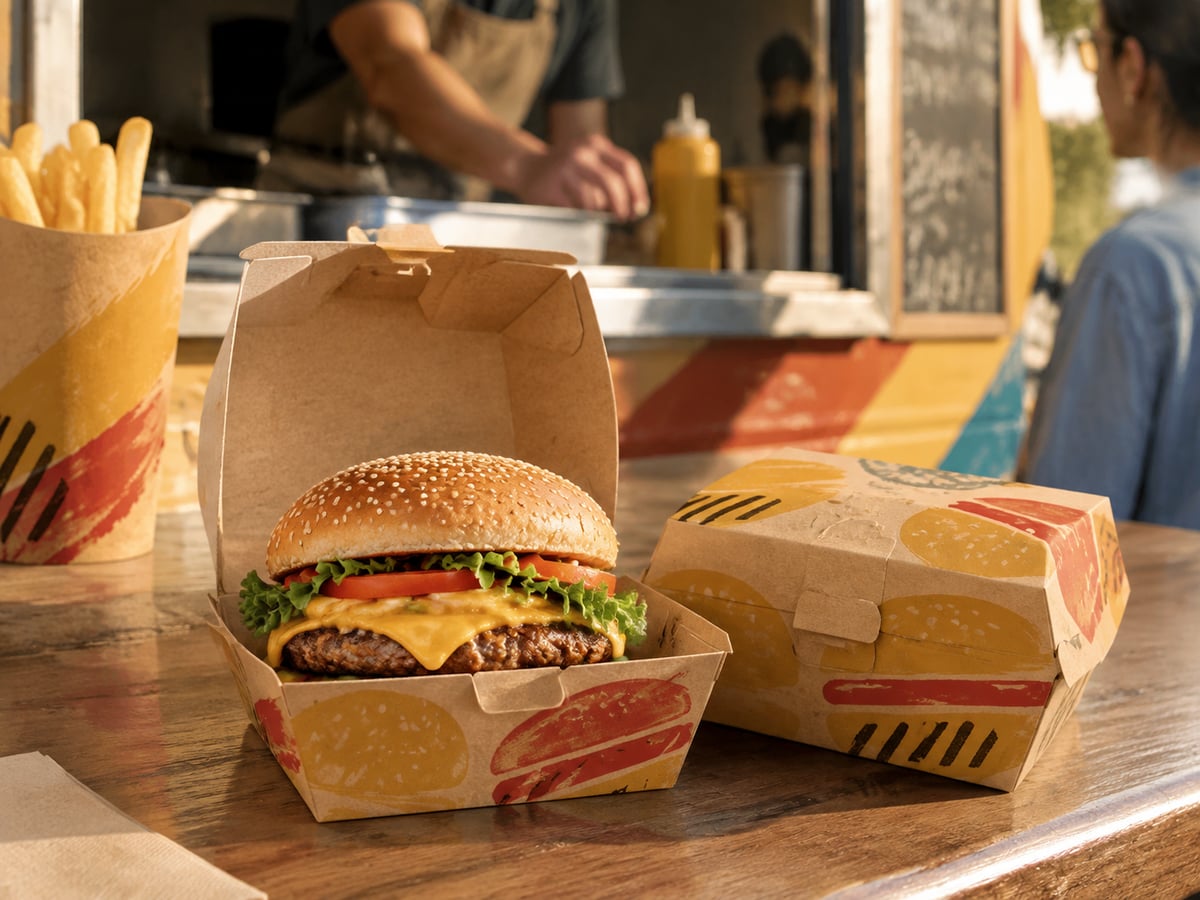
For food packaging, buyers should connect caliper and GSM to the actual failure mode. For example, a hot soup bowl needs rim stiffness, sidewall integrity, bottom bonding, and resistance to heat and moisture. A burger box needs stack compression, grease resistance, hinge performance, and print-scuff resistance. A kraft lunch box needs good fold retention, secure closure, and resistance to sauce migration. Testing should therefore simulate the actual foodservice application rather than relying on a paper specification alone.
A practical approval sequence is: define the product application; agree the target GSM and caliper range; condition specimens; measure material consistently; run functional trials using food or appropriate simulants; document results; approve a golden sample; and verify every incoming lot against the agreed control plan. This approach gives procurement teams an objective basis for comparing suppliers in Shanghai, Qingdao, Ningbo, Rotterdam, Los Angeles, Dubai, Singapore, and other global trade hubs.
| Measure | What It Indicates | Typical Unit | Buyer Benefit | Key Limitation |
|---|---|---|---|---|
| GSM | Mass per square metre | g/m² | Supports material-cost and board-grade control | Does not directly prove thickness or stiffness |
| Caliper | Thickness under defined test pressure | µm or mm | Helps assess bulk, rigidity, and forming fit | Can vary with moisture and compression history |
| Bulk | Thickness relative to board mass | cm³/g | Shows whether board has an open or dense structure | Must be interpreted with strength data |
| Stiffness | Resistance to bending | mN or equivalent | Relates to container shape retention | Depends on grain direction and structure |
| Wet strength | Strength retained after moisture exposure | Percentage or test result | Relevant for hot, wet, and chilled foods | Not determined by GSM alone |
| Compression resistance | Ability to tolerate stacking load | N or kgf | Reduces collapse during delivery and warehousing | Depends on final pack geometry |
The table shows why procurement teams should not specify “400 GSM” without also identifying a caliper target, acceptable tolerance, coating system, board grade, and functional performance requirements. A meaningful specification combines material measurements with the real use case.
Caliper vs GSM: Buyer Risk

The principal buyer risk is assuming that GSM and caliper are interchangeable. They are related but independent enough to create quality gaps when a supplier changes pulp mix, board source, coating weight, moisture level, or calendering pressure. A board may meet the purchased GSM value but be thinner than the approved material. This can lead to weaker sidewalls, poor lid engagement, lower stack strength, distorted printing registration, or insufficient thermal insulation.
In takeaway packaging, a caliper drop may increase the risk of softening when the package holds fried food, curry, noodles, soup, salad dressing, or refrigerated prepared meals. For distributors, the issue can remain hidden until the products reach a restaurant or delivery platform. By that point, freight, relabelling, replacement, and brand-damage costs can exceed the saving generated by a lower-cost board.
Buyers should assess risk by product category. Cups and bowls are highly sensitive to wall stiffness, bottom curl quality, sealing performance, and lid compatibility. Burger boxes and clamshells are sensitive to crease cracking, closure retention, compression strength, and grease exposure. Rectangular lunch boxes need reliable corners, sidewall squareness, and load capacity. Flat food trays are more vulnerable to sagging and edge deformation during handling.
| Packaging Application | Likely Failure | Caliper/GSM Contribution | Operational Consequence | Recommended Control |
|---|---|---|---|---|
| Hot soup bowl | Sidewall softening | Thin board or inadequate wet-strength system | Leakage, difficult handling, customer complaints | Hot-fill and hold test with load |
| Paper cup | Rim deformation | Low caliper reduces curl stability | Poor lid fit and spill risk | Rim, lid-fit, and top-load checks |
| Burger box | Collapsed lid or base | Low stiffness despite nominal GSM compliance | Food presentation damage during delivery | Compression and stack simulation |
| Kraft lunch box | Corner opening | Board too thin at score lines | Sauce leakage and weak closure | Fold-cycle and filled-pack testing |
| Salad container | Panel bowing | Low caliper after chilled moisture exposure | Unstable stacking and lid mismatch | Cold-hold humidity trial |
| Noodle box | Bottom distortion | Material loses rigidity under heat and moisture | Handling failure and reduced safety perception | Heat, time, and carry-load test |
For global sourcing, risk also varies by logistics route. Containers shipped from Qingdao or Ningbo may experience extended humidity changes before discharge at Hamburg, Jebel Ali, Sydney, or Long Beach. Packaging should be protected by suitable outer cartons, palletisation, moisture control where appropriate, and pre-shipment verification. Material readings must be measured on conditioned samples; otherwise, a temporary moisture difference may be mistaken for a permanent board-quality difference.
This indicative market-growth trend reflects stronger demand for documented material consistency, recyclable fibre-based formats, and food-contact compliance. It is not a substitute for a buyer’s own forecast, but it highlights why structured board controls are becoming more important in international procurement.
Caliper vs GSM: Sample Size

Sample size should reflect both the risk of the product and the variability of the lot. A single specimen is never sufficient because board thickness can vary across a sheet, roll, print run, and die-cut position. For initial qualification, buyers should test samples from multiple production positions, including early, middle, and late production. For routine incoming inspection, samples should be selected randomly from different cartons and pallet locations.
For board measurements, a common practical method is to take at least ten specimens per lot or production batch, avoiding creases, print-heavy areas, embossed regions, seams, and visibly damaged sections. For critical products such as soup bowls, heavy meal boxes, large cups, or multi-compartment trays, use larger sampling plans and include complete formed packs in addition to flat-board measurements. Every test record should identify lot number, production date, paperboard source, coating designation, operator, instrument, and conditioning status.
| Control Stage | Material or Product | Minimum Sample Approach | Sampling Locations | Main Purpose |
|---|---|---|---|---|
| New supplier qualification | Flat board and formed pack | 30 board specimens plus 20 finished packs | Across multiple production times | Establish baseline capability |
| First production order | Finished packaging | 20 to 32 finished packs | At least 5 cartons | Confirm approved specification |
| Routine incoming lot | Finished packaging | 13 to 20 packs, risk based | Top, middle, bottom pallet levels | Detect shipment variation |
| High-risk hot-food item | Bowls, cups, meal boxes | 20 packs plus functional trials | Multiple cartons and forming positions | Verify wet and heat performance |
| Complaint investigation | Retained and returned samples | All available evidence plus fresh lot samples | Complaint and reference batches | Identify root cause |
| Annual requalification | Approved product range | Full material and function review | Representative SKUs | Confirm continuing suitability |
The sample plan should be adjusted for lot size, historical conformity, product criticality, and customer exposure. A premium coffee chain operating in London, Toronto, Seoul, or Melbourne may require tighter controls than a low-risk dry-food tray. However, no buyer should reduce verification to a visual check when board properties are central to product performance.
Caliper vs GSM: Test Equipment
Reliable results require calibrated equipment and a consistent method. GSM is commonly measured by cutting a defined specimen area and weighing it using a calibrated analytical balance. Caliper should be measured with a paper thickness gauge or micrometer designed for paperboard, with documented contact area and pressure. A general-purpose handheld micrometer can give misleading results if test pressure is uncontrolled.
Supporting equipment may include a specimen cutter, conditioned test room or chamber, digital balance, moisture meter, compression tester, folding endurance fixture, temperature probe, test weights, and leak-testing setup. For foodservice packaging, the most useful laboratory setup combines material testing with actual-use trials. This allows the supplier and buyer to link a numerical board reading to customer-facing performance.
| Equipment | Primary Use | Control Point | Recommended Record | Common Error Prevented |
|---|---|---|---|---|
| Precision balance | Weigh defined board specimen | GSM calculation | Instrument ID and calibration date | Incorrect board-mass result |
| Standard specimen cutter | Cut known sample area | GSM consistency | Cut area and specimen count | Area calculation variation |
| Paperboard thickness gauge | Measure caliper under controlled pressure | Thickness tolerance | Individual readings and average | Operator-pressure bias |
| Conditioning chamber | Stabilise temperature and relative humidity | Pre-test preparation | Conditioning time and settings | Moisture-driven variation |
| Compression tester | Measure filled-pack stacking resistance | Structural performance | Peak load and deformation | Warehouse or delivery collapse |
| Hot-fill test station | Assess heat and liquid exposure | Functional suitability | Food/simulant, temperature, duration | Unrealistic dry-only approval |
Test equipment should be calibrated according to a documented schedule. Buyers do not need to own a full laboratory if they use qualified third-party laboratories, but they should be able to review the method, raw data, calibration status, and sample traceability. A supplier report containing only a single “pass” statement is not enough for high-risk food-contact packaging.
Caliper vs GSM: Test Conditions
Test conditions should reflect expected use, not merely ideal factory conditions. Before material testing, condition board samples in a controlled environment. For many paper and paperboard methods, a standard atmosphere around 23°C and 50% relative humidity is commonly used, but buyers should state the method and accepted range in the specification. The same condition must be used when comparing supplier batches.
Functional tests should use the actual food where feasible or an appropriate simulant when food testing is impractical. Hot water may be useful for liquid containment, but it may not represent greasy fried food, acidic sauces, cold condensation, or long delivery times. A practical test plan should define fill volume, food temperature, exposure duration, transport load, stacking arrangement, and inspection criteria.
| Food Application | Suggested Test Medium | Temperature | Holding Time | Additional Stress |
|---|---|---|---|---|
| Hot soup | Water-based soup or approved simulant | 85–95°C | 30–60 minutes | Carry load and lid-fit check |
| Fried chicken | Hot oily food or grease simulant | 65–80°C | 30–45 minutes | Stacking and closure cycling |
| Noodles with sauce | Wet starch-based food or simulant | 75–90°C | 30–60 minutes | Bottom deformation observation |
| Cold salad | Chilled salad and dressing | 2–8°C | 2–4 hours | Condensation and lid engagement |
| Bakery products | Dry warm food product | 25–45°C | 1–2 hours | Compression and print rub test |
| Meal delivery order | Representative mixed menu | Service temperature | 45–90 minutes | Vibration, bag carry, and stack load |
Document any change in board source, coating, ink system, glue, die-cut tooling, or converting process. Even where GSM and caliper remain within target, a process change can alter crease durability, odour, sealing, or food-contact performance. This is especially relevant when packaging is exported across different climate zones and used in high-volume quick-service restaurants.
The demand comparison illustrates why delivery kitchens and quick-service restaurants generally require the strictest structural validation. Their packaging must remain presentable after filling, stacking, bagging, and last-mile transportation.
Caliper vs GSM: Pass-Fail Limits
Pass/fail limits should be agreed before mass production. Procurement should avoid arbitrary limits copied from unrelated products. Instead, define a nominal GSM, a nominal caliper, tolerances, test method, sample quantity, acceptance rule, and required functional outcomes. Limits should be tight enough to protect performance yet realistic enough to account for normal paperboard variation.
As an illustrative starting point, a buyer may specify a target material such as 350 GSM with an agreed tolerance and a caliper range validated for the pack design. The actual range must be confirmed through prototypes and performance trials; it should not be treated as universal. A tall cup, shallow tray, and hinged meal box can require different caliper targets even when they use similar GSM.
Functional pass/fail criteria should be unambiguous. Examples include: no visible leakage; no base separation; no wall collapse; lid remains engaged; no cracking beyond an agreed visual threshold; deformation remains below an agreed limit; and a filled pack withstands its stated stack load. Photographs, dimensional measurements, and numerical data should support the decision.
Caliper vs GSM: Supplier Test Report
A supplier test report should allow a buyer to reproduce and audit the result. It should state the supplier name, product code, customer code, production lot, board grade, coating type, test standard or internal method, sample quantity, conditioning settings, equipment identification, calibration status, individual readings, averages, ranges, acceptance criteria, test conclusion, and responsible quality signature.
For a finished food container, the report should also include functional-test details: food or simulant used, fill volume, start temperature, ambient conditions, duration, stacking load, observed defects, final photographs when required, and conclusion against the approved golden sample. Buyers should retain approved reports by lot and link them to shipping documentation and complaint records.
Fude Packaging can provide product-specific inspection documentation for agreed projects, including batch verification and functional checks where specified. This is useful for importers consolidating multiple container types, because it makes it easier to compare results across cups, bowls, trays, burger boxes, and meal containers from one controlled manufacturing system.
Caliper vs GSM: Corrective Action
When a lot fails a GSM, caliper, or functional requirement, the first step is containment. Stop shipment or segregate affected stock, identify all related production lots, preserve samples, and notify relevant teams. The second step is confirmation: repeat measurements using conditioned specimens and calibrated equipment to distinguish an actual material deviation from a sampling or test-method error.
Root-cause analysis should investigate board supplier changes, moisture exposure, incorrect paper reel selection, coating variation, excessive calendering, printing pressure, die-cut settings, score depth, forming temperature, glue application, and storage conditions. Corrective action may include replacing material, adjusting converting settings, revising tolerance controls, retraining operators, increasing inspections, or revalidating the product design.
A corrective action report should show the nonconformance, immediate containment, verified root cause, correction, preventive action, ownership, completion date, and effectiveness review. For global market buyers, this report is important evidence that the supplier can manage repeatability rather than merely replace one defective shipment.
The trend shift toward documented sustainable-material controls is driven by customer expectations, extended producer responsibility rules in some markets, fibre sourcing requirements, compostability claims, and more detailed procurement audits. Buyers should distinguish recyclable, compostable, renewable-content, and food-contact claims rather than treating them as interchangeable.
Our Company: Fude Packaging for Caliper vs GSM
Fude Packaging supports overseas B2B buyers with controlled paper food packaging development and export supply. Our technical capabilities include material selection, coating recommendations, structural development, artwork and dieline review, prototype testing, caliper and GSM verification, and performance evaluation for heat, grease, moisture, leakage, strength, and lid compatibility. Our in-house laboratory helps link board measurements to the real application rather than treating thickness as an isolated number.
Our manufacturing capabilities are based on more than 20 years of industry experience, a self-owned 30,000 m² factory in Shandong, automated production lines, and production capacity of up to 120,000 units per day. We manufacture paper cups, paper bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, food trays, and multi-compartment meal boxes in-house. Buyers can review our food container range when planning a consolidated packaging programme across multiple foodservice formats.
For kraft-based takeaway applications, buyers can also explore our sustainable kraft paper takeout containers, which can be evaluated against application-specific targets for GSM, caliper, load, moisture resistance, and closure performance. Material recommendations can be adapted to the food type, serving temperature, destination requirements, branding needs, and desired end-of-life positioning.
Our service capabilities include OEM and ODM support, rapid sampling, Pantone colour matching, functional prototypes, export-ready packing, third-party inspection coordination, and documentation support for international shipments. We serve customers in more than 50 countries and can assist with projects shipped through ports such as Qingdao, Shanghai, Ningbo, Rotterdam, Felixstowe, Los Angeles, and Dubai. Standard orders are commonly completed in approximately 7–15 days, depending on specification and volume.
| Evaluation Criterion | Basic Supplier | Controlled Manufacturing Partner | Buyer Value |
|---|---|---|---|
| Material declaration | States GSM only | States GSM, caliper, board grade, coating, and tolerance | More complete purchase control |
| Sample approval | Visual sample only | Golden sample plus functional validation | Lower application risk |
| Production traceability | Limited carton information | Lot, date, material, and inspection linkage | Faster complaint investigation |
| Testing capability | Outsourced only or unavailable | In-house checks with third-party option | Better response speed |
| Customization | Standard sizes and generic printing | Material, structure, print, and pack configuration support | Better brand and application fit |
| International service | Quotation-focused support | Sampling, documentation, logistics, and claim handling | Reduced procurement workload |
This comparison chart is an illustrative procurement framework. Buyers should score suppliers against their own food-safety, commercial, quality, sustainability, and delivery requirements. The strongest option is not always the lowest quoted unit price; it is often the supplier that lowers total risk across quality consistency, freight utilisation, compliance readiness, and claim management.
FAQ — Paperboard Caliper and GSM Packaging for B2B Buyers
1. What failure risk does paperboard caliper and GSM packaging evaluation measure?
It measures the risk that packaging will fail because the board is too light, too thin, too dense, insufficiently stiff, or inconsistent from lot to lot. Potential outcomes include soft walls, weak closures, poor lid fit, stack collapse, leakage, distortion, and a lower-quality customer experience. The evaluation should always include functional tests for the intended food application.
2. Which samples and conditions should be used?
Use random samples from different cartons, pallet positions, and production periods. For qualification, include both flat board and formed packaging. Condition samples before measurement, then test with actual food or an appropriate simulant at expected temperature, duration, filling level, load, and transport conditions. Hot, oily, wet, chilled, and delivery applications should be tested differently.
3. How are results recorded objectively?
Record individual readings rather than only averages. Include sample ID, lot number, board source, coating, test method, instrument ID, calibration status, conditioning conditions, operator, average, minimum, maximum, specification limit, and pass/fail conclusion. For functional trials, include photographs and specific observations such as leakage, deformation, cracking, or lid disengagement.
4. What pass/fail limit should procurement set?
Procurement should set limits based on validated prototypes and the final application. The specification should include nominal GSM, GSM tolerance, nominal caliper, caliper tolerance, and functional requirements. Avoid copying limits from a different package type. A meal box, coffee cup, soup bowl, and dry bakery tray may require very different material ranges even if they appear similar.
5. How often should the test be repeated?
Repeat testing during supplier qualification, first-order approval, routine incoming inspection, after any material or process change, after a complaint, and at planned periodic requalification. High-risk formats should receive more frequent checks. Buyers with stable suppliers and strong batch records may use a risk-based reduced inspection plan, but should retain the ability to increase testing immediately when performance changes.
Looking toward 2026 and beyond, buyers should expect greater use of digital quality records, lot-level traceability, automated vision inspection, lower-plastic coating solutions, fibre-source verification, and more stringent sustainability claims. The most effective procurement strategy is to combine measurable GSM and caliper controls with real-world performance testing, clear documentation, and a supplier capable of maintaining the same approved standard at scale.
About the Author
Fude Packaging is a professional flexible packaging manufacturer serving global food brands, wholesalers, and distributors. Our team shares practical insights on custom packaging, printing technology, food-safe materials, and industry trends to help businesses build better packaging solutions.
Share
Product Category
Start Your Project With Fude Today
Related Post
-

Global Market Guide to Condensation-Resistant Paper Packs
A reliable evaluation of condensation-resistant paper packaging requires a repeatable test method using controlled samples, a defined food product or simulant, specified temperatures, exposure duration, stacking load, and objective pass/fail limits. For Global market buyers, the result should not remain an informal sample observation. It should become part of the approved product specification, supplier quality agreement, incoming inspection plan, and corrective-action process.Condensation is created when hot food, cold ingredients, external humidity, or rapid temperature changes cause water vapor to collect on or inside paper packaging. In practical food-service operations, this moisture can soften the board, weaken folds, reduce stacking strength, stain printed areas, cause lid deformation, promote leakage, or make a package look unsuitable at delivery. A paper bowl that performs well in a dry warehouse may fail after twenty minutes containing hot noodles, chilled salad components, fried food, or sauce.Buyers should test the exact packaging configuration they will purchase: the approved paper grade, coating, printing, glue, size, lid, food-contact side, and packing method. A test report for an unprinted sample or a different coating construction is not enough. The accepted test should reproduce realistic conditions at restaurants, airports, catering kitchens, convenience stores, dark kitchens, supermarkets, and delivery routes.For procurement teams, the practical objective is simple: define what “acceptable moisture performance” means before placing a high-volume order. This prevents disputes after containers reach distribution centers in Rotterdam, Los Angeles, Dubai, Singapore, Sydney, Hamburg, or São Paulo.Evaluation ElementRecommended RequirementWhy It MattersSample identityRecord SKU, size, board grade, coating, print version, and production dateEnsures the tested item matches the approved purchase specificationFood or simulantUse actual food where possible; otherwise use controlled hot water, oil, or sauce simulantReplicates moisture exposure and contact conditionsFill temperatureDefine a range, such as 75–90°C for hot mealsTemperature strongly affects vapor generation and board softeningExposure timeMeasure at 15, 30, 45, and 60 minutesReflects kitchen holding, pickup, and delivery windowsStacking loadApply a defined number of filled packs or calibrated weightChecks deformation under transport and restaurant storage conditionsAcceptance criteriaSet numeric limits for leakage, delamination, collapse, stains, and dimensional changeReduces subjective approval decisions and claim disputesThe table above can be converted into a product-specific inspection sheet. Different products require different thresholds. A soup bowl may prioritize seam integrity and bottom stiffness, while a kraft burger box may prioritize fold retention, top-panel sag, grease control, and resistance to moisture escaping from hot fried food.Condensation resistance measures a package’s ability to maintain functional strength, appearance, and food containment when exposed to moisture generated by the packed food or the surrounding environment. It does not only mean “waterproof.” A package can resist direct liquid contact yet still lose compression strength because steam migrates into paper fibers through edges, creases, uncoated areas, or poor sealing zones.For Global market importers and distributors, the buyer risk is amplified by longer supply chains. Packaging may be produced in China, loaded through Qingdao or Shanghai, transferred through Singapore, Jebel Ali, Hamburg, or Long Beach, stored in humid conditions, then distributed to restaurants in multiple climate zones. Although the food-contact test happens after the package arrives at the customer site, warehouse humidity and carton protection can affect the starting condition of paper products.The most common commercial risks include food leakage, container collapse, moisture staining, lid-fit loss, customer complaints, wasted food, refunds from delivery platforms, damaged brand perception, and rejected inventory. A minor packaging weakness can become expensive when a restaurant chain uses thousands of units daily.Failure ModeTypical CauseCommercial ImpactSoft bottom panelInsufficient barrier coating or high moisture absorptionContainer distortion, leaks, and unsafe carryingSidewall collapseLow wet strength or excessive hot-food holding timeFood spillage during takeaway deliveryDelaminated paper layersPoor adhesive compatibility or repeated moisture exposureVisible quality defect and loss of structural integrityStained printingCondensation penetration through board or inadequate ink protectionBrand appearance issues and retail rejectionLid looseningRim deformation caused by heat and steamLeakage of soup, noodles, coffee, or saucesStack compression failureWet board strength below transport requirementDamage to multiple packed meals in delivery bagsFor restaurant chains, the most meaningful risk is not a laboratory-only defect. It is a service failure at the moment a consumer opens a delivered meal. Therefore, testing should consider the full meal format: a hot entrée, sauce cup, cold garnish, lid, outer bag, and realistic delivery duration.var ctx = document.getElementById('lineChart').getContext('2d');var chart = new Chart(ctx, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026', '2027'],datasets: [{label: 'Indexed Global Demand for Moisture-Resistant Food Packaging',data: [100, 108, 117, 128, 140, 154],borderColor: 'rgb(35, 125, 90)',backgroundColor: 'rgba(35, 125, 90, 0.10)',fill: false,tension: 0.3}]},options: {responsive: true, maintainAspectRatio: false}});The line chart illustrates a realistic directional procurement trend: demand for paper food packaging with verified moisture performance is rising as takeaway, delivery, convenience food, and sustainability requirements grow together. Buyers increasingly request performance evidence rather than relying only on material descriptions.Sample size should be large enough to identify normal production variation. One successful sample proves very little. For product development, buyers can begin with five units per condition. For approval and routine verification, a practical minimum is often ten units per condition, with additional samples when the package contains seams, windows, special coatings, multi-compartment structures, or unusually high fill temperatures.Samples should be selected from different points in the production batch whenever possible. This may include the beginning, middle, and end of a manufacturing run. If printed packaging is involved, include samples from each print position or color-heavy area because ink coverage, drying conditions, and board handling may affect performance.Test StageSuggested Sample QuantityPurposeMaterial screening5 units per constructionCompares paper grades, coatings, and structural optionsPrototype approval10 units per food conditionConfirms suitability before artwork and mass productionFirst production batch13–20 units per SKUChecks scale-up consistency and forming qualityRoutine lot verification10 units per lot or agreed production intervalSupports ongoing supplier controlComplaint investigation20 or more units, including retained samplesIdentifies whether failure is isolated or systematicHigh-risk chain rollout30 units across locations or shiftsValidates real operational performance before national launchThe sample plan should distinguish between cosmetic observations and functional failures. A faint, non-progressive moisture mark may be acceptable for a natural kraft container, depending on brand requirements. A soft base that prevents safe carrying is not acceptable. Procurement teams should agree on this distinction before supplier quotations are compared.The equipment does not need to be overly complex, but it must be controlled and calibrated. The basic setup includes a thermometer or temperature probe, timer, digital scale, measuring ruler or caliper, standardized load weights, controlled food or simulant containers, camera, test forms, and a flat test surface. Advanced in-house laboratories may also use humidity chambers, compression testers, Cobb absorption equipment, burst-strength testing, thickness gauges, and data logging systems.For buyers purchasing paper cups, noodle boxes, salad bowls, burger boxes, or meal trays, the most useful test equipment is the equipment that reproduces operational failure. A compression tester is valuable for stacked meal boxes. A controlled hot-fill station is useful for soup cups. A camera station with fixed lighting is useful for comparing moisture staining objectively across production batches.EquipmentPrimary UseRecommended ControlDigital thermometerMeasures fill and surface temperaturesVerify calibration regularlyDigital scaleControls fill mass and load applicationUse the same target fill weight for all samplesTimerRecords exposure intervalsStart timing immediately after filling and closingCompression fixture or weightsSimulates stacked delivery packsSpecify load in kilograms or number of filled containersHumidity chamberSimulates tropical or humid storage conditionsDefine temperature and relative humidity set pointsFixed-light camera stationDocuments staining, swelling, and deformationUse standard background, angle, and photo distanceWhen suppliers present laboratory data, buyers should ask whether the equipment was used on finished converted packaging or only on raw paper. Raw-material results are informative, but they do not replace finished-product testing. Die-cutting, folding, side seams, glue, rim forming, and printing can all change real performance.Test conditions should mirror actual use. A hot noodle bowl in London winter delivery conditions behaves differently from a rice meal box carried in humid Bangkok weather or a salad container packed with chilled ingredients in Dubai. The correct test protocol depends on food type, service temperature, delivery time, package geometry, and consumer handling.A practical test begins by conditioning empty samples in a defined room environment. Fill each sample with the same mass of actual food or simulant at the specified temperature. Close the package using the approved lid or closure. Hold it for the agreed time. If stacking is relevant, apply the defined load after filling. Inspect at each time point for leakage, board softening, seam opening, delamination, print transfer, and dimensional change.ApplicationSuggested Food or SimulantTypical Test ConditionHot soup bowlWater-based soup simulant85°C fill, 45 minutes, lid closedNoodle containerHot noodles with broth80°C fill, 30–60 minutes, stacked loadFried-food boxFresh fried chicken or fries75°C food, 30 minutes, venting evaluatedRice meal boxRice, sauce, vegetables, protein70°C fill, 45 minutes, delivery bag simulationCold salad bowlChilled salad with dressing cup4–8°C storage, humid exterior exposureBakery or dessert cartonWarm baked product or chilled dessertTemperature transition from kitchen to retail displayThe table provides starting conditions, not universal limits. Buyers should adjust them after observing their menu and logistics. For example, a food-delivery platform may require sixty minutes of performance because riders travel longer distances. An airport catering operator may need tests involving chilled storage followed by ambient exposure. A restaurant serving highly acidic or oily sauces may need additional barrier and grease-resistance testing.Pass/fail limits convert visual impressions into purchase requirements. The best limits are measurable, relevant, and easy for both buyer and supplier to verify. They should address the failure modes that matter for each package category rather than copying a generic requirement from another product.A clear specification may state that no visible leakage is allowed; no seam opening is allowed; no collapse is allowed under a specified load; rim diameter change must remain within a defined tolerance; external wetting must not exceed a defined visual grade; and package tilt testing must show no loss of contained liquid. If a product has a natural kraft appearance, the buyer may allow slight color darkening but prohibit fiber breakdown or moisture transfer to the outer delivery bag.Performance AttributeExample Pass LimitInspection MethodLeakageNo visible liquid leakage during test periodVisual inspection on dry absorbent surfaceBottom integrityNo softening that prevents normal liftingLift filled pack after designated exposureSidewall deformationNo collapse; height reduction within agreed toleranceMeasure before and after exposureSeam conditionNo opening, peeling, or separationVisual and light manual inspectionStacking strengthNo failure under defined vertical loadApply calibrated weight for set durationExterior appearanceNo unacceptable staining, print smearing, or transferFixed-light photo comparison and gradingDo not set impossible limits that ignore the nature of paper packaging. The goal is not always zero visible moisture effect; it is fitness for use. A responsible supplier should help define a realistic limit based on the selected board, coating, compostability target, food temperature, and intended duration.var ctx = document.getElementById('barChart').getContext('2d');var chart = new Chart(ctx, {type: 'bar',data: {labels: ['Delivery Meals', 'Quick-Service Restaurants', 'Cafés', 'Catering', 'Retail Ready Food', 'Airports'],datasets: [{label: 'Relative Demand for Condensation Control',data: [92, 86, 68, 76, 73, 64],backgroundColor: ['#2c7a7b','#3182ce','#805ad5','#dd6b20','#38a169','#d69e2e']}]},options: {responsive: true, maintainAspectRatio: false}});The bar chart shows why delivery meals and quick-service restaurants normally require the strictest condensation-resistance controls. They combine hot food, rapid packing, stacking, enclosed bags, variable delivery times, and high consumer visibility.A supplier test report should allow a buyer to understand exactly what was tested and whether the result applies to the ordered product. At minimum, the report should include the product code, photographs, material construction, sample quantity, production batch reference, food or simulant, fill mass, temperature, exposure duration, load, test environment, observations, pass/fail decision, tester name, and approval signature.Reports should include failures as well as passes. A supplier who only provides selected photos of successful samples does not provide a fully auditable quality record. For high-volume tenders, buyers may request retained samples, video evidence, third-party verification, or a witnessed test before shipment.Report FieldBuyer Verification QuestionImportanceProduct identificationDoes the SKU match the approved artwork and specification?Prevents substitution of a different sampleMaterial constructionAre paper, coating, glue, and lid details stated?Confirms the tested structure is representativeSample countHow many units passed and failed?Shows variation rather than a single resultTest conditionsWere temperature, mass, duration, and load controlled?Allows repeatability between buyer and supplierPhoto evidenceAre before-and-after photos taken consistently?Supports objective appearance assessmentConclusionIs the pass/fail decision linked to an agreed limit?Makes the report commercially actionableFor international procurement, reports should be written clearly enough for quality teams in different countries to interpret consistently. A retailer in Germany, a distributor in the United Arab Emirates, and a restaurant operator in Canada should be able to review the same report without relying on informal explanations.If samples fail, corrective action should start with identifying the failure mechanism. Increasing coating weight may help, but it is not always the right solution. The problem may instead be poor fold design, insufficient venting, weak adhesive, unsuitable board bulk, excessive food temperature, incompatible lid geometry, poor carton storage, or an unrealistic packing process.Corrective action should follow a documented process: contain affected goods, define the defect, review production and material records, test retained samples, identify root cause, implement a corrective measure, re-test under the same conditions, and confirm that the change has not created new issues such as reduced recyclability, poor print adhesion, odor, or lid-fit variation.For example, a fried-food box may become soft because trapped steam has no exit. A heavier barrier may not solve the root problem as effectively as adding controlled vents or changing the fold structure. A hot soup container with rim leakage may need a revised lid fit or rim-forming tolerance rather than a different paper grade.var ctx = document.getElementById('areaChart').getContext('2d');var chart = new Chart(ctx, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026', '2027'],datasets: [{label: 'Share of Buyer Specifications Requiring Moisture Validation (%)',data: [34, 41, 49, 58, 66, 74],borderColor: 'rgb(49, 130, 206)',backgroundColor: 'rgba(49, 130, 206, 0.25)',fill: true,tension: 0.3}]},options: {responsive: true, maintainAspectRatio: false}});The area chart reflects the shift from general material claims toward documented functional validation. By 2026 and beyond, packaging buyers are expected to combine food-contact compliance, sustainability declarations, and application-based performance testing within a single approved specification.Fude Packaging supports Global market buyers with paper food packaging designed around actual food-service requirements, including condensation exposure, heat retention, grease contact, structural strength, and delivery handling. Rather than treating moisture resistance as a generic claim, we can help customers match material construction and testing conditions to their food type, service format, destination market, and brand objective.Our technological capabilities include material selection, coating recommendations, structural development, prototype testing, print adaptation, dieline checking, and in-house functional evaluation. For hot noodles, soup bowls, meal boxes, and takeaway containers, we can review steam generation, expected holding time, food mass, lid compatibility, and stacking requirements before mass production. This helps buyers avoid selecting a package only by appearance or unit price.Our manufacturing capabilities are supported by more than 20 years of packaging experience, a self-owned 30,000 m² factory in Shandong, automated production lines, and capacity of up to 120,000 units per day. Material selection, printing, die-cutting, forming, inspection, packing, and shipment are managed within our production system. This direct control supports more consistent implementation of approved board grades, coatings, dimensions, and print standards for international orders.Our service capabilities include OEM and ODM support, white samples, printed samples, functional prototypes, export-ready packing, document coordination, and communication for overseas customers. We have served customers in more than 50 countries and can support buyers shipping through major trade routes and ports, including Qingdao, Shanghai, Rotterdam, Hamburg, Long Beach, Melbourne, and Jebel Ali. Customers can also arrange third-party inspection or independent testing before shipment.For buyers sourcing kraft takeaway formats, explore our sustainable kraft paper takeaway containers. For broader menu programs, review our food container packaging range for bowls, lunch boxes, salad containers, trays, and other food-service formats.Buyer RequirementFude Packaging SupportExpected Procurement BenefitHot-food moisture controlMaterial and structure recommendations based on use conditionsLower leakage and softening riskCustom brandingArtwork review, Pantone matching, and printed sample approvalMore consistent brand presentationMultiple packaging categoriesPaper cups, bowls, boxes, trays, and meal containers from one supplierSimplified purchasing and container planningQuality verificationIn-house inspection, test records, and third-party inspection supportBetter batch confidence before shipmentRegulatory readinessSupport for relevant food-contact and sustainability documentationImproved market-entry preparationInternational serviceSampling, export documents, logistics coordination, and claim handlingReduced cross-border sourcing complexityvar ctx = document.getElementById('comparisonChart').getContext('2d');var chart = new Chart(ctx, {type: 'bar',data: {labels: ['Test Documentation', 'Custom Development', 'Batch Consistency', 'Export Support', 'Multi-SKU Supply', 'Third-Party Inspection'],datasets: [{label: 'Integrated Supplier Capability Score',data: [90, 88, 86, 89, 92, 84],backgroundColor: 'rgb(128, 90, 213)'},{label: 'Basic Transactional Supplier Score',data: [55, 48, 58, 50, 42, 35],backgroundColor: 'rgb(160, 174, 192)'}]},options: {responsive: true, maintainAspectRatio: false}});The comparison chart demonstrates why buyers should compare suppliers beyond quoted unit price. A supplier with integrated testing, customization, manufacturing control, and export support can reduce the hidden cost of quality claims, fragmented sourcing, late corrections, and inconsistent specifications.It measures whether paper packaging can retain its structure, containment, and appearance when exposed to moisture caused by hot food, steam, chilled products, humidity, sauces, or temperature changes. Typical risks include bottom softening, leakage, sidewall collapse, seam failure, print staining, lid loosening, and reduced stacking strength.Use finished packaging from the approved specification, including the correct paper grade, coating, print, adhesive, lid, and size. Test with the actual food whenever practical. If using a simulant, control the fill mass, temperature, duration, closure method, and stacking load. Conditions should match the customer’s actual kitchen, delivery, retail, or catering process.Use a standardized form with sample identification, fill temperature, food mass, exposure time, load, room conditions, photos, measurements, observations, pass/fail limits, and signatures. Fixed lighting and consistent photo angles improve comparison. Measurements such as height reduction, rim deformation, leakage occurrence, and load survival make results more reliable than visual comments alone.Set limits based on fitness for use. At minimum, define no visible leakage, no seam opening, no unsafe loss of lift strength, no collapse under the agreed load, and no unacceptable staining or print damage. For higher-risk applications such as soup, noodles, and stacked delivery meals, include time-based performance and lid-fit requirements.Repeat testing during prototype approval, first mass production, material or coating changes, major artwork changes, complaint investigations, and regular lot verification. High-volume restaurant chains may also require periodic verification by production batch, monthly production cycle, or shipment schedule. The frequency should reflect product risk, order volume, and the cost of field failure.Looking toward 2026, buyers should expect stronger demand for data-backed packaging specifications, lower-plastic material solutions, recyclable or compostable options where locally appropriate, improved water-based barrier technologies, digital batch traceability, and more detailed food-service testing. Policy changes across Europe, North America, the Middle East, Asia-Pacific, and other Global market regions will continue to increase attention on food-contact compliance, waste reduction, and packaging performance in real delivery conditions. -
Delivery Food Packaging Selection Guide for Canada
Delivery food packaging should be selected around the actual conditions of transport: whether the food is hot, cold, dry, oily, sauced or liquid; how much it weighs; how long it will remain packed; how it is stacked; and how customers open, carry and reheat it. A container that performs well for a 15-minute urban delivery in downtown Toronto may fail during a 45-minute trip across the Greater Toronto Area, a winter delivery in Calgary, or a multi-order courier route in Vancouver.For Canadian delivery-first brands, the best approach is to start with the menu rather than the cheapest container. Define the serving temperature, fill weight, moisture level, sauce volume, delivery radius, sealing requirement and intended customer experience. Then test samples under realistic service conditions before approving a bulk purchase.Reliable delivery packaging usually requires a combination of the right material, structure and lid system. For example, dry fried foods may require ventilation; oily foods need grease resistance; sauced meals need secure seams and lids; and soups require reliable leak resistance plus secondary carrying support. A practical approval record should include approved dimensions, material details, print standard, lid fit, leakage threshold, stacking performance and production sample reference.Decision FactorWhat to ConfirmTypical Risk if IgnoredFood temperatureHot, chilled, frozen or mixed-temperature useSoftened board, condensation or unsafe handlingFood weightNet fill weight plus sauce and garnishBottom deformation or lid displacementOil contentLight oil, fried food, fatty protein or butter sauceGrease penetration and weak appearanceLiquid volumeSoup, broth, gravy, dressing or beverage amountLeakage during courier movementDelivery time15, 30, 45 or 60-minute holding periodLoss of heat, texture or container strengthCustomer handlingOpening, sharing, reheating and disposal needsMessy unboxing and negative reviewsThis checklist helps purchasing teams move from generic food containers to a measurable delivery food packaging specification. It also makes it easier to compare supplier samples fairly and reduce avoidable packaging complaints.Delivery food packaging is most effective when the container supports both food protection and brand presentation. In Canada, common applications include restaurant takeout, ghost kitchens, university food service, corporate catering, meal-prep subscriptions, grocery prepared foods, coffee shops and delivery-platform merchants.For restaurants in Montreal, Ottawa and Toronto, compact containers with strong stacking performance are useful where courier bags carry several orders at once. In Vancouver and Victoria, moisture management is important for seafood, rice bowls and fresh salads. In Prairie cities such as Edmonton, Winnipeg and Saskatoon, packaging should tolerate seasonal temperature swings during pickup and last-mile delivery.Quick-service restaurants serving burgers, fried chicken, wraps and sides. Asian cuisine brands serving noodles, rice bowls, dumplings, soups and curries. Meal-prep businesses supplying chilled weekly portions. Cafés and bakeries delivering beverages, breakfast items and desserts. Corporate caterers preparing multi-compartment lunch formats. Retail food counters supplying ready-to-eat meals through grocery channels. var ctxIndustryDemand = document.getElementById('industryDemandChart').getContext('2d');new Chart(ctxIndustryDemand, {type: 'bar',data: {labels: ['Quick Service', 'Asian Cuisine', 'Meal Prep', 'Cafés', 'Catering', 'Retail Prepared Food'],datasets: [{label: 'Estimated Delivery Packaging Demand Index in Canada',data: [92, 85, 76, 68, 61, 73],backgroundColor: ['#b85c38','#d88b4a','#6c8e6b','#8e6c88','#527f9b','#c5a253']}]},options: {responsive: true, maintainAspectRatio: false, scales: {y: {beginAtZero: true, max: 100}}}});The chart illustrates relative demand patterns for delivery-oriented food packaging categories. Quick-service and Asian cuisine operators often require the broadest mix of bowls, boxes, trays, cups and leak-resistant lids.Food condition is one of the most important selection variables. Dry foods, greasy foods, sauced dishes and liquids create different stresses on fibre packaging, coatings, folds, seams and closures. A single box format may not be suitable for every item on a menu.Food TypeRecommended FormatImportant Packaging FeatureFrench fries and fried chickenVentilated clamshell or fry boxAirflow to reduce trapped steamBurgers and sandwichesRigid folding burger boxGrease-resistant board and stable closurePasta and rice bowlsPaper bowl with fitted lidHeat resistance and secure lid engagementCurry and sauced entréesDeep bowl or food tray with lidLeak-resistant seams and splash controlSoup and broth noodlesRound soup container with tight lidLeak prevention and compression strengthSalads and cold dessertsClear-lid bowl or salad containerVisibility, cold stability and dressing separationDry foods need protection from crushing and excess condensation. For fries, onion rings and crispy chicken, a fully sealed container can trap steam and reduce texture quality. Strategic ventilation is often more valuable than maximum closure.Greasy foods need paperboard and coatings that resist visible oil migration. Grease marks can make a premium meal look poorly packed even when the food is safe. For burgers, poutine, pastries and fried snacks, test the package after holding food at the real serving temperature.Sauced meals need enough headspace to prevent spills when couriers turn corners, climb stairs or place orders in insulated delivery bags. Liquids require the highest test standard: fill the pack to the intended level, close it, tilt it, invert it briefly if suitable, and simulate vibration or stacking.A Canadian Korean fried chicken brand may use one vented box for dry wings, one grease-resistant bucket for glazed chicken, and separate sauce cups for dipping sauces. Using the same sealed bowl for all three items may create sogginess, leakage and an inconsistent customer experience.Delivery time changes packaging performance. A container suitable for a 10-minute pickup order may not be reliable after 45 minutes in a courier bag. Restaurants should establish a realistic hold-time range based on delivery zones, traffic, weather, courier availability and multi-stop dispatching.In central Toronto or downtown Vancouver, short-distance orders may arrive quickly, but elevator waits, apartment access and traffic congestion can still extend the actual hold time. In suburban areas around Mississauga, Brampton, Surrey or Laval, delivery routes may be longer and more variable. Winter conditions in Canada can add further stress when hot meals meet cold outdoor temperatures.Delivery ScenarioTypical Hold TimePriority Packaging RequirementCounter pickup5–10 minutesFast packing and basic structural protectionDense urban delivery15–25 minutesStacking strength and spill resistanceSuburban courier route25–40 minutesHeat retention and strong lid securityMulti-order batch delivery30–45 minutesCompression strength and clear order separationWinter delivery30–60 minutesInsulation support and condensation controlCatering or scheduled meal drop45–90 minutesLarge-format stability and tamper-evident handlingThe table shows why a delivery-first brand should test packaging at the longest normal delivery time, not only under ideal pickup conditions. The test should include real food, normal fill level, common courier bag conditions and actual stacking.var ctxMarketGrowth = document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctxMarketGrowth, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026', '2027'],datasets: [{label: 'Canadian Delivery-Ready Packaging Demand Index',data: [100, 108, 116, 124, 133, 142],borderColor: '#2f6f73',backgroundColor: 'rgba(47,111,115,0.12)',borderWidth: 3,fill: false,tension: 0.3}]},options: {responsive: true, maintainAspectRatio: false, scales: {y: {beginAtZero: false}}}});This planning trend line reflects continuing demand for packaging that protects food quality, supports branded delivery and helps operators standardize service across multiple locations.Packaging dimensions should match the order format. Single portions need portion control and easy handling. Combo meals need separation between components. Sharing formats need strength, stacking ability and convenient opening. Oversized packs can make food look underfilled, while undersized packs can compress toppings, damage presentation and increase leakage.Order FormatBest Container ApproachUseful Add-OnSingle rice or noodle bowlRound or rectangular bowl with lidSeparate sauce cupBurger mealBurger box plus side containerDrink carrier or cup trayTwo-person comboMultiple clearly sized containersTamper seal and bag organiserFamily mealLarge tray or compartment meal boxStrong external carry bagOffice lunch orderStackable individual meal boxesName label areaMeal-prep subscriptionRepeatable portioned tray systemReheating and storage instructionsFor combo meals, do not assume a multi-compartment box always improves the experience. Compartments are useful when food components must remain separated, such as rice, protein and vegetables. They are less suitable when a sauce needs to coat the full dish or when deep liquid content can move between sections.Customers judge quality before tasting the meal. A clean, well-fitted package can make a delivery order feel organized and premium. A greasy exterior, loose lid, collapsed box or oversized container can reduce perceived value even if the kitchen prepared the food correctly.Presentation details include the opening direction, food visibility, printed design, logo placement, insert cards, sauce organization and the absence of leakage. In competitive markets such as Toronto, Montreal and Vancouver, repeat customers often compare restaurants through delivery photos, unboxing videos and ratings. Packaging therefore supports both operations and marketing.For branded packaging projects, start with a functional white sample before moving to a printed proof. After verifying dimensions and performance, review the final print proof for logo scale, barcode area, colour consistency, readable food labels and safe margins around folds.var ctxPresentationTrend = document.getElementById('presentationTrendChart').getContext('2d');new Chart(ctxPresentationTrend, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026', '2027'],datasets: [{label: 'Basic Unbranded Packaging',data: [66, 61, 56, 51, 47, 43],borderColor: '#9a6b4a',backgroundColor: 'rgba(154,107,74,0.22)',fill: true,tension: 0.3},{label: 'Branded Functional Packaging',data: [34, 39, 44, 49, 53, 57],borderColor: '#416f5b',backgroundColor: 'rgba(65,111,91,0.25)',fill: true,tension: 0.3}]},options: {responsive: true, maintainAspectRatio: false, scales: {y: {beginAtZero: true, max: 70}}}});The area chart shows a typical market shift toward packaging that combines functional performance with brand visibility. The trend is especially relevant for delivery brands that depend on online repeat orders.No packaging format is universal. A paper-based box should not be selected merely because it looks sustainable or costs less. The format must suit the menu and distribution process.A vented fried-food box should not be used for soups, broths or high-volume curries. A shallow tray should not be used for tall layered meals that may shift during transport. A standard paper bowl should not be used for extremely oily or acidic food without confirming the appropriate barrier material. A clear-lid cold-food container should not be assumed suitable for high-temperature foods. A large family tray should not be used for single portions where presentation and heat loss matter. A multi-compartment pack should not be used if liquids can overflow between compartments. When the food contains high levels of liquid, oil, steam or weight, ask the supplier to recommend a tested structure rather than choosing only by appearance. A pack should also be compatible with the intended lid, sealing method and courier bag orientation.The following table can be used as a starting point for menu engineering, procurement discussions and sample requests. Final selection should always be confirmed through service trials with the real recipe and delivery route.Menu ItemSuggested PackagingKey TestCanadian Delivery ConsiderationChicken shawarma plateCompartment meal boxOil resistance and divider strengthSeparate garlic sauce to avoid leakageRamen or phoDeep soup bowl with secure lidLeak and heat testPack noodles and broth separately for longer routesPoutineGrease-resistant bowlBottom strength after 30 minutesVentilation can reduce sogginessSushi platterLow-profile tray with clear lidLid fit and cold stabilityProtect presentation during courier stackingButter chicken with riceRound bowl or divided traySauce splash and lid sealAllow adequate headspace for hot sauceMeal-prep entréePortioned rectangular trayChilled storage and reheating suitabilityUse consistent portions for subscription ordersSalad with dressingSalad bowl with separate cupCondensation and lid clarityKeep crunchy toppings dry until openingUse this table to create a packaging matrix for every SKU. For each item, document container code, lid code, capacity, minimum board or material requirement, approved supplier, packing quantity and acceptance test result.Fude Packaging supports overseas B2B buyers seeking scalable paper food packaging for Canadian food-service, distribution and retail projects. The company offers packaging across cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, trays and multi-compartment meal packaging. Buyers can explore the available range through the food packaging product collection.Packaging performance depends on material selection, structural design, printing control and testing. Fude Packaging uses an in-house laboratory to support practical evaluation of leak resistance, grease resistance, structural strength, lid compatibility and food-contact performance. For customized projects, the team can assist with artwork review, dieline checking, Pantone colour matching, material recommendations and prototype development.For Canada-bound packaging programs, documentation and material selection can be aligned with applicable food-contact, quality and sustainability needs. Available support includes FDA-related food-contact documentation, FSC materials, ISO 9001 systems and selected compostability options where appropriate to the product and destination requirement.With more than 20 years of industry experience, a self-owned 30,000 m² production base and automated capacity of up to 120,000 units per day, Fude Packaging can support recurring orders, branded product launches and multi-category procurement. Direct control over printing, die-cutting, forming, inspection, packing and shipment helps improve consistency across repeat orders.The company has experience supporting buyers that need to consolidate multiple packaging types under one supplier. This can simplify container loading, artwork management, quality control and replenishment planning for distributors, restaurant groups and meal-service operators. Learn more about the company through the Fude Packaging company profile.Fude Packaging provides OEM and ODM support from early packaging selection to mass-production coordination. Buyers may request digital proofs, white samples, printed samples or pre-production proofs before approving full production. Full-batch traceability and defined inspection stages support a repeatable approval process.For Canadian importers, shipments may be planned through major logistics gateways such as the Port of Vancouver, Port of Montreal, Toronto-area distribution centres and cross-country warehouse networks. The team can support export packing, commercial documents, scheduled production and practical communication around delivery deadlines. View available support through custom packaging services.var ctxSupplierComparison = document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctxSupplierComparison, {type: 'bar',data: {labels: ['Customization', 'Production Scale', 'Sample Options', 'Quality Traceability', 'Multi-Category Supply', 'Export Support'],datasets: [{label: 'Fude Packaging Capability Score',data: [92, 90, 94, 91, 89, 88],backgroundColor: '#486c8d'},{label: 'Typical Single-Category Supplier Score',data: [62, 58, 65, 60, 52, 57],backgroundColor: '#b5a16b'}]},options: {responsive: true, maintainAspectRatio: false, scales: {y: {beginAtZero: true, max: 100}}}});This comparison chart is a procurement planning tool. Buyers should validate actual requirements, samples, documents, lead times and quality standards during supplier qualification.Canadian buyers may source from local distributors, regional converters or overseas manufacturers. Local suppliers can provide fast replenishment for standard inventory, while overseas manufacturing may offer stronger customization, broader product consolidation and more competitive pricing for planned volumes. The right model depends on demand predictability, storage capacity, lead time, order quantity and branding complexity.Supplier OptionBest ForBuying ConsiderationLocal cash-and-carry supplierUrgent standard stockLimited customization and higher unit costCanadian regional distributorRegular replenishmentCheck inventory depth and SKU consistencyLocal custom converterShort-run branded packagingConfirm capacity during peak seasonsOverseas direct manufacturerPlanned volume and customizationManage sampling, shipping and production scheduleMulti-supplier modelRisk diversificationMaintain consistent specifications across sourcesSingle-source packaging partnerMulti-category consolidationAudit quality systems and continuity plansBefore issuing a purchase order, request samples and define measurable acceptance criteria. Typical criteria include capacity tolerance, lid fit, leak performance, grease resistance, compression strength, print colour, odour, cleanliness, carton count and shipment marking. For a tailored quotation or sample discussion, contact the Fude Packaging export team.Pack the actual menu item at normal serving temperature and fill weight. Hold the packed food for the maximum expected delivery time. Place units in the same bags or crates used by couriers. Stack orders as they are handled during real service. Check leakage, grease marks, lid movement, temperature loss and food appearance. Ask staff and customers to assess opening convenience and perceived value. Record results with photos, date, food type, container code and corrective actions. By 2026 and beyond, Canadian delivery packaging decisions will increasingly be shaped by sustainability expectations, municipal waste policies, extended producer responsibility programs, food-service labour shortages and consumer demand for convenient but lower-waste packaging.One important trend is material optimization: using sufficient board strength and barrier performance without unnecessary material weight. Another is better separation of hot and cold items, including compartment systems and secondary carriers that reduce spills. Digital printing and shorter branded production runs are also becoming more useful for seasonal menus, promotions and regional campaigns.Technology will improve approval processes as well. Brands are likely to use digital dieline approvals, batch traceability, QR-enabled packaging information and standardized test records. Procurement teams will increasingly evaluate total landed cost rather than only unit price, including defect risk, freight efficiency, storage space, customer complaints and brand consistency.Yes, provided the format is selected for the actual food condition. Hot foods require heat and moisture management; oily foods need grease resistance; sauced foods need secure seams and lids; and liquids need robust leak testing. One packaging style should not be assumed suitable for every menu item.Test at the normal packing temperature and at the longest expected delivery duration. For many urban delivery brands, this means at least 30 to 45 minutes. Include seasonal conditions where relevant, especially Canadian winter routes and longer suburban deliveries.Pack food at the intended fill level, close the lid, hold it for the planned delivery time and simulate handling through stacking, tilting and movement. Inspect the seams, lid edge, bottom panel and outer surface for visible leaks, grease migration, softening or deformation.The best size matches the food volume, toppings, sauce level and desired presentation. Choose enough headspace to prevent splashing but avoid excessive empty space. Round bowls suit soups and sauced meals; rectangular trays suit meal prep; boxes suit burgers, fried foods and dry combinations.A real-service trial should include the actual recipe, expected serving temperature, normal portion size, common delivery bag, courier-style stacking, maximum delivery time and customer opening review. Record results in a repeatable approval file before placing a full production order. -
Packaging Cost per Meal in Canada: Full Cost Model
Packaging cost per meal is not simply the supplier’s quoted price for a bowl, cup, tray, box, lid, napkin or cutlery kit. For Canadian food-service operators, meal-prep brands, distributors and procurement teams, a practical calculation includes fixed setup costs, variable unit costs, inbound freight, customs-related handling, warehousing, secondary packaging, production and handling waste, defects, returns, and obsolete inventory.A useful starting formula is:Packaging Cost per Meal = (Allocated Setup Cost + Product Cost + Freight + Storage + Secondary Packaging + Waste Allowance + Defect Allowance + Obsolescence Allowance) ÷ Usable Meals PackedFor example, a Toronto meal-delivery company may buy a 1,000 mL paper bowl at CAD 0.31 per unit. The quote can look competitive until the buyer adds CAD 0.04 for ocean and domestic freight, CAD 0.015 for warehouse handling, CAD 0.025 for a lid and corrugated shipper allocation, and an allowance for 4% waste. The real packaging cost may be CAD 0.42 to CAD 0.46 per meal rather than CAD 0.31.The decision should therefore be based on landed and usable cost, not headline unit price. Confirm the specification using a white sample, printed proof or food-filled trial; define measurable acceptance criteria for dimensions, leak resistance, lid fit, print accuracy and case count; then retain a repeatable approval record for each SKU.Cost ElementTypical BasisIllustrative CAD per MealCommon Canadian Buyer RiskPrimary containerSupplier unit price0.31Comparing materials with different performanceLid or closureMatched component price0.08Loose fit, leakage or separate sourcingSetup allocationTooling, plate or artwork cost ÷ planned units0.01Low volume absorbs too much fixed costFreight and receivingTotal inbound logistics ÷ units received0.04Ignoring port, drayage or domestic transferStorage and handlingMonthly carrying cost ÷ units issued0.02Bulky cases consume warehouse spaceWaste and defectsReplacement cost × expected loss rate0.02Underestimating line loss and damageObsolescence allowanceExpected write-off ÷ planned consumption0.01Menu, brand or regulation changesThis table illustrates why a quote should be reviewed as a cost stack. The actual values depend on order quantity, ship mode, origin, container nesting efficiency, warehouse location, seasonality and the food application. A salad bowl moving through Vancouver may have a different landed cost profile from a hot meal tray routed through Montréal or Halifax.The scope should cover every packaging item required to deliver one saleable meal in the condition promised to the customer. In Canada, this can include a primary food container, lid, seal, sleeve, tamper-evident label, sauce cup, cutlery pouch, napkin, thermal bag, corrugated outer carton and pallet-related allocation. A restaurant serving food for immediate dine-in consumption may use less secondary packaging than a ghost kitchen delivering across Calgary, Ottawa or Greater Vancouver.Separate packaging costs from food cost, labour and delivery-platform fees, but do not omit packaging activities that consume resources. If a fragile lid causes kitchen staff to double-bag orders, the extra bag is part of the packaging cost. If an outer carton is needed to prevent meal trays from crushing during last-mile handling, its cost belongs in the packaging model. This level of visibility is especially important for national chains and meal-kit businesses using multiple fulfillment hubs.Meal FormatPrimary PackagingSecondary Packaging Often RequiredCost Driver to MonitorHot takeaway bowlPaper bowl with lidCarry bag, lid seal, case linerHeat performance and lid securitySalad or poke bowlClear or paper bowl with lidTamper label, sauce cup, bagCondensation and visual presentationBurger comboBurger box and fry cartonBag, napkins, drink carrierGrease resistance and stackabilityPrepared meal subscriptionCompartment tray with film or lidInsulated shipper, gel packs, labelsCold-chain protection and cube utilizationBakery deliveryClamshell, tray or cake boxCorrugated shipper, divider, tapeBreakage and print finishCatering orderLarge tray with lidTransport carton, tamper seal, labelsLoad bearing and leak preventionThe purpose of this scope table is to prevent a misleading “container-only” number. Procurement should map packaging at the meal, order and shipment level. An individual rice bowl might require one bowl and lid, while a customer order of four bowls may also require one delivery bag, two condiment packs, a receipt label and a share of a corrugated transit carton.Canadian buyers face a wide range of operating conditions. Food-service operators in dense downtown Toronto or Vancouver locations may prioritize compact packaging and rapid replenishment because storage space is expensive. Regional distributors in Winnipeg, Edmonton or Saskatoon may focus more heavily on inventory cover, domestic transfer freight and seasonal lead-time protection. Businesses serving Northern communities may require larger safety stocks, making storage and obsolescence more material than the initial product quote.Policy and sustainability goals also affect scope. Packaging choices may be influenced by municipal waste requirements, customer expectations for fibre-based formats, retailer sustainability scorecards and evolving provincial extended producer responsibility programs. Buyers should assess the complete performance and documentation package for their intended market rather than assuming one material or claim fits every application.var ctxMarket = document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctxMarket, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Illustrative Canadian food-service packaging demand index', data: [100, 106, 112, 118, 125, 132], borderColor: 'rgb(35, 111, 73)', backgroundColor: 'rgba(35, 111, 73, 0.12)', borderWidth: 3, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, plugins: { legend: { display: true } }, scales: { y: { beginAtZero: false, title: { display: true, text: 'Demand index (2022 = 100)' } } } }});The line chart is an illustrative planning index rather than a market forecast. It shows why buyers should model scalable packaging costs: ongoing growth in delivery, prepared foods and convenience-led meals can magnify small per-unit cost errors across millions of meals.Fixed costs do not rise in direct proportion to every pack produced. They can include printing plates, cutting dies, mould adjustments, artwork preparation, colour matching, sample development and laboratory testing. Variable costs rise with volume and usually include paperboard, coatings, inks, forming, lids, packing materials and direct production labour. One-time costs are project-specific expenses that may be allocated across an agreed forecast quantity or treated as launch expenses.Allocation needs discipline. If a custom bowl project has CAD 3,000 in artwork, plate and setup charges and the first planned run is 300,000 units, the allocation is CAD 0.01 per unit. If the business expects only 30,000 usable units before redesigning the artwork, the effective allocation is CAD 0.10 per unit. The same quote can therefore have radically different economics at different volumes.Cost TypeExamplesAllocation MethodProcurement ActionFixed setup costPlates, dielines, tooling preparationSpread over forecast usable unitsNegotiate reuse rights and revision rulesVariable material costPaperboard, coating, ink, lid resinCost per unitCompare equivalent specificationsVariable conversion costPrinting, die-cutting, forming, packingCost per unit or caseConfirm tolerances and output capacityOne-time sampling costWhite sample, printed prototype, testingLaunch budget or unit allocationApprove before production commitmentOne-time logistics costSample courier, pilot shipment, urgent air freightProject cost or first-order allocationAvoid using emergency mode as baselineInventory carrying costWarehouse space, insurance, capital tie-upMonthly rate × average inventoryAlign MOQ with consumption rateThe table helps finance and operations teams avoid mixing timing categories. A setup charge paid once should not be ignored, but it should also not make a long-term supply program appear uneconomic if the asset can support repeat orders. Conversely, a “free tooling” offer may simply be recovered through higher unit pricing, a stricter minimum order quantity or less flexible artwork changes.Before releasing a purchase order, create a product approval record containing the product name, SKU, dimensions, capacity, paper grade or material structure, coating, lid reference, print artwork revision, Pantone targets where required, carton pack count, pallet pattern, acceptable defect level and food-use conditions. Include photos of approved samples and a clear statement of whether the pack is intended for hot, cold, greasy, wet or frozen food.For branded projects, digital proof, unprinted white sample and printed pre-production proof are different approval stages. Each stage answers a different question: artwork layout, structural fit and manufacturing colour or finish. Combining them into one informal approval can lead to expensive rework later.A pack is the individual packaging component, such as one bowl or one burger box. A meal is the complete packaging set needed for one menu item. A customer order is the group of meals and shared packaging sent to one destination. All three measures are useful, but they answer different questions.Cost per pack helps buyers compare components. Cost per meal supports menu engineering and gross-margin reporting. Cost per customer order helps delivery businesses account for shared bags, labels, drink carriers and delivery protection. A customer who orders three meals does not necessarily create three bag costs, so order-level allocation may reduce distortion.Cost per pack = Total landed cost of that SKU ÷ usable units received.Cost per meal = Sum of component cost per pack × quantity used per meal.Cost per customer order = Meal packaging total + shared order packaging + order-specific protection.Example ComponentQuantity per MealUsable Unit Cost (CAD)Extended Meal Cost (CAD)1,000 mL paper bowl10.310.31Ventilated lid10.080.08Sauce cup with lid10.060.06Tamper-evident label10.0250.025Napkin allocation20.010.02Paper carry bag allocation0.500.120.06Total packaging cost per meal——0.555This illustration shows that a meal may have CAD 0.555 in packaging before any order-level insulated shipper, box divider or third-party fulfillment handling is added. The percentage of meal revenue should then be reviewed. If a meal sells for CAD 14.99, packaging at CAD 0.555 represents approximately 3.7% of menu revenue before food, labour, rent and delivery costs.Different industries need different cost logic. Quick-service restaurants often prioritize speed, stackability and standardized ordering. University cafeterias and hospital food-service programs may prioritize portion consistency, food-contact documentation and dependable scheduled supply. Meal-prep operators need microwavable or reheatable formats where applicable, plus trays that hold up through refrigeration and last-mile movement. Grocery prepared-food departments typically focus on shelf presentation, tamper evidence, barcode label space and case-packing efficiency.For food trucks and event caterers, compact case dimensions and weather resistance can matter more than a minor unit-price difference. For e-commerce meal kits, packaging may need to survive parcel-network sorting, making corrugated protection, thermal materials and damage allowances central to the calculation.var ctxIndustry = document.getElementById('industryDemandChart').getContext('2d');new Chart(ctxIndustry, { type: 'bar', data: { labels: ['Quick service', 'Meal prep', 'Grocery prepared food', 'Catering', 'Coffee and bakery', 'Institutional foodservice'], datasets: [{ label: 'Illustrative annual packaging demand index', data: [88, 72, 79, 48, 61, 55], backgroundColor: ['#2f855a', '#3182ce', '#805ad5', '#dd6b20', '#d53f8c', '#718096'] }] }, options: { responsive: true, maintainAspectRatio: false, plugins: { legend: { display: true } }, scales: { y: { beginAtZero: true, title: { display: true, text: 'Demand index' } } } }});The bar chart illustrates how demand patterns can differ by industry. Buyers should not copy another segment’s packaging specification without checking the food temperature, hold time, delivery route, consumer handling and expected order frequency.Freight should be calculated from the supplier’s shipping terms through to the point where the packaging is usable in the Canadian operation. This can include origin handling, sea freight, insurance, destination terminal charges, customs brokerage, drayage, cross-docking and domestic transfer. For less-than-container-load shipments, the cost per unit can be much higher than for a well-utilized full container. Lightweight packaging is often freighted by volume rather than weight, so nesting efficiency and carton dimensions can materially influence landed cost.Storage must be converted into a per-unit cost. Use the average monthly inventory, warehouse cost, handling touches, insurance and working-capital charge. If a buyer stocks six months of printed cartons because the MOQ is high, capital is tied up and the risk of a menu or branding change increases. Packaging with a low purchase price can therefore become expensive if it occupies costly space in a Mississauga, Surrey or Montréal warehouse.Waste and failure allowances should include production-line loss, kitchen mishandling, transport damage, lid mismatch, leakage, crushed cartons, print defects and customer replacements. The allowance should be based on actual operations data where available. If the operation uses 102,000 bowls to serve 100,000 saleable meals, the practical usage loss is 2%. If an additional 1% is written off due to damage or quality failure, the total loss factor is 3%.Allowance CategorySuggested CalculationIllustrative RateControl MethodOcean and domestic freightTotal logistics spend ÷ units receivedCAD 0.025–0.070Improve container fill and route planningReceiving and warehouse handlingLabour and equipment ÷ units issuedCAD 0.005–0.020Standardize carton and pallet formatsStorage carrying costAverage inventory value × monthly carrying rateCAD 0.005–0.030Use forecast-based replenishmentKitchen wasteUnits discarded ÷ units issued1%–3%Train staff and improve dispensingSupplier defectsRejected units ÷ units received0.3%–1.5%Set acceptance criteria and inspectionsTransit damageDamaged units ÷ units shipped0.2%–1.0%Strengthen cases and pallet protectionObsolete stockExpected write-off ÷ annual usage0.5%–4%Limit custom inventory exposureThe ranges above are planning examples, not universal benchmarks. A proven, stable SKU with disciplined replenishment can achieve lower loss. A newly launched printed package with long lead times and variable sales can require a more conservative allowance. Review actual usage monthly and revise the model after each major product, menu or logistics change.Ask suppliers for carton dimensions, gross and net carton weight, units per carton, cartons per pallet, pallet height and estimated container loading quantity before choosing a supplier. Compare the number of usable meal sets per cubic metre, not merely the number of units per carton. A slightly higher unit-price tray that nests better may lower freight and warehouse cost enough to win on total economics.When importing through the Port of Vancouver, Port of Prince Rupert, Port of Montréal or Halifax, plan for inland transport to the final operating region. A supplier’s export quotation should be reconciled with the buyer’s broker, forwarder and warehouse data. For urgent launches, separate air-freight or courier samples from the normal replenishment model so an exceptional event does not hide the economics of the regular supply program.Ignoring secondary packaging and waste creates false gross-margin confidence. The error can be small on a single order but substantial across a chain. Consider a business serving 2 million meals annually. If the budget excludes CAD 0.07 per meal for bags, labels, corrugated allocation and loss, the annual shortfall is CAD 140,000. That gap can consume much of the benefit from negotiating a CAD 0.02 discount on the primary container.Secondary packaging also protects revenue. A sturdy outer carton can reduce crushed meal trays and customer credits. A tamper-evident seal can support order integrity. A compatible lid can reduce spills that result in refund costs, remakes, platform penalties and brand damage. The best packaging solution is not automatically the least expensive component; it is the one that delivers the lowest controllable cost for a reliably saleable meal.ScenarioQuoted Primary Pack CostHidden or Omitted CostsTrue Cost per MealAnnual Impact at 1M MealsQuote-only viewCAD 0.34None includedCAD 0.34CAD 340,000Add lid and bagCAD 0.34CAD 0.14CAD 0.48CAD 480,000Add freight and storageCAD 0.34CAD 0.18CAD 0.52CAD 520,000Add 3% wasteCAD 0.34CAD 0.20CAD 0.54CAD 540,000Add defects and creditsCAD 0.34CAD 0.23CAD 0.57CAD 570,000Optimized total-cost modelCAD 0.37CAD 0.15CAD 0.52CAD 520,000The final row demonstrates an important procurement insight: a CAD 0.37 primary pack can be better than a CAD 0.34 quote if it improves nesting, reduces breakage, eliminates double-bagging and lowers defects. This is the reason to test comparable products under actual meal conditions rather than choosing solely from a product photograph or price list.A meal-prep operator serving the Greater Toronto Area initially chose a lower-priced black plastic tray at CAD 0.29 per unit. The company later found that the trays required more protective outer packaging, had inconsistent lid fit across batches and increased replacement meals during courier delivery. After a structured review, the operator moved to a matched tray-and-lid system with a higher primary component cost but better case protection and clearer stock control. The result was a lower total packaging cost per order because loss, emergency purchases and customer credits declined.The lesson is not that one material is always better than another. The lesson is that each specification should be measured against the actual food, handling route and sales volume. A warm, sauce-heavy meal has different needs from a chilled salad or a dry bakery item.var ctxTrend = document.getElementById('trendShiftChart').getContext('2d');new Chart(ctxTrend, { type: 'line', data: { labels: ['2022', '2023', '2024', '2025', '2026', '2027'], datasets: [{ label: 'Share of total cost managed through unit-price focus', data: [72, 66, 59, 53, 47, 41], borderColor: 'rgb(214, 69, 65)', backgroundColor: 'rgba(214, 69, 65, 0.22)', fill: true, tension: 0.25 }, { label: 'Share managed through total landed-cost focus', data: [28, 34, 41, 47, 53, 59], borderColor: 'rgb(49, 130, 206)', backgroundColor: 'rgba(49, 130, 206, 0.16)', fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, plugins: { legend: { display: true } }, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Illustrative management focus (%)' } } } }});The area chart presents an illustrative trend toward total-cost management. By 2026 and beyond, more buyers are expected to evaluate packaging through logistics efficiency, product performance, compliance readiness, waste reduction and supplier reliability, rather than through a single ex-factory price.Scenario planning turns a packaging calculation into a procurement tool. At minimum, compare low, expected and high volume. Then test specification changes such as natural kraft versus printed white board, standard versus custom sizes, single-wall versus insulated formats, and local warehousing versus direct import. Consider lead time, expected inventory days, freight mode and expected demand variability.For a Canadian restaurant group, an annual forecast of 500,000 meals may justify a custom print run, while 50,000 meals may be better served by a stock item plus applied label. A fully printed package can improve brand presentation, but if a campaign runs for only two months, obsolete inventory risk can outweigh the marketing gain.ScenarioAnnual Usable VolumeSetup Cost per UnitFreight and Storage per UnitEstimated Total Cost per MealSmall pilot, standard stock50,000CAD 0.000CAD 0.085CAD 0.61Small pilot, custom print50,000CAD 0.060CAD 0.085CAD 0.69Regional launch250,000CAD 0.018CAD 0.055CAD 0.58Multi-city program750,000CAD 0.008CAD 0.042CAD 0.52National chain program2,000,000CAD 0.004CAD 0.033CAD 0.47High-volume scheduled release5,000,000CAD 0.002CAD 0.028CAD 0.43This scenario table explains why volume affects more than product price. Higher volume can reduce setup allocation and improve freight efficiency, but it can also increase exposure to obsolescence if purchasing outruns consumption. The best approach is often a scheduled-order arrangement: reserve manufacturing capacity or materials while releasing production and shipment in stages aligned with demand.Packaging cost models will increasingly include digital traceability, automated visual inspection, demand forecasting and more granular carbon or waste reporting. Buyers may ask for batch-level identification, documented material sourcing, improved recyclability guidance or compostability options suitable for a specific program. Smart production scheduling can reduce emergency freight, while better carton design can improve container utilization and lower the logistics cost per meal.Policy developments and customer expectations will continue to favour clearer material information and more responsible end-of-life planning. Canadian businesses should verify that claims, product documentation and disposal guidance are appropriate for their own province, municipality, food application and sales channel. Sustainable packaging should be evaluated for functional performance, availability, cost stability and actual recovery conditions—not only for appearance or marketing language.Once the complete per-meal cost is known, procurement can negotiate the drivers that matter most. If unit price is only 55% of total packaging cost, there is limited value in spending weeks negotiating a one-cent product reduction while ignoring freight, case configuration and defect controls. If setup is the main issue, negotiate tool amortization, plate reuse or a stock-format launch. If storage is the issue, negotiate staged shipments and practical minimum order quantities.Budgeting should include a base case, a downside case and a decision trigger. The base case uses expected volume and normal freight. The downside case uses lower consumption, a modest freight increase and a higher obsolescence factor. The trigger identifies when management should revisit the purchase plan, such as demand falling 20% below forecast or defect rates exceeding the agreed tolerance.Request comparable pricing for equivalent material, capacity, coating, print coverage and case count. Ask for carton dimensions and loading plans before comparing freight-sensitive products. Define defect handling, inspection process, evidence requirements and remedy timelines. Confirm lead time, production window, payment terms and scheduled release options. Set acceptance criteria for leak resistance, grease resistance, lid fit, print registration and compression strength. Review whether custom artwork remains usable if menus, logos or promotions change. Evaluate consolidation opportunities across cups, bowls, boxes, trays and compartment meal packaging. var ctxCompare = document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctxCompare, { type: 'bar', data: { labels: ['Quoted unit price', 'Freight efficiency', 'Quality control', 'Customization support', 'Documentation readiness', 'Scheduled supply'], datasets: [{ label: 'Supplier A: quote-focused score', data: [92, 55, 62, 48, 58, 50], backgroundColor: 'rgba(214, 69, 65, 0.72)' }, { label: 'Supplier B: total-cost score', data: [82, 83, 88, 86, 90, 84], backgroundColor: 'rgba(35, 111, 73, 0.72)' }] }, options: { responsive: true, maintainAspectRatio: false, plugins: { legend: { display: true } }, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Illustrative score out of 100' } } } }});This comparison chart is an example of a weighted supplier evaluation. Supplier A appears stronger on quoted unit price, while Supplier B performs better on the broader contributors to reliable total cost. Each buyer should set its own weighting based on application risk, annual spend, delivery locations and brand requirements.Fude Packaging supports overseas B2B buyers with food-service packaging across cups, bowls, boxes, trays, burger packaging, kraft lunch boxes, salad containers, noodle boxes and multi-compartment meal formats. The goal is to help buyers compare more than a single unit quote by aligning manufacturing capability with product performance, branding needs and logistics requirements.With an in-house laboratory and process controls covering material selection, printing, forming, inspection and packing, Fude Packaging can support structured product validation for commercial packaging programs. Buyers can use digital artwork proofing, white samples and printed pre-production samples to check dimensions, capacity, structure, lid compatibility, print placement and food-use suitability before approving mass production.For projects requiring food-contact documentation or chain-specific quality review, the team can discuss available BRC, FSC, ISO 9001, LFGB and FDA-related documentation based on product selection and destination-market requirements. Batch traceability and defined inspection steps help procurement teams maintain an approval trail from sample through shipment.Fude Packaging has more than 20 years of packaging experience and operates from a self-owned 30,000 m² production base in Shandong. Automated capacity can reach up to 120,000 units per day, depending on product specifications and production planning. In-house manufacturing across multiple categories can help Canadian importers consolidate suppliers, coordinate branding and improve container utilization when purchasing related packaging items together.For operators managing recurring demand, scalable production is valuable only when it is paired with consistent quality. Material inspection, production monitoring, final checks and batch verification are designed to support repeatable output. Buyers can also arrange independent third-party inspection where appropriate for their procurement process.Fude Packaging provides OEM and ODM support that can include material recommendations, structural development, custom sizes, artwork and dieline review, Pantone colour matching, sampling, export packing and shipment coordination. Standard production lead times can be approximately 7–15 days, subject to design complexity, production schedule and order quantity. Scheduled-order support can help distributors and multi-location operators balance MOQ efficiency with inventory risk.Canadian buyers can explore available formats through the food packaging product range, review customization and project support through the packaging services page, learn more about production background on the Fude Packaging company profile, or request a specification review through the contact team.Include every packaging item and activity needed to deliver one saleable meal: primary container, lid, labels, bags, inserts, secondary packaging, freight, receiving, storage, handling, waste, defects, returns and expected obsolete inventory. If the meal requires a component for safe delivery or customer presentation, it should be part of the model.Allocate one-time costs across the expected number of usable units during the period in which the design will remain active. For example, divide tooling, plates and artwork preparation by the forecast quantity before the next brand, menu or specification change. Use a conservative volume estimate if demand is uncertain.Divide total freight, destination handling and domestic transfer costs by usable units received. For storage, calculate monthly warehouse, handling, insurance and carrying costs, then divide by units issued during the same period. Use carton dimensions and occupancy data because bulky packaging can have a high cube cost even when it is lightweight.Use historical operational data where possible. Multiply the relevant packaging cost by the expected loss percentage, or divide total cost by usable units rather than purchased units. Track kitchen waste, transit damage, supplier rejects and customer replacement events separately so corrective action can target the real cause.Compare at least low, expected and high volume; standard versus custom specification; full-container versus less-than-container freight; direct import versus local stock; and normal versus disruption-level waste. Management should also compare a low quoted-price option against a higher-performing option that may reduce damage, double packing, refunds and obsolete inventory.A disciplined per-meal packaging cost model gives Canadian operators a clearer basis for menu pricing, sourcing decisions, supplier negotiations and inventory planning. The most useful result is not a single static number; it is a repeatable method that reveals where cost, risk and performance truly sit.