Global Market Multi-SKU Food Packaging Supplier Guide
Quick Answer — How to Qualify a Multi-SKU Food Packaging Supplier

When evaluating a multi-SKU food packaging supplier for the Global market, buyers should request evidence that the factory can manufacture the exact food-contact products, materials, sizes, coatings, print designs, and order quantities required. A supplier may produce paper cups successfully but lack suitable forming tools, leak-testing methods, lid-matching capability, or quality controls for noodle boxes, salad bowls, burger boxes, or compartment meal trays.
The most reliable qualification method combines document review, factory capability verification, product-specific sampling, measurable quality limits, production-capacity validation, and a corrective-action process. Buyers should not approve a factory based only on catalog photos, certificates, or a low quotation. Instead, confirm the supplier’s equipment list, material specifications, traceability records, laboratory testing, inspection procedures, delivery performance, and response to non-conforming products.
For international buyers, the goal is not simply to find the lowest quoted factory price. It is to reduce total procurement risk across multiple packaging categories. A qualified supplier should help consolidate purchasing, standardize quality, coordinate artwork, improve shipment utilization, and provide compliance documents suitable for the destination market.
| Qualification Area | What Buyers Should Verify | Practical Evidence | Acceptance Measure |
|---|---|---|---|
| Product scope | Exact packaging types and sizes | Specification sheet, dieline, samples | Dimensions match approved drawing |
| Food-contact control | Material, coating, ink, adhesive suitability | Declarations, test reports, supplier records | Documents match destination market |
| Factory equipment | Printing, die-cutting, forming and packing lines | Equipment list, videos, audit observations | Correct equipment for each SKU |
| Quality management | Incoming, in-process and final inspection | Inspection records and quality plan | Defined AQL or agreed defect limits |
| Traceability | Lot identification from paper to shipment | Batch cards, warehouse records, carton labels | Lot can be traced within one working day |
| Capacity | Available output during peak periods | Production plan, shift record, order history | Confirmed allocation before purchase order |
| Corrective action | Response to quality or shipment claims | CAPA report, replacement procedure | Root cause and action deadline defined |
The table above should become the basis of a buyer’s supplier-approval file. Evidence should be SKU-specific. For example, proof of paper-cup production does not automatically verify a supplier’s ability to make grease-resistant burger boxes or leak-resistant paper bowls.
Multi-SKU Packaging: Product Scope

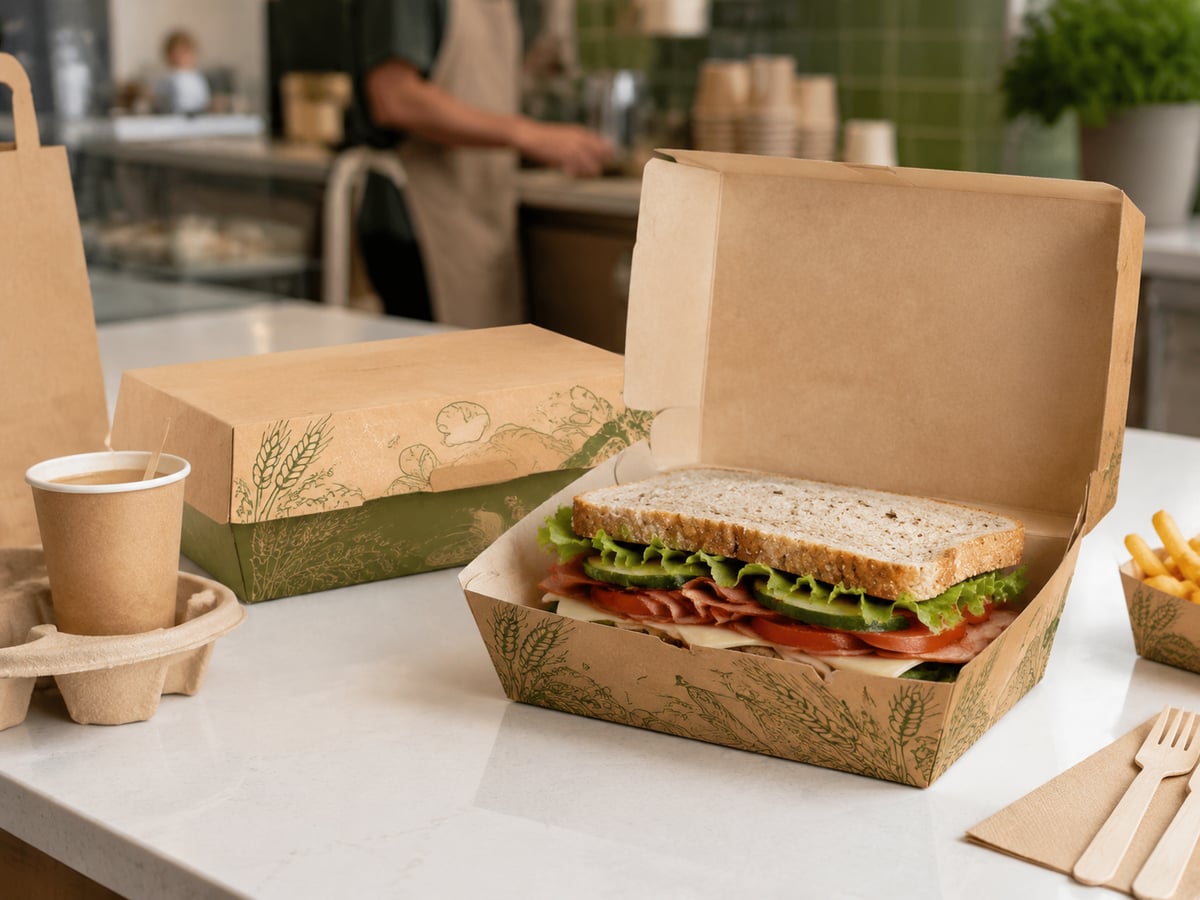
Multi-SKU food packaging means sourcing several packaging categories from one coordinated manufacturer or supplier. Typical programs include hot-drink cups, cold-drink cups, paper bowls, soup containers, lunch boxes, salad containers, trays, burger boxes, noodle boxes, lids, sleeves, and branded outer cartons. These programs are common for restaurant chains, distributors, ghost kitchens, catering companies, airline-food providers, retailers, and takeaway platforms.
In the Global market, buyers should define the product scope before comparing factories. The specification must state the food type, serving temperature, fill level, contact duration, transportation conditions, microwave requirement if applicable, grease exposure, moisture exposure, stacking requirement, closure system, branding requirement, and disposal objective. Without this information, factories may quote visually similar products built with different paper grades, coatings, grammage, or structural strength.
For example, a 750 ml salad bowl may require a different board grade and lid fit from a 750 ml hot noodle bowl. A burger box for dry products may perform differently from one intended for fries, sauces, and delivery transport. The buyer should define the actual application rather than purchasing only by nominal size.
| Packaging Category | Typical Application | Critical Performance Requirement | Common Buyer Error |
|---|---|---|---|
| Paper cups | Coffee, tea, juice, soft drinks | Leak resistance, rim strength, lid fit | Approving a cup without testing the matching lid |
| Paper bowls | Soup, noodles, rice, salads | Heat performance, seam integrity, stacking | Using one board grade for all food temperatures |
| Kraft lunch boxes | Meals, bakery products, takeaway | Grease resistance and fold strength | Ignoring sauce or condensation exposure |
| Burger boxes | Burgers, fries, sandwiches | Compression resistance and ventilation | Testing only empty boxes |
| Salad containers | Fresh produce, grain bowls | Lid security and moisture tolerance | Not testing refrigerated delivery use |
| Noodle boxes | Asian noodles, rice, stir-fry | Leak prevention and handle strength | Ignoring oil and hot-food contact |
| Food trays | Snacks, bakery, fast food | Rigidity and grease resistance | Assuming all kraft trays are food-contact equal |
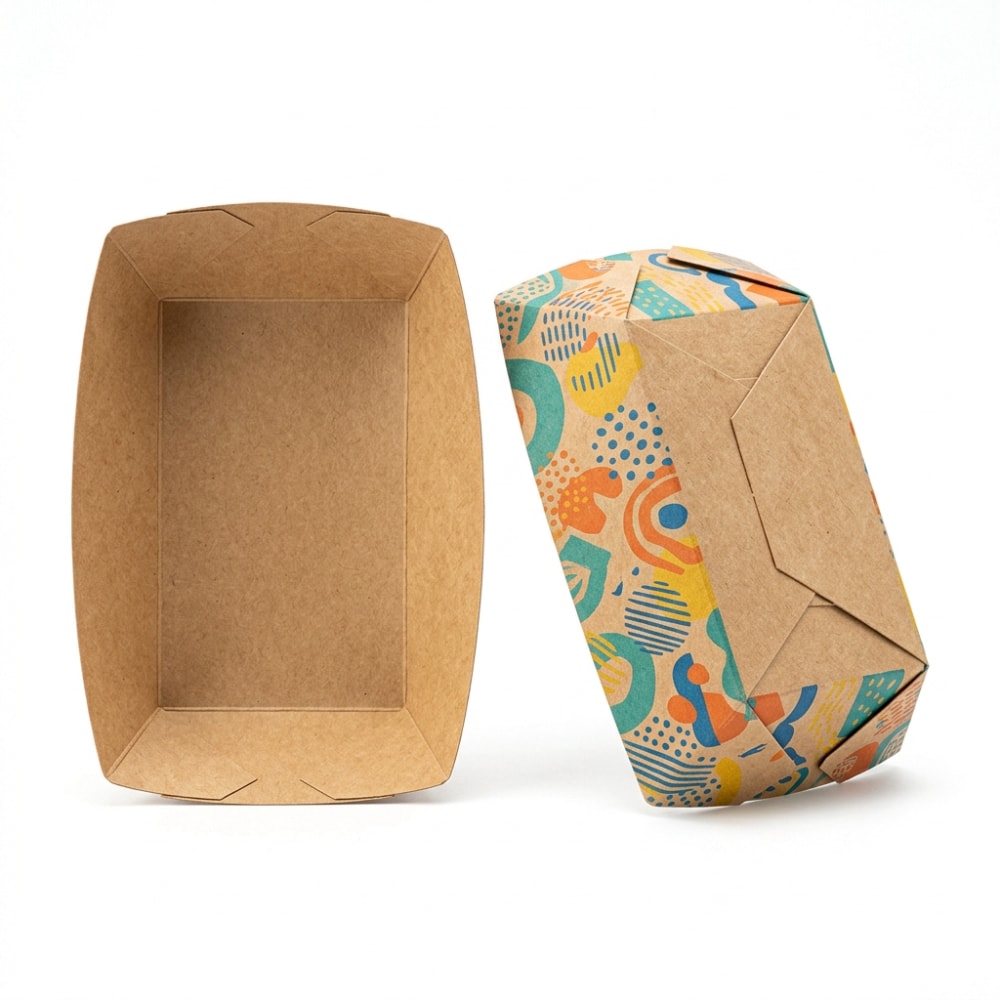
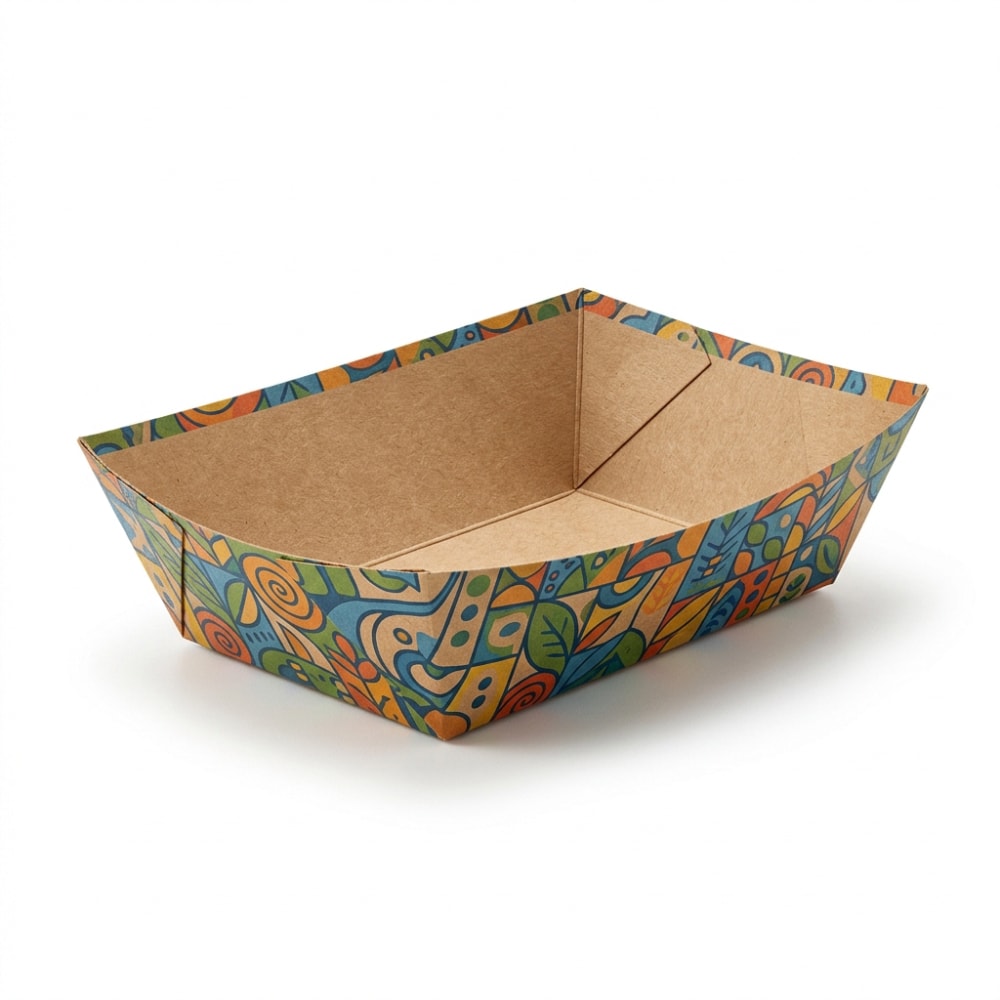
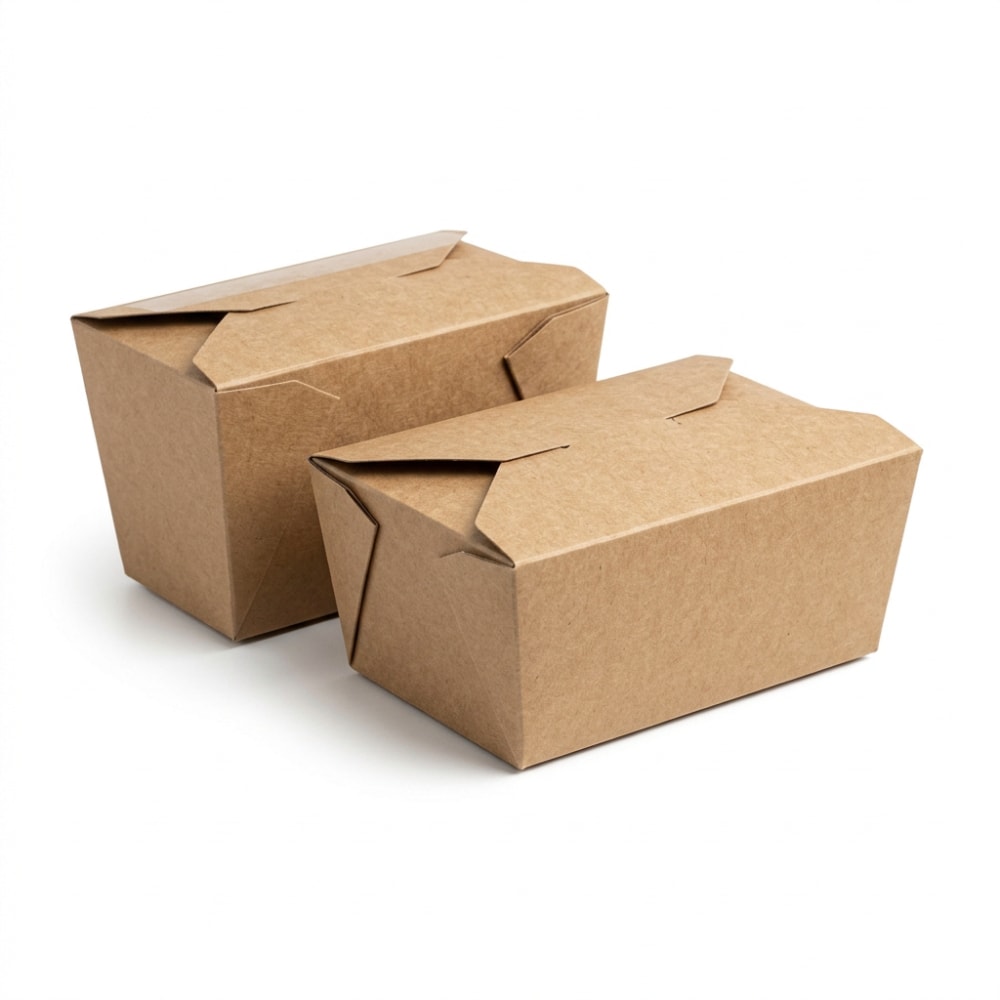
Buyers can review Fude Packaging’s available food containers when developing a multi-category procurement list. A complete product matrix helps purchasing teams identify which sizes can share lid systems, cartons, print colors, pallet formats, and shipping plans.
Global demand for consolidated packaging sourcing continues to rise because food-service brands need consistent packaging in multiple locations. Importers serving London, Dubai, Los Angeles, Sydney, Singapore, Rotterdam, Jeddah, and Hamburg increasingly prefer fewer supplier relationships, provided the factory can maintain category-specific quality controls.
The line chart illustrates an indexed planning trend rather than a guarantee of future market volume. Growth is supported by takeaway food consumption, restaurant-chain expansion, private-label retail, demand for branded packaging, and supplier-consolidation programs.
Multi-SKU Packaging: Factory Equipment

Equipment verification should focus on the manufacturing route for every important SKU. A multi-SKU supplier should be able to explain how paper is received, stored, printed, coated or converted, die-cut, formed, inspected, packed, and prepared for export. Buyers should also distinguish between in-house production and outsourced items. Outsourced products are not automatically unacceptable, but the supplier must disclose the arrangement and show how quality, traceability, and delivery responsibility are controlled.
For paper food packaging, relevant equipment may include flexographic or offset printing machines, laminating or coating equipment, die-cutting machines, paper cup forming machines, bowl forming machines, automatic lunch-box forming lines, inspection systems, packing machines, palletizing areas, and laboratory instruments. The required line configuration depends on the product construction.
During a remote or onsite audit, buyers should ask for machine model, line quantity, typical output rate, maintenance plan, changeover process, operator training records, rejection records, and examples of the same or comparable product. A factory that can run a high volume of standard white cups may have lower efficiency when producing several customized printed SKUs with frequent artwork changes.
| Equipment or Control | Relevant Product Types | Audit Question | Useful Record |
|---|---|---|---|
| Printing line | Branded cups, bowls, boxes | How is color approved and monitored? | Color standard, print inspection sheet |
| Die-cutting machine | Boxes, trays, sleeves, lids | How are cut accuracy and tool wear checked? | Die maintenance and first-piece record |
| Cup forming machine | Hot and cold paper cups | How are bottom and side seams verified? | Leak-test and hourly inspection record |
| Bowl forming machine | Soup, noodle and salad bowls | Can it run required diameter and height? | Machine setup and sample test report |
| Box forming line | Burger and meal boxes | How is fold consistency controlled? | In-process dimensional check |
| Laboratory equipment | All food-contact packaging | Which performance tests are conducted? | Test method and dated report |
| Automated packing line | High-volume export programs | How is SKU mixing prevented? | Carton label and packing verification |
Fude Packaging operates from a self-owned approximately 30,000 m² factory in Shandong, China, a region connected to established paper and packaging supply networks. Its technological capabilities include automated production lines, in-house printing and forming processes, product development support, and laboratory-based performance testing. For buyers shipping through Qingdao Port, Ningbo-Zhoushan Port, Shanghai Port, or Shenzhen’s Yantian Port, integrated factory control can help reduce coordination gaps between multiple subcontractors.
Equipment proof should be linked to performance proof. A video of a production line is useful, but it is not equivalent to a passed sample trial, a machine capability review, or a documented inspection result.
Multi-SKU Packaging: MOQ and Price Drivers
Minimum order quantity is influenced by more than the number of finished pieces. In multi-SKU packaging programs, MOQ and price are affected by board grade, coating type, cup or bowl diameter, print coverage, Pantone color requirements, die-cutting tools, lid compatibility, packing configuration, freight terms, destination, and whether the order combines standard items with custom artwork.
Buyers should ask suppliers to separate one-time costs from recurring unit costs. Tooling, plates, artwork preparation, prototype development, special carton printing, and custom molds may affect the first order. Recurring pricing should identify the base material, conversion cost, printing cost, packing cost, inspection level, and applicable delivery terms such as EXW, FOB, CIF, or DDP where available.
| Price Driver | Effect on Cost | How Buyers Can Manage It | Risk if Ignored |
|---|---|---|---|
| Paper grammage | Higher material cost and strength | Specify needed performance, not excessive weight | Weak containers or unnecessary overspending |
| Coating system | Changes material and processing cost | Match coating to food and disposal requirement | Leakage or compliance mismatch |
| Print colors | More colors increase setup complexity | Use controlled color standards | Brand inconsistency between batches |
| Custom size | May require tooling or mold cost | Consider standard dimensions where practical | High MOQ and slower replenishment |
| Order mix | Many small SKUs reduce line efficiency | Forecast annual demand by SKU | Frequent changeovers and unstable price |
| Export packing | Stronger cartons increase cost | Define carton drop and humidity needs | Transit damage and mixed cartons |
| Freight utilization | Container loading affects landed cost | Optimize carton dimensions and SKU mix | Paying freight for unused volume |
The most useful quote comparison is landed-cost comparison, not unit-price comparison. A lower-priced supplier may create higher total cost through poor carton utilization, inconsistent print, short shipments, rejected goods, delayed containers, or separate purchases from several factories.
Multi-SKU Packaging: Samples and Quality Limits
A product-specific sample trial should represent the final commercial configuration as closely as possible. Buyers should request white samples for structural review, printed samples for artwork and color review, and functional samples for food application testing. For high-risk products, samples should be tested with the actual food, sauce, oil, beverage, temperature, lid, transport route, and holding time expected in use.
Define measurable acceptance criteria before samples are approved. Terms such as “good quality,” “no leakage,” or “nice printing” are too subjective for international purchasing. Instead, define dimensions with tolerances, sample size, test duration, permitted visual defects, print color references, leak-test conditions, carton requirements, and the acceptable quality level for mass production.
| Sample Test | Recommended Method | Typical Acceptance Criterion | Applicable Products |
|---|---|---|---|
| Dimension check | Measure diameter, height, width and depth | Within agreed drawing tolerance | All SKUs |
| Leak test | Fill with hot or cold liquid for set time | No visible seam or bottom leakage | Cups, bowls, noodle boxes |
| Grease test | Hold oily food or simulant | No unacceptable oil strike-through | Burger boxes, trays, lunch boxes |
| Lid fit test | Apply, remove, invert and transport | Lid remains secure under agreed conditions | Cups, bowls, salad containers |
| Compression test | Stack filled or simulated packs | No collapse during defined stacking period | Boxes, bowls, trays |
| Print inspection | Compare against approved artwork and color | Legible print with no critical misregistration | Custom printed products |
| Odor review | Evaluate clean empty package | No abnormal or objectionable odor | All food-contact packaging |
Quality limits should also distinguish critical, major, and minor defects. Critical defects can affect food safety, function, or legal labeling. Major defects can prevent normal use, such as leaking cups, crushed bowls, incorrect print, or incorrect size. Minor defects may be cosmetic but should still have limits.
Buyers sourcing paper bowls should test filled products at the actual service temperature, including lid fit and delivery vibration. The same principle applies to branded paper cups, where rim quality, seam integrity, and lid compatibility must be approved together.
The bar chart highlights industries where multi-SKU packaging control is particularly important. Restaurant chains and distributors often require the strongest consistency because their packaging is used across many outlets, menu items, and geographic locations.
Multi-SKU Packaging: Compliance Documents
Compliance documentation should match the destination market, material structure, and intended food-contact use. Buyers should ask what the document covers, which production material it applies to, the issue date, the testing scope, and whether the report relates to the actual product or only a generic raw material. A certificate alone is not enough if the final product includes printing inks, adhesives, coatings, or components not covered by the document.
Common requirements may involve FDA-related food-contact expectations for the United States, EC 1935/2004 for the European Union, applicable national rules in the United Kingdom, Gulf market import requirements, Australian and New Zealand food-contact expectations, or country-specific declarations. Sustainability claims must also be verified carefully. FSC material claims, BPI compostability, OK Compost certification, recyclable claims, and plastic-reduction claims should be used only where the relevant product and certification scope support them.
| Document Type | Why It Matters | Buyer Verification Point | Review Frequency |
|---|---|---|---|
| Food-contact declaration | Confirms suitability statement | Check product, material and market scope | Each new product or material change |
| Migration or material test report | Supports food-contact assessment | Confirm tested structure and conditions | Based on validity and customer policy |
| FSC documentation | Supports responsible fiber sourcing claims | Verify certificate status and claim wording | Annual certificate review |
| ISO 9001 record | Shows quality-management framework | Check issuer, scope and validity | Annual certificate review |
| Compostability certificate | Supports approved compostability claims | Verify exact product and coating coverage | Before each claim or product launch |
| Ink and adhesive statement | Assesses converted product components | Confirm intended food-contact configuration | When artwork or material changes |
| Shipment inspection report | Verifies released order condition | Match PO, quantity, cartons and defects | Each shipment |
Documentation should be stored in a controlled supplier file. Procurement, quality, regulatory, and marketing teams should work from the same approved version. This helps prevent a marketing claim from being printed before its certification scope has been checked.
Multi-SKU Packaging: Capacity and Lead Time
Real capacity is verified through evidence, not claimed daily output alone. Ask the supplier for historical production data, current order loading, planned maintenance dates, shift pattern, line allocation, raw-material stock, production calendar, and peak-season commitments. Capacity should be assessed separately for each product family because cup lines, bowl lines, printing lines, and box-forming lines may be different bottlenecks.
A factory may state that it produces 120,000 units per day, but buyers should clarify whether this is total theoretical output, practical average output, or available capacity after existing orders. They should also ask whether the figure applies to simple white products, customized printed SKUs, or the exact combination required.
Fude Packaging reports automated production capability of up to approximately 120,000 units per day, subject to product structure, specifications, printing requirements, and order mix. Standard production orders can generally be scheduled within approximately 7–15 days when materials, artwork, capacity, and payment conditions are confirmed. For large seasonal programs, buyers should reserve capacity earlier and agree to rolling forecasts.
The area chart reflects a directional sourcing trend: buyers are increasingly requesting verified fiber-based options, lower-plastic structures, compostability-ready products where suitable infrastructure exists, and clearer material declarations. Requirements vary by country, waste-management system, and product application, so sustainability claims should remain precise.
For container shipments, buyers should also consider port routing and lead-time risk. Qingdao and Shanghai are major export gateways for northern and eastern China production; Rotterdam, Hamburg, Long Beach, Los Angeles, Jebel Ali, Singapore, and Sydney are important receiving hubs for many Global market programs. Allow time for vessel schedules, port congestion, customs clearance, local delivery, and safety stock.
Multi-SKU Packaging: Supplier Scorecard
After initial qualification, supplier management should continue through a scorecard. The scorecard converts supplier performance into measurable indicators and helps buyers identify whether issues are isolated or systemic. Review monthly for high-volume programs and quarterly for smaller programs.
| KPI | Measurement Method | Suggested Target | Corrective Action Trigger |
|---|---|---|---|
| On-time delivery | Orders shipped by confirmed date | 95% or above | Below target for two review periods |
| Accepted quality rate | Shipments passing agreed inspection | 98% or above | Repeated major defects |
| Claim response time | Initial response after issue notification | Within 24–48 hours | Late response or missing investigation |
| Corrective action closure | CAPA completed by agreed deadline | 90% or above | Overdue action or recurring root cause |
| Artwork accuracy | Approved design versus shipped product | 100% critical-content accuracy | Any regulatory or brand-critical error |
| Quantity accuracy | Shipped quantity versus purchase order | Within agreed tolerance | Shortage affecting customer supply |
| Document completeness | Required files received before shipment | 100% | Missing compliance or customs document |
A strong supplier scorecard does not replace collaboration. It creates a factual basis for improvement discussions. When a defect occurs, buyers should require containment action, root-cause analysis, corrective action, verification of effectiveness, and a preventive step for future orders.
The comparison chart is an illustrative evaluation model. Buyers should replace the example values with their own audit scores, evidence grades, and commercial priorities. A distributor may prioritize lead-time flexibility, while a restaurant chain may assign more weight to brand consistency and product performance.
Our Company: Fude Packaging for Multi-SKU Packaging
Fude Packaging supports overseas B2B buyers who want to consolidate several paper food-packaging categories under one manufacturing partner. The company serves importers, restaurant groups, distributors, food brands, retailers, and takeaway operators across more than 50 countries and six continents.
From a manufacturing capability perspective, Fude Packaging produces core categories in-house, including paper cups, paper bowls, food containers, burger boxes, kraft lunch boxes, salad containers, noodle boxes, food trays, and multi-compartment meal boxes. Centralized manufacturing can help customers coordinate packaging specifications, batch consistency, export packing, and container loading across several related SKUs.
From a technological capability perspective, the company combines automated production lines with in-house quality checks and laboratory performance testing. Incoming materials, production processes, finished goods, and batch identification can be reviewed through defined inspection stages. Buyers may also arrange independent pre-shipment inspections or third-party laboratory verification where required.
From a service capability perspective, Fude Packaging provides OEM and ODM support covering product selection, structural recommendations, coating and material recommendations, artwork and dieline review, Pantone-oriented color matching, prototype development, functional sampling, mass-production coordination, and export documentation. The international team can support T/T and L/C arrangements, sea freight, air freight, LCL, FCL, and express sample shipments.
For Global market projects, the practical approach is to start with a SKU matrix and annual demand forecast. This lets the supplier recommend common materials, compatible lids, efficient carton formats, staged sample approval, and a replenishment plan that is suitable for the buyer’s sales regions and delivery calendar.
FAQ — Multi-SKU Food Packaging Supplier Qualification
1. How should buyers verify a multi-SKU food packaging supplier?
Buyers should verify the supplier through a structured process: confirm product scope, review equipment and factory records, inspect food-contact documentation, approve product-specific samples, define quality limits, assess available capacity, and establish post-approval KPIs. A remote audit can be useful, but high-volume or high-risk programs may also justify an onsite audit or third-party inspection.
2. Which factory records prove production capability?
Useful records include equipment lists, machine maintenance plans, production schedules, shift records, historical order output, first-piece inspection sheets, in-process inspection records, final inspection reports, warehouse batch records, packing lists, and shipment documents. Buyers should request records that relate to the product category being sourced rather than relying only on general factory presentations.
3. What should a product-specific sample trial include?
A sample trial should include dimensional review, material confirmation, artwork approval, functional testing, packing evaluation, and actual food-use testing where possible. For hot-food containers, test heat, condensation, leakage, grease resistance, lid fit, and transport performance. For printed products, compare the sample against approved artwork and agreed brand-color standards.
4. How is real capacity verified before a peak season?
Verify real capacity by reviewing the supplier’s current order load, production calendar, line allocation, raw-material availability, staffing plan, maintenance schedule, and confirmed capacity reservation. Ask for available capacity by product family, not only total factory output. A written forecast and rolling order plan are especially important before Ramadan, year-end holidays, major retail promotions, summer beverage peaks, or restaurant launches.
5. Which supplier KPIs matter after approval?
The most useful KPIs are on-time delivery, accepted quality rate, claim response time, corrective-action closure rate, artwork accuracy, quantity accuracy, documentation completeness, and communication speed. Buyers should also monitor recurring defect types, freight damage, carton consistency, and the supplier’s ability to react to forecast changes.
6. Should buyers use one supplier for every packaging SKU?
One supplier can simplify procurement, quality control, and logistics, but only if the supplier has verified capability for each important category. Strategic buyers may use one primary multi-SKU manufacturer plus an approved backup source for critical items. The decision should balance cost, risk, capacity, product specialization, and regional service needs.
7. What are the main 2026 trends in food packaging sourcing?
Key 2026 trends include increased use of automation for inspection and production planning, stronger traceability expectations, more detailed food-contact documentation, lower-plastic and fiber-based material development, demand for verified sustainability claims, digital artwork approval, and improved supply-chain visibility. Policy developments will continue to vary by market, so buyers should verify local packaging, waste, labeling, and food-contact requirements before product launch.
About the Author
Fude Packaging is a professional flexible packaging manufacturer serving global food brands, wholesalers, and distributors. Our team shares practical insights on custom packaging, printing technology, food-safe materials, and industry trends to help businesses build better packaging solutions.
Share
Product Category
Start Your Project With Fude Today
Related Post
-

United States Paper Food Container Distribution Guide
The United States food service sector continues to shift toward practical, brandable, and more sustainable takeaway packaging. For restaurants, deli chains, caterers, wholesalers, and regional importers, choosing the right paper food containers distributor is no longer only about unit cost. It now involves coating choice, container strength, lid fit, compliance, print quality, freight timing, and the ability to serve multiple use cases from hot soups to salad bowls and compartment meal boxes. A reliable distributor or factory-direct partner can reduce procurement risk, support private label growth, and help operators meet changing customer expectations in markets such as New York, Los Angeles, Chicago, Houston, Miami, Seattle, and Atlanta.In the United States, demand is especially strong in urban delivery corridors near major logistics hubs and ports such as Los Angeles/Long Beach, New York/New Jersey, Savannah, Houston, and Seattle-Tacoma. Buyers want containers that travel well, resist leaks, maintain food presentation, and fit the economics of takeout and delivery platforms. At the same time, municipal compostability rules, state-level packaging scrutiny, and consumer attention to material choices are pushing buyers to compare PE-lined and PLA-lined paper packaging more carefully than before.This guide explains the market outlook, product ranges, coating options, scale manufacturing, certification expectations, pricing factors, and sourcing advice for buyers looking for a dependable paper food packaging supply partner in the United States.If you need a dependable paper food containers distributor for the United States, focus on five priorities: food-contact compliance, product range, coating suitability, reliable production capacity, and customization support. The best suppliers can provide kraft and white paper bowls, lunch boxes, noodle containers, trays, fry cups, deli boxes, and compartment meal boxes with matching lids in multiple capacities. They should also support FDA-compliant materials, provide clear documentation, offer both PE and PLA coating options, and maintain stable lead times for recurring wholesale orders.For most U.S. buyers, kraft and white paper containers remain the most versatile choice for takeout, delivery, fast casual, and prepared foods. PE-coated options generally offer strong leak and grease resistance at a lower cost, while PLA-coated options are often selected for compostable programs and environmentally positioned brands. The right distributor should not only sell containers, but also guide you on substrate thickness, lid compatibility, stacking, carton configuration, print design, and freight planning for your sales channels.Factory-direct sourcing has become more attractive for importers and large distributors because it can improve pricing consistency and widen SKU availability. Buyers seeking scale often prefer partners with integrated forming, printing, die-cutting, testing, and warehousing. This shortens communication loops and makes it easier to control brand color, structural performance, and repeat-order quality.Buyer NeedWhat to CheckWhy It MattersTypical U.S. Use CaseRecommended OptionRisk If IgnoredLeak resistanceCoating type and sealing qualityPrevents spills in deliverySoup, noodles, sauced mealsPE or PLA lined bowl/boxCustomer complaints and refundsBrandingPrinting capabilitySupports shelf appeal and loyaltyCafes and regional chainsCustom flexo printingGeneric packaging lookComplianceFDA and other certificatesReduces import and sales riskNationwide wholesaleDocumented food-contact complianceCustoms or client rejectionSustainability positioningMaterial and compostable statusImportant for eco-conscious marketsWest Coast and college townsPLA or certified compostable linesBrand mismatch with policy goalsSKU flexibilityRange of sizes and lidsSimplifies supplier baseMulti-location food groupsOne-stop product lineHigher purchasing complexityLead time stabilityProduction and warehousing capacityHelps maintain inventory flowDistributors and importersSupplier with scale productionStockouts and lost salesThe table above shows why U.S. packaging buyers increasingly evaluate suppliers beyond price alone. A container that saves a fraction of a cent but leaks, collapses, or lacks proper documentation usually costs more over time.By 2026, the United States market for paper food containers is expected to expand further as delivery, grab-and-go retail meals, convenience dining, and eco-oriented packaging continue to grow. Several forces are driving demand. First, restaurant and grocery prepared-food formats increasingly depend on disposable packaging that can handle temperature changes, transit stress, and visual presentation. Second, many municipalities and institutional buyers are reevaluating plastic-heavy packaging. Third, chain operators and wholesalers are consolidating purchasing toward suppliers that can standardize packaging across multiple regions.The strongest growth areas are likely to be salad bowls, soup bowls, lunch boxes, compartment containers, and paper cups with compatible lids. Growth is not limited to restaurant corridors in Manhattan, Brooklyn, downtown Chicago, or Los Angeles County. It also extends to suburban delivery kitchens, airport concession programs, university dining, sports venues, and large grocery prepared-food departments in Texas, Florida, Georgia, and the Midwest.In practical terms, demand in 2026 will be shaped by three trends: operational efficiency, sustainability pressure, and visual branding. Operators want containers that stack neatly, seal consistently, and reduce rework in busy kitchens. Sustainability pressure is pushing requests for recyclable fiber content, responsibly sourced paper, and compostable lines where feasible. Visual branding is driving custom-printed cups, kraft bowls with clean logo applications, and premium window-lid boxes for deli and dessert presentations.var ctxMarket = document.getElementById('lineChartMarket').getContext('2d');var chartMarket = new Chart(ctxMarket, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026'],datasets: [{label: 'Estimated U.S. Paper Food Container Demand Index',data: [78, 84, 91, 99, 108],borderColor: 'rgb(75, 192, 192)',backgroundColor: 'rgba(75, 192, 192, 0.15)',fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart illustrates a realistic demand index trajectory rather than a fixed market value, showing the broad expansion expected through 2026. This pattern reflects continued growth in takeaway and prepared-food consumption, especially in dense urban regions and fast-growing Sun Belt metros.Demand Driver2024 Impact2025 Direction2026 OutlookMain U.S. RegionsPackaging EffectFood delivery growthHighHighVery highCalifornia, New York, TexasMore leak-proof bowls and boxesPrepared grocery mealsMediumHighHighFlorida, Illinois, GeorgiaWindow-lid deli and meal boxesCampus dining changesMediumMediumHighMassachusetts, Michigan, North CarolinaCompostable and branded containersQuick-service expansionHighHighHighNationwideFries cups, drink cups, combo boxesLocal packaging regulationMediumHighHighWest Coast, NortheastHigher PLA and certified linesPrivate label food brandsMediumHighHighMajor metro areasCustom print demand risesThe table shows that 2026 demand is not based on a single factor. Rather, it reflects a convergence of food delivery economics, sustainability policy, and retail-ready meal packaging. Suppliers that serve the United States effectively will need the flexibility to support both high-volume commodity SKUs and specialized branded programs.Product range matters because U.S. buyers often want to reduce the number of vendors they manage. A distributor with a full catalog can supply bowls, paper cups, food trays, lunch boxes, noodle containers, fry cups, deli boxes, bento-style boxes, and matching lids in coordinated carton quantities. This simplifies inventory planning for restaurant groups and wholesalers serving different food categories.Typical capacities commonly requested in the United States include small deli sizes such as 500 ml, 650 ml, and 750 ml; medium meal sizes such as 800 ml and 1000 ml; and bowl capacities spanning 8 oz to 40 oz depending on the menu. Cups are usually stocked from 4 oz to 32 oz. For restaurant and meal-prep applications, multi-compartment paper boxes are increasingly important because they allow portion control and keep sauces, proteins, and sides more organized during transport.Kraft paper remains especially popular in the U.S. because it visually signals natural or eco-friendly packaging, while white paper offers a cleaner premium canvas for detailed printing. Window-lid options are common for deli counters, pastry programs, and grab-and-go refrigerated meals. For hot applications such as ramen, rice bowls, chili, and soup, buyers usually prioritize rigidity, lid fit, and sidewall sealing.Product TypeCommon SizesBest ForLid OptionsTypical Material FinishDistribution NotesPaper bowls8 oz, 12 oz, 16 oz, 26 oz, 32 ozSoup, salad, noodlesPaper lid, PP lid, PET lidKraft or whiteStrong demand in delivery and lunch serviceLunch boxes500 ml, 700 ml, 900 ml, 1000 mlRice meals, pasta, takeoutFold-top or separate lidKraft or whitePopular with casual dining and takeout chainsCompartment meal boxes2-compartment, 3-compartmentMeal prep, school lunchesAttached lidUsually PE linedUseful for portion separationNoodle boxes16 oz, 26 oz, 32 ozAsian takeaway, stir-fryFold-topKraft/white with coatingFrequent in urban delivery marketsFry cups and snack cupsSmall, medium, largeFries, churros, snacksOpen topOil-resistant kraftCommon in stadium and food truck channelsDeli boxes with windows500 ml to 1000 mlBakery, salads, sandwichesPET window lid or window topKraft with clear panelStrong in retail-ready food programsPaper cups4 oz to 32 ozHot, cold, dessert beveragesFlat, dome, sip lidsSingle, double, ripple wallHigh repeat volume for chains and cafesThe range above is valuable because many U.S. distributors sell to mixed accounts: a coffee shop may need hot cups and dessert bowls, while a ghost kitchen may need soup bowls, compartment boxes, and sauce-compatible meal containers from the same supplier.var ctxIndustry = document.getElementById('barChartIndustry').getContext('2d');var chartIndustry = new Chart(ctxIndustry, {type: 'bar',data: {labels: ['Restaurants', 'Delivery Kitchens', 'Cafes', 'Grocery Prepared Foods', 'Caterers', 'Food Trucks'],datasets: [{label: 'Estimated U.S. Demand by Channel',data: [92, 88, 74, 81, 67, 59],backgroundColor: ['rgb(255, 99, 132)','rgb(54, 162, 235)','rgb(255, 206, 86)','rgb(75, 192, 192)','rgb(153, 102, 255)','rgb(255, 159, 64)']}]},options: {responsive: true,maintainAspectRatio: false}});This bar chart shows where a distributor’s product breadth matters most. Restaurants and delivery kitchens drive large, recurring volumes, but grocery prepared-food departments and cafes also represent important channels for size diversification and custom print programs.One of the most common questions from U.S. buyers is whether PE or PLA coating is better. The answer depends on performance requirements, sustainability positioning, cost targets, and local disposal conditions. PE, or polyethylene, has long been used because it provides dependable liquid and grease resistance, supports hot and cold applications, and is generally cost-effective. It remains the mainstream choice for many high-volume food service programs.PLA, or polylactic acid, is typically chosen when a compostable or bio-based positioning is important. It can align well with institutions, eco-focused brands, and cities where compostability messaging is commercially valuable. However, buyers should still review the disposal environment in the actual end market. A PLA-coated product may have strong marketing value, but its practical benefit depends on whether composting infrastructure and collection habits exist in the customer’s region.For the United States, PE often remains the best fit for value-driven national distribution, especially when leak resistance, temperature tolerance, and broad affordability are priorities. PLA becomes more compelling in premium food service, campus, corporate, and policy-sensitive environments. Smart distributors typically carry both options so they can match the buyer’s cost and compliance profile rather than forcing a one-material approach.FactorPE CoatingPLA CoatingBest FitU.S. Buyer ConsiderationSummary AdviceCostUsually lowerUsually higherHigh-volume commodity SKUsImportant for chain and wholesale biddingChoose PE when unit economics dominateLeak resistanceStrongStrong when properly madeSoups, noodles, saucesNeed sealing consistencyBoth can work if manufacturing is stableHeat performanceReliableApplication dependentHot meals and hot drinksTest with real menu itemsPE often wins for broad hot-use programsSustainability messagingModerateStrongerEco-positioned brandsUseful in West Coast and campus marketsPLA helps with compostable narrativesAvailabilityVery commonGrowing but more selectiveFast replenishmentMay affect lead times by SKUKeep safety stock for PLA programsEnd-of-life perceptionConventionalCompostable-orientedInstitutional sustainability programsNeed accurate local claim languageVerify certificates and local policy wordingThe comparison above helps buyers avoid a common mistake: choosing material only from a marketing perspective. The correct approach is to match coating choice to menu profile, budget, disposal environment, and customer communication needs.Large-scale paper food container production combines material science, tooling accuracy, controlled forming, printing quality, and final inspection. For U.S. importers and distributors, understanding the process helps explain why some suppliers are more reliable than others. Good containers start with carefully selected food-grade board, coating application, and dimensional consistency before any forming begins. Small variation at the sheet or roll stage can later create lid mismatch, seam weakness, or poor stacking.At scale, production usually follows a structured flow: substrate sourcing, printing, die-cutting, sidewall and base shaping, forming, heat sealing, rim curling where applicable, inspection, count packing, and warehousing. For cups and bowls, rim formation and side-seam quality are especially critical. For lunch boxes and deli containers, crease precision and corner locking matter more. For window-lid products, adhesive accuracy and film placement affect both appearance and food visibility.Advanced factories increasingly rely on automated equipment to control speed and consistency. This is relevant to U.S. buyers because stable automation typically means better repeatability across reorders. When a distributor promises the same 26 oz soup bowl every shipment, that consistency depends on tooling, machine settings, coating stability, and lab checks for leakage, compression, and migration compliance.In the technology capability area, a manufacturer with automated lines, flexographic printing, precision die-cutting, and in-house quality labs can usually support more dependable bulk programs. In manufacturing capability terms, integrated forming, inspection, and climate-managed warehousing improve carton stability before export. In service capability, the strongest partners help clients confirm artwork, samples, carton marks, and shipment schedules before production begins, which lowers risk for U.S. arrivals through ports such as Los Angeles, Oakland, Houston, Savannah, or Newark.Production StageMain PurposeKey Quality PointCommon Defect to AvoidWhy U.S. Buyers CareControl MethodPaper selectionBase material performanceFood-grade consistencyWeak stiffnessAffects stackability and strengthIncoming material checksPrintingBranding and graphicsColor alignmentSmudging or misregistrationImportant for retail appearancePrint monitoringDie-cuttingShape accuracyDimensional precisionPoor lid fitImproves packing line efficiencyTool calibrationForming and sealingContainer structureSeam strengthLeaksCritical for soups and saucesHeat and pressure controlInspectionDefect screeningRandom sampling resultsMixed quality lotsReduces claim ratesLab and visual QCWarehousingProduct protectionDry, clean storageMoisture damageMaintains import conditionClimate-conscious inventory managementThis production overview is useful when comparing suppliers. A distributor with real scale should be able to explain not just what it sells, but how it controls consistency from raw material through packed carton.var ctxTrend = document.getElementById('areaChartTrend').getContext('2d');var chartTrend = new Chart(ctxTrend, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026'],datasets: [{label: 'Shift Toward Sustainable Paper Packaging',data: [34, 41, 49, 58, 68],fill: true,backgroundColor: 'rgba(75, 192, 192, 0.25)',borderColor: 'rgb(75, 192, 192)',tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The area chart reflects the steady shift toward sustainability-focused paper packaging programs. By 2026, this trend is expected to influence specification choices, bid requirements, and custom product development more heavily across the United States.A useful example comes from a mid-sized U.S. distributor serving restaurant accounts in Texas and the Southeast. The company sold packaging to fast casual operators, Asian takeout concepts, and regional deli chains, but faced recurring problems with inconsistent bowl dimensions from multiple suppliers. Lid fit varied by batch, print colors drifted between reorders, and stock planning became difficult because lead times were unpredictable.To solve this, the distributor consolidated purchasing around a factory partner able to supply paper bowls, noodle containers, lunch boxes, fry cups, and custom paper cups under one sourcing plan. The project started with a requirement review covering food types, fill temperatures, carton pack preferences, and target margins. Samples were produced for testing with soup, ramen, sauced rice bowls, and chilled deli items. After approval, custom artwork and barcode placement were finalized for a private label launch.Within two ordering cycles, the distributor reduced SKU overlap, improved lid compatibility, and lowered packaging complaints from restaurant clients. A clearer order calendar also helped synchronize inbound shipments to Houston and Savannah. Because the product line came from a more integrated manufacturing system, repeat order consistency improved, and the distributor could present a stronger value proposition to new accounts.The most important lesson from this case is that success came from combining manufacturing stability with service support. Product itself matters, but so do sample validation, artwork preparation, realistic lead-time planning, and communication around freight and replenishment.ChallengeBefore ChangeAction TakenResultBusiness ImpactTakeawayLid mismatchFrequent complaintsStandardized bowl-lid systemBetter fitFewer returnsDimension control mattersToo many suppliersComplex purchasingConsolidated vendor baseSimpler sourcingLower admin costOne-stop supply improves efficiencyColor inconsistencyBrand image issuesCentralized print approvalStable appearanceStronger private label valueArtwork control is essentialLead-time uncertaintyInventory pressurePlanned reorder scheduleBetter forecast accuracyFewer stockoutsCapacity planning supports growthLimited product rangeMissed cross-sellingExpanded SKUsBroader offeringHigher account penetrationRange supports sales growthWeak end-customer trustPrice-focused sellingImproved product reliabilityHigher retentionBetter margin stabilityReliability sells better than low price aloneFor distributors in the United States, this kind of improvement is realistic when sourcing shifts from fragmented buying to a structured supply model.Certification is a major issue in the United States because food-contact documentation can affect customs clearance, distributor qualification, and end-customer trust. At minimum, U.S. buyers should ask for documentation that supports food-grade suitability and compliance with relevant standards for the materials used. Depending on the product, buyers may also request sourcing and quality system documents that support corporate procurement requirements.For paper food containers, common buyer expectations often include FDA-related food-contact compliance documentation, ISO 9001 quality management support, and FSC for responsibly sourced paper where sustainability claims are part of the buying program. For compostable products, BPI or OK Compost documentation may be important depending on market positioning and customer requirements. Buyers should also ensure the exact SKU and material configuration match the certificate scope rather than assuming one document covers all products.This matters even more in the United States because customer groups differ. A local diner in Phoenix may simply want a dependable soup bowl at the right price. A university dining contractor in California may require compostability documentation and chain-of-custody assurance. A distributor selling to natural grocery retailers in Seattle or Boston may need both sustainability language and performance proof.Good suppliers make compliance easier by organizing documentation before ordering begins. They can explain which products are FDA-compliant, which lines are compostable, and how to label marketing claims correctly. They also help prevent overclaiming, which is increasingly important in a market where environmental statements are under more scrutiny.Certification or StandardWhat It CoversWhy It Matters in the United StatesTypical BuyerBest Use CaseProcurement TipFDA food-contact complianceFood safety suitabilityBaseline requirement for many buyersImporters, distributors, chainsAll food-contact containersMatch document to specific materialISO 9001Quality management systemSignals process disciplineWholesalers and large accountsLong-term repeat programsAsk how QC is applied in practiceFSCResponsible paper sourcingSupports sustainability goalsRetail and institutional clientsKraft and white paper linesUse when sourcing claims are importantBPICompostability certificationUseful in compostable programsUniversities, eco-focused brandsPLA-coated linesConfirm claim language for local marketsOK CompostCompostability verificationHelpful for global procurement alignmentInternational buyers in U.S. marketsSpecial sustainability projectsVerify end-market relevanceEU food-contact standardsInternational compliance supportHelpful for broader brand confidenceMulti-region distributorsCross-market packaging programsUseful but not a substitute for U.S. needsThe table above shows that documentation is not just a formality. It shapes who you can sell to, how confidently you can market the product, and how easily your business can scale into more demanding customer segments.Minimum order quantity and pricing for paper food containers vary according to size, print requirement, coating type, material weight, lid combination, and packaging configuration. Plain stock items typically have lower MOQs, while custom-printed SKUs usually require higher volumes because of plate setup, production scheduling, and carton efficiency. For U.S. distributors, the key is balancing landed cost with inventory turnover. A lower unit price is not always beneficial if the MOQ is too large for your sales rhythm.Plain kraft bowls, white bowls, lunch boxes, and cups often work well for trial orders or regional distributor launches. Once demand stabilizes, custom print runs become more attractive because branding increases perceived value and can support margin improvement. In many cases, a supplier that offers flexible MOQs and lead times around 7 to 15 days for production can help buyers test new SKUs more safely before expanding into larger orders.Pricing also depends on whether the order includes matching lids, special coatings, window features, or compartment structures. Freight to the United States, palletization, and port routing can significantly affect the true landed cost. A distributor planning arrivals through Long Beach may structure orders differently from one routing through New York/New Jersey or Houston due to transit timing and warehouse replenishment patterns.Pricing FactorLower-Cost ScenarioHigher-Cost ScenarioImpact on MOQBest Buyer TypeAdvicePrintingPlain stockCustom multi-color brandingCustom usually higherStock for resellers vs private labelStart plain, scale to custom after validationCoatingPEPLAPLA may require more planningBudget vs sustainability programsChoose by market need, not trend aloneContainer sizeStandard SKUsSpecial dimensionsSpecial sizes increase MOQ riskBroad market vs niche usersUse common sizes for easier turnoverLid inclusionContainer onlyMatched full setMay increase order complexityDistributors serving delivery accountsBundle when presentation and sealing matterMaterial weightStandard paper basisHeavier boardOften similar MOQ but higher costHot food and premium brandsUse heavier stock for structural confidenceCarton packingStandard export packingSpecial retail or barcode needsCustomized packing may raise MOQPrivate label and retail channelsPlan carton marks earlyThe pricing table makes one point clear: cost is highly specification-dependent. Buyers should request quotations only after confirming size, coating, lid type, print, and carton configuration, otherwise comparisons will be misleading.var ctxSupplier = document.getElementById('comparisonChartSupplier').getContext('2d');var chartSupplier = new Chart(ctxSupplier, {type: 'bar',data: {labels: ['Product Range', 'Customization', 'Lead Time Stability', 'Certification Support', 'Scale Capacity', 'Service Responsiveness'],datasets: [{label: 'Factory-Integrated Supplier Score',data: [92, 90, 86, 94, 91, 88],backgroundColor: 'rgb(153, 102, 255)'},{label: 'Basic Trading Supplier Score',data: [68, 61, 57, 63, 54, 66],backgroundColor: 'rgb(201, 203, 207)'}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart highlights why many U.S. buyers prefer integrated supply partners for long-term programs. The advantage is not only price; it is also product range, documentation support, lead-time visibility, and customization control.For buyers seeking a dependable supply partner, Shandong Fude Packaging Co., Ltd. serves global food service and distribution clients with a focused approach to practical and eco-conscious paper packaging. Since its founding in 2004, the company has built long-term experience supplying disposable food-grade packaging to customers across multiple continents, including North America. Its strength is not just in manufacturing volume, but in combining technical process control, production integration, and customer service that supports repeat wholesale orders.From a technology perspective, the company operates with automated equipment, flexographic printing capability, die-cutting systems, forming lines, and quality inspection resources that help maintain repeatable production standards. That matters for U.S. buyers who need consistent rim curling, stable seams, accurate print placement, and dependable carton packing. From a manufacturing standpoint, a modern large-scale facility, daily cup output capacity, organized workflow, and warehousing support make it easier to handle both standard and customized orders for restaurants, wholesalers, and distributors.From a service standpoint, the company works through a streamlined process that begins with requirement review, moves through design and sample confirmation, and then advances to production and delivery coordination. This is useful for U.S. importers because it reduces confusion in artwork preparation, size selection, and shipment planning. The team also supports OEM and private label programs for logos, structures, materials, coatings, and dimensions.Its portfolio includes kraft and white food containers, paper bowls, lunch boxes, trays, noodle boxes, fry cups, deli boxes, compartment meal boxes, and paper cups from small to large beverage sizes. Matching lids, window features, and coating options can be adapted to menu needs. For businesses that want to learn more about the available product line, visit paper packaging products. To understand the company background in more detail, see about Fude. Buyers looking for customization workflow information can review packaging services, and those ready to discuss specifications or request samples can use contact our team.For the United States market, the company is especially relevant to distributors, wholesalers, chains, food delivery platforms, and emerging brands that need a one-stop source with compliance awareness, product breadth, and support for scalable repeat ordering.What should a U.S. buyer look for first in a paper food containers distributor?Start with food-contact compliance, leak performance, size range, and lead-time reliability. Then evaluate print quality, lid compatibility, MOQ flexibility, and communication speed.Are kraft paper containers better than white paper containers?Not necessarily better, but different. Kraft offers a natural, eco-oriented look that many U.S. consumers like. White paper is often preferred for cleaner premium branding and vivid logo printing.Which is better for soup and saucy food, PE or PLA?Both can work if made properly. PE is usually the more cost-effective mainstream option for hot and liquid-heavy applications. PLA is often selected when compostable positioning is important.Can I order custom branding for a distributor program?Yes. Custom logos, size configurations, coatings, and carton marks are commonly available. Most custom programs require higher MOQs than plain stock items.What industries buy the most paper food containers in the United States?Restaurants, fast casual chains, delivery kitchens, grocery prepared-food departments, cafes, caterers, food trucks, stadium vendors, and institutional dining operations are all major buyers.What lead times are common?Production timing varies by order complexity, but many standard wholesale programs work within a short production window once specifications and artwork are approved. Freight timing to the United States must be added separately.How do I reduce risk when switching suppliers?Approve samples, test with real menu items, confirm certificates by SKU, align lid/container systems, and begin with a manageable order mix before moving to larger annual contracts.What are the biggest 2026 trends to watch?Expect more demand for compostable lines, stronger sourcing scrutiny, more custom branding, improved barrier materials, smarter inventory planning, and packaging designs optimized for delivery and heat retention.Are local U.S. suppliers always better than overseas factory-direct sources?Not always. Local suppliers may shorten replenishment time for standard stock, but factory-direct partners can offer wider customization, stronger price control at scale, and better integration for private label programs. The best choice depends on volume, urgency, and complexity.What applications are growing fastest?Prepared meals, noodle and rice bowls, deli salads, grab-and-go lunch boxes, premium dessert packaging, and branded beverage cups are among the strongest growth categories.The U.S. market for paper food containers in 2026 will reward suppliers and distributors that combine performance, compliance, sustainability awareness, and operational discipline. Whether your business serves downtown restaurants in Manhattan, suburban caterers in Dallas, university accounts in California, or deli wholesalers in New Jersey, the right packaging partner should help you sell more confidently, not just source more cheaply. -
Branded Kraft Boat Tray Sizing Guide for Canada Buyers
The right branded kraft boat tray is the smallest practical format that carries the intended handheld snack or branded food service portion without crushing, spilling, looking underfilled, or leaving excessive empty space. For Canadian restaurant chains, stadium vendors, food trucks, cafés, promotional agencies, and distributors, tray selection should be based on actual food tests rather than nominal dimensions alone.A tray may appear large enough on a specification sheet but fail during service when fries shift, sauce cups tip, poutine weight softens the base, or stacked trays rub against printed areas. Conversely, a tray that is too large can make a premium portion look small, increase paper consumption, take more delivery-bag space, and raise freight costs into Canada through Vancouver, Prince Rupert, Montréal, Halifax, or Toronto distribution routes.Use a repeatable approval process: fill samples with real menu portions, include condiments and liners, check headspace, weigh the filled tray, simulate customer carrying movement, and inspect the print after contact with oil, heat, and adjacent packages. Confirm the finished specification with measurable acceptance criteria, approved artwork, material details, packing configuration, and batch reference information.For a starting point, explore Fude Packaging’s custom boat tray range and compare formats against the foods actually sold at your Canadian locations. The goal is not simply to select a capacity; it is to protect food quality, present the portion consistently, and maintain a recognizable brand experience.Handheld foods vary significantly in footprint, height, grease level, and customer handling. A narrow tray can hold a small fry portion efficiently, while loaded nachos, chicken tenders, mini churros, or poutine need broader support and more practical clearance. The best branded kraft boat trays match the food’s real serving profile, not only its nominal weight.In Canada, menu patterns often differ by region and venue. A downtown Toronto quick-service operator may need a compact tray for commuter-friendly snacks. A Calgary sports venue may need a sturdier, broader tray for fries, wings, and toppings. A Québec festival supplier may need high-visibility French-English brand artwork and formats that are quick to fill during peak service. Vancouver operators may prioritize fibre-based packaging and portion presentation for plant-forward snacks or street-food concepts.Food Service ItemRecommended Tray ProfileUseful HeadspacePrimary RiskRecommended TestSmall friesNarrow, shallow boat tray8–12 mmPortion looks sparseShake test and visual fill checkLoaded friesMedium-width, deeper tray15–25 mmSauce overflowHeat and topping migration testPoutineWide-base, grease-resistant tray20–30 mmBase softening and leakage20-minute hold testChicken tendersLong rectangular boat tray12–20 mmProduct shiftingCarry and bag insertion testNachosBroad, open presentation tray20–35 mmEdge spill and topping lossCounter-service handling testChurros or dessert bitesMedium shallow tray10–18 mmSugar and oil transferPrint rub inspectionMini slidersWide, deeper tray with liner option15–25 mmCompression during transportStacking testThis table is a planning guide rather than a replacement for physical samples. Ingredient variability matters. Fries with dry seasoning behave differently from fries with gravy; crispy chicken behaves differently after a 20-minute delivery hold; and cheese-topped foods create different thermal and grease exposure conditions. Standardize the food build before approving the tray.Nominal capacity is the theoretical internal volume of a tray. Usable volume is the space that remains practical after allowing for food shape, topping height, customer movement, sauce cups, liners, and safe headspace. A tray may technically hold 700 mL of water, yet only function well with a 450–550 mL loaded-food portion.Water tests can be helpful for comparing formats, but they are not enough for branded food service. Real snacks contain uneven pieces, irregular toppings, air spaces, sauces, and high points. The operational question is: “Can staff fill this tray quickly and consistently, while customers can carry it without mess?”Nominal CapacityTypical Usable Food VolumeSuggested ApplicationTypical Filled Weight RangeApproval Note250 mL170–200 mLSmall fries, bite-size sweets70–140 gBest for low-sauce items400 mL280–330 mLRegular fries, nuggets140–260 gCheck sidewall stability550 mL390–460 mLTenders, loaded snack portions220–380 gAllow space for toppings750 mL530–640 mLLoaded fries, poutine350–600 gRequire grease-resistance test1,000 mL700–850 mLShareable snacks, nachos500–850 gReview delivery-bag fit1,250 mL880–1,050 mLVenue sharing portions700–1,100 gConfirm base compression strengthThe figures above show why capacity alone should never determine procurement. For a Canadian chain offering a regular poutine, the usable volume and filled weight are more important than a nominal millilitre figure. A practical trial should include the highest expected topping load, the warmest holding condition, and a realistic customer journey from counter to table, car, or delivery address.Tray geometry influences customer perception as much as capacity. Broad and shallow trays create visual abundance, making fries, nachos, and shareable snacks look generous. Narrow and deep trays can contain taller foods efficiently but may hide the portion and make toppings difficult to access. Length matters for chicken tenders, skewers, churros, and mini sandwiches, while corner shape affects how sauces pool and how easily customers can pick up food.For branded kraft boat trays, dimensions also determine how visible the logo is during service. A broad front panel provides a stronger brand surface at a counter, concession stand, or food truck window. However, large open panels can be more exposed to oil staining or abrasion when trays are stacked. The ideal design balances food presentation, structural performance, and print visibility.var ctx1 = document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctx1, {type: 'line',data: {labels: ['2022', '2023', '2024', '2025', '2026', '2027'],datasets: [{label: 'Indexed Canadian demand for branded paper snack trays',data: [100, 108, 117, 126, 136, 148],borderColor: 'rgb(120, 82, 45)',backgroundColor: 'rgba(120, 82, 45, 0.12)',borderWidth: 3,fill: false,tension: 0.3}]},options: {responsive: false,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: false, title: { display: true, text: 'Demand index' } } }}});This market-growth chart is an indexed planning illustration for procurement teams, showing the continued role of branded fibre-based snack packaging as Canadian operators expand takeaway, event food service, and delivery-ready menu formats. Demand will differ by province, menu type, municipal waste rules, and seasonal event calendars.Many boat trays are intended for open counter service, but some Canadian food businesses use clear covers, paper wraps, sleeves, carry trays, or delivery bags to protect food on the move. Tray selection should therefore consider the complete packaging system. A well-sized boat tray can still fail if it slides inside a delivery bag, catches against a bag seam, or presses toppings into a lid.Where a lid is used, verify the effective internal lid height rather than relying on the external lid specification. For open trays placed in bags, evaluate whether the bag supports the base and whether adjacent products can move into the tray. This is especially important for delivery routes in Toronto, Montréal, Ottawa, Edmonton, and other cities where traffic time can turn a ten-minute dispatch into a longer holding period.Packaging CombinationSuitable Food TypeKey Fit CheckCommon FailureRecommended ActionOpen tray + paper bagDry fries and churrosBag base widthTray tilts in transitUse a flat-bottom bagTray + clear coverLoaded fries and dessertsTop clearanceToppings touch lidIncrease headspaceTray + greaseproof linerWings and fried chickenLiner overlapOil reaches print areaSpecify suitable barrier paperTray + carry cartonMultiple snack ordersCarton internal heightTray compressionTest full stack loadTray + delivery bagPoutine and nachosMovement during turnsSauce spills over edgeUse deeper format or support insertTray + beverage bundleCombo mealsSide clearanceDrink condensation transferSeparate wet and dry zonesThe table highlights why packaging must be approved as a system. Ask staff to pack a complete customer order, including beverages, napkins, condiments, and promotional inserts. Then perform a carry test, a short vehicle test where appropriate, and a stacking check. The correct branded tray protects both the food and the brand identity at the moment customers see the order.Custom printing must survive real handling conditions. Ink rub often appears on the outer sidewalls where trays contact one another during nesting, packing, stacking, or bagging. Oil staining may become visible along the base, lower sidewall folds, and corners where grease accumulates. Registration drift is most noticeable around logos, fine typography, border lines, QR codes, and artwork positioned close to folds or die-cut edges.For Canadian branded food service, print approval should include both a flat artwork review and a formed-product inspection. A logo that looks centered on a digital proof may shift visually after tray forming because curved edges, folded panels, and food placement alter what customers see. Keep essential brand elements away from creases, glue zones, and high-contact areas.Service ConditionLikely Print or Material IssueWhere It AppearsHow to TestAcceptance CriterionNested tray storageInk rubOuter walls and rimSeparate and inspect 20 nested traysNo visible logo damage at normal viewing distanceHot fried foodOil stainingBase corners and lower panelsHold filled tray for 20 minutesNo unacceptable seepage or print distortionSauce-heavy portionBarrier weaknessInterior base and foldsFill with maximum sauce loadNo softening that affects handlingFast counter serviceRegistration drift visibilityFront brand panelInspect formed samples against approved proofLogo remains within agreed toleranceDelivery-bag transportScuffingEdges and side panelsSimulate bag insertion and removalNo major scuffs on key artworkCondensation exposureColour change or fibre softeningBottom surfacePlace beside cold beverage for 15 minutesTray remains stable and legibleExplain the acceptance standard before production begins. “Good print quality” is too vague for a repeat order. Instead, define approved Pantone references where relevant, permissible placement tolerance, minimum readable text size, prohibited defects, inspection sample quantity, and the conditions under which the tray will be tested. This makes supplier communication clearer and reduces disagreement after arrival at a Canadian warehouse.Reducing stock-keeping units can simplify purchasing, warehouse organization, and restaurant training. However, using one tray size for every menu item usually creates compromise: small portions look lost, large portions overflow, and delivery performance becomes inconsistent. The better strategy is to create a small family of compatible sizes with shared material, print style, case packing logic, and operational purpose.For example, a three-size tray program can often serve a large share of snack menus: a small tray for fries and dessert bites, a medium tray for tenders and regular loaded snacks, and a large tray for poutine, nachos, and sharing portions. Use a fourth specialist tray only when a menu item truly requires a different length, depth, or structural profile.var ctx2 = document.getElementById('industryDemandChart').getContext('2d');new Chart(ctx2, {type: 'bar',data: {labels: ['Quick Service', 'Sports Venues', 'Food Trucks', 'Cafés', 'Catering', 'Retail Deli'],datasets: [{label: 'Relative demand for custom snack trays',data: [88, 76, 69, 51, 58, 46],backgroundColor: ['#8b5a2b', '#a66c36', '#c18345', '#7c9b6b', '#b06f49', '#6a8f9a']}]},options: {responsive: false,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Demand score' } } }}});This industry-demand comparison helps buyers prioritize where branded kraft boat trays can deliver the strongest operational and marketing value. Quick-service restaurants and sports venues commonly need high-volume, fast-fill formats, while caterers may value presentation and transport stability more heavily. Each segment should use its own menu and service workflow as the final decision point.Once a tray has passed food, transport, print, and staff-use testing, record every production-critical detail. A purchase order description such as “kraft fries tray with logo” is not enough for consistent reorders. The final specification should identify dimensions, board grade, coating or barrier requirement, fold construction, print colours, artwork revision, packing method, carton dimensions, quantity tolerance, quality criteria, and approved sample reference.A clear record protects multi-location businesses when staff change, menus evolve, or procurement moves from one Canadian region to another. It also helps distributors coordinate mixed packaging programs for customers serving from Vancouver to Winnipeg, Toronto, Montréal, and Halifax.Specification ItemWhat to RecordWhy It MattersOwnerReorder CheckTray dimensionsTop length, width, base, depthControls food fit and bag compatibilityBuyerCompare to approved drawingMaterial constructionPaper type, basis weight, barrierControls rigidity and grease performancePackaging managerReview material declarationArtwork revisionFile name, date, colour referencesPrevents outdated brandingMarketing teamMatch digital proofPrint placementLogo panel and tolerance zoneMaintains visible brand presentationQuality teamInspect formed trayFilled-weight limitMaximum approved food loadPrevents structural failureOperations teamRepeat load testPack configurationUnits per sleeve, carton, palletSupports warehouse efficiencyLogistics teamVerify carton labelApproved sample codePhysical sample or photo referenceCreates a common quality benchmarkBuyer and supplierRetain before each production runA written approval record is especially valuable for imported packaging. It provides a practical bridge between a Canadian purchasing team, overseas factory staff, freight partners, and receiving warehouses. Include photos of a filled tray, a side view showing headspace, a bag-fit image, and any approved defect examples. These simple records reduce interpretation gaps.Canada continues to reward packaging that is functional, branded, and easier to align with evolving sustainability goals. Food service operators are balancing customer demand for convenient takeaway with provincial and municipal expectations around single-use items, material recovery, and environmental claims. Requirements differ by location, so buyers should confirm current local obligations rather than assume one national rule applies to every food-service format.In 2026 and beyond, purchasing teams are likely to place more emphasis on verified material information, traceable supply, reduced excess packaging, lighter-weight structures that still perform, and designs that help customers sort packaging correctly. Digital workflow improvements will also matter: faster artwork approvals, documented colour targets, QR-enabled batch records, and data-supported inventory planning can reduce costly errors for chains and distributors.var ctx3 = document.getElementById('trendShiftChart').getContext('2d');new Chart(ctx3, {type: 'line',data: {labels: ['2023', '2024', '2025', '2026', '2027', '2028'],datasets: [{label: 'Standard unbranded tray purchasing',data: [62, 57, 51, 46, 42, 38],borderColor: '#8f8f8f',backgroundColor: 'rgba(143,143,143,0.20)',fill: true,tension: 0.3},{label: 'Specified branded fibre-based tray purchasing',data: [38, 43, 49, 54, 58, 62],borderColor: '#7b552d',backgroundColor: 'rgba(123,85,45,0.22)',fill: true,tension: 0.3}]},options: {responsive: false,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 70, title: { display: true, text: 'Procurement mix (%)' } } }}});The area chart illustrates a directional purchasing shift toward more specified, brand-controlled fibre-based tray programs. It does not replace local regulatory advice. Canadian buyers should request documentation appropriate to the intended food-contact application and destination market, and should ensure any sustainability statement is accurate, supportable, and consistent with the selected material system.Fude Packaging supports overseas B2B buyers with custom paper food packaging programs that combine practical engineering, manufacturing control, and export-oriented service. For branded kraft boat trays, the process begins with food type, serving temperature, portion target, grease exposure, artwork, order volume, and Canadian delivery requirements rather than a generic quotation.Fude Packaging uses in-house quality and performance testing to support evaluations of structure, print appearance, food-contact suitability, grease resistance, heat performance, and filled-product handling. Digital proofs, white samples, and printed pre-production proofs help buyers validate dimensions and brand presentation before mass production. Artwork and dieline review can identify issues such as text placed too close to fold lines, insufficient logo clearance, or graphics that may be distorted during forming.For Canadian buyers that need a broader food-service program, Fude Packaging can also coordinate compatible paper cups, bowls, boxes, trays, and multi-compartment meal packaging. This can simplify visual consistency across quick-service menus and reduce the administrative burden of managing several unrelated suppliers. Learn more about available custom packaging services.With more than 20 years of packaging experience, a 30,000 m² self-owned production base in Shandong, automated capacity of up to 120,000 units per day, and full-batch traceability practices, Fude Packaging is positioned to support both established food chains and growing distributors. In-house control covers material selection, printing, die-cutting, forming, inspection, packing, and shipment preparation.Its production systems can support documentation and material programs associated with BRC, FSC, ISO 9001, LFGB, FDA-related food-contact requirements, and other destination-market needs, subject to the final product specification. Buyers can review the company background through Fude Packaging’s manufacturing profile when assessing supplier capability for Canadian imports.Fude Packaging provides project support from sampling through export-ready packing. Canadian customers can discuss port routing, full-container or less-than-container shipments, express sample delivery, production scheduling, commercial documents, packing lists, and inspection arrangements. Typical standard production timing can be approximately 7–15 days depending on specifications and order volume.The service approach is suitable for buyers managing seasonal promotions, food-truck launches, stadium events, restaurant rollouts, and distributor replenishment schedules. A buyer may begin with a white sample to check food fit, then approve a printed pre-production sample for colour and placement, followed by a documented mass-production approval. For related snack packaging, see the kraft paper fries cup collection.Canadian buyers generally choose among local stock distributors, local short-run printers, and overseas custom manufacturers. The best route depends on demand stability, artwork complexity, lead time, order size, storage capacity, and desired control over the final specification. A blended approach can also work: use local stock for urgent replenishment and planned import orders for standardized branded programs.var ctx4 = document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctx4, {type: 'bar',data: {labels: ['Unit Cost Efficiency', 'Custom Size Options', 'Print Consistency', 'Urgent Availability', 'Documentation Support', 'Large-Scale Capacity'],datasets: [{label: 'Local stock distributor',data: [58, 35, 50, 92, 55, 48],backgroundColor: '#78909c'},{label: 'Planned custom manufacturing program',data: [88, 90, 86, 45, 82, 94],backgroundColor: '#8b5a2b'}]},options: {responsive: false,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: 'Relative capability score' } } }}});This comparison chart is a procurement-planning tool. Local suppliers can be valuable for short lead times and emergency stock, while planned custom production typically offers more flexibility in tray geometry, large-run branding, and structured approval processes. Evaluate landed cost rather than only unit price, including cartons, palletization, container utilization, customs documentation, inland delivery, and inventory carrying cost.Toronto quick-service fries concept: A multi-location operator used one medium tray for every fry option. Small portions looked underfilled, while loaded fries sat too close to the edge. After testing, the operator retained a smaller tray for plain fries and a deeper medium tray for topped products. The revised program improved visual consistency and reduced wasted board on entry-level portions.Calgary arena concession: A venue needed trays that could be filled rapidly during intermission. The final selection used a broad, easy-access format for tenders and fries, with a high-contrast logo on the front panel. Tests included one-handed carrying, rapid stacking, and nesting separation. The approval record specified a practical maximum fill line to help temporary event staff serve consistent portions.Montréal promotional food brand: A campaign required a kraft look with detailed graphics. The team reviewed print placement on formed samples, moving fine text away from fold zones and high-contact edges. A printed pre-production sample was approved before the campaign quantity was released, reducing the risk of registration concerns during the promotional launch.Vancouver delivery-focused snack kitchen: The brand offered loaded fries and plant-based poutine alternatives. The tray program was approved only after delivery-bag movement testing, including maximum sauce load and a 20-minute hold. The selected size created enough headspace to protect toppings while avoiding an oversized appearance.Measure the food as it is actually served, including toppings, sauce cups, liners, and garnish. Record the food footprint, maximum food height, average and maximum filled weight, and required headspace. Then test at least two tray options using the real portion build. Choose the smallest tray that allows safe handling and an attractive presentation.Most dry snacks need approximately 8–15 mm of headspace, while loaded fries, poutine, nachos, and sauce-heavy foods often need 15–30 mm or more. The correct amount depends on the transport method, topping height, and whether a lid or carry carton is used. Confirm headspace through a shake, carry, stacking, and bag-fit test.Yes, provided the portions have compatible footprints, heights, weights, and handling requirements. A small, medium, and large tray family often covers a broad menu efficiently. Do not force one size onto foods that differ significantly, such as plain fries, poutine, long chicken tenders, and wide nacho portions.A custom tray size is justified when stock formats create repeated operational problems: poor food presentation, overflow, weak delivery performance, wasted material, poor bag fit, or an insufficient branding panel. It can also be justified when a chain has high volumes and needs a format that supports faster filling, consistent portion control, or a unique menu signature.The most reliable test is a real-food application trial using the maximum approved menu build. Fill the tray with the heaviest expected portion, hold it at service temperature, carry it, place it in the intended bag or carton, simulate movement, and inspect the base, corners, print, and food appearance after the expected hold time. Record the result with photos and approval notes.For Canadian buyers, the final decision should be based on measurable performance: portion fit, headspace, filled weight, grease resistance, print durability, bag compatibility, and repeat-order control. A well-specified branded kraft boat tray becomes a reliable part of the customer experience rather than an avoidable source of spills, waste, or inconsistent presentation. -
Global Market Guide to Compostable Takeout Box Buying
For wholesale compostable takeout boxes, the purchasing decision should be based on evidence rather than a general “eco-friendly” label. Global market buyers need to confirm what the box is made from, which barrier layer is used, whether the product is suitable for the intended food and serving temperature, and whether compostability claims apply in the destination market.A molded fiber clamshell, kraft paper lunch box, or coated paper takeaway container can look similar externally while performing very differently with hot curry, fried chicken, salad dressing, noodles, soup, steam, or oily foods. A buyer should request a material specification, food-contact declaration, test samples, barrier description, temperature-use limits, and applicable compostability documentation before approving mass production.For importers supplying restaurants in Singapore, Dubai, London, Los Angeles, Sydney, Toronto, Rotterdam, or São Paulo, local disposal infrastructure matters as much as material composition. A package may be certified compostable under industrial composting conditions but still be unsuitable for a municipal waste stream that does not accept food-service packaging. Marketing claims should therefore distinguish between compostable material, certified compostable products, recyclable paper-based products, and locally accepted waste solutions.Buyer CheckpointWhat to ConfirmWhy It MattersRecommended EvidenceBase materialBagasse, kraft paper, bamboo pulp, paperboard, or blended fiberDetermines rigidity, appearance, renewable-content profile, and end-of-life routeMaterial data sheet and production specificationBarrier layerWater-based coating, PLA, PBAT blend, aqueous dispersion, or other treatmentControls resistance to oil, sauces, moisture, and vaporBarrier chemistry declaration and product sampleFood contactApplicable market, food type, contact duration, and temperature rangeDocumentation must match the actual food applicationDeclaration of compliance and migration supportHeat performanceHot-fill use, microwave suitability, freezer performance, and steam exposurePrevents softening, warping, leakage, or lid failureHeat-use statement and practical food trialCompostability claimIndustrial, home, or non-certified compostable wordingReduces risk of misleading environmental marketingRelevant certificate scope and approved artworkSupply consistencyRaw-material source, coating specification, approved sample, and change processProtects repeat orders from unnoticed performance changesChange-control agreement and batch recordsThe table above provides a practical approval sequence. Buyers should treat each item as a separate checkpoint. Food-contact compliance does not automatically prove compostability, and compostability certification does not automatically prove resistance to hot oil or heavy sauce.Compostable takeaway boxes are commonly produced from molded plant fiber, paperboard, or kraft paper structures. Bagasse is made from sugarcane-processing residue and is widely used for hinged clamshells, meal trays, and compartment containers. It offers a natural fiber appearance and good rigidity, especially for dry and moderately moist foods. Bamboo pulp and other molded fibers may be selected where strength, smoothness, or a particular visual finish is required.Paperboard and kraft paper boxes are typically cut, printed, creased, formed, and bonded into lunch boxes, noodle boxes, salad containers, burger boxes, or folded takeaway trays. Their performance depends heavily on paper grammage, structural design, seam construction, and barrier coating. A carton designed for dry bakery items should not automatically be used for saucy rice bowls or fried food with prolonged holding time.Buyers should ask suppliers whether the fiber is virgin, recycled, FSC-certified, or mixed. Recycled content may support circularity objectives, but it must remain suitable for the intended food-contact application. Material choices also affect print quality, odor, stiffness, stacking strength, and the box’s behavior in humid container shipping conditions.Material TypeTypical Product FormatStrengthsBuyer ConsiderationsBagasse molded fiberClamshells, trays, compartment meal boxesRigid structure, natural appearance, good heat toleranceConfirm oil resistance and lid closure under steamBamboo pulp fiberPremium trays, bowls, food boxesDense fiber structure and refined surface finishCheck availability, color consistency, and cost premiumUncoated kraft paperBakery boxes, dry-food cartons, snack packagingPaper-forward appearance and easy printingLimited protection against sauce and greaseCoated kraft paperLunch boxes, salad containers, noodle boxesBetter moisture and grease performanceVerify coating chemistry and end-of-life claimWhite paperboardBranded meal boxes and retail takeaway packsStrong color reproduction and clean presentationConfirm whether bleach, coating, and inks suit market requirementsFiber-paper compositeSpecialty hot-food or delivery formatsCan balance stiffness and functional protectionReview separability and certified compostability scopeMaterial composition should be linked directly to the food menu. Fried seafood, butter chicken, ramen, poke bowls, grilled meats, pastries, and cold salads each create different risks. A wholesale buyer should build an item-by-item specification rather than use one generic compostable box across every menu category.Barrier performance describes how well a package resists oil, water, sauces, vapor, and food residue. It is one of the most important technical factors in compostable food packaging procurement. A box may remain visually intact for a few minutes but fail after thirty minutes of contact with hot gravy, chili oil, or steam from freshly cooked rice.Water-based and aqueous dispersion barriers are increasingly used on paper packaging because they can provide moisture protection while reducing reliance on conventional plastic films. PLA and other bio-based coatings can also be applied in certain products, although their suitability depends on product structure, heat conditions, and composting certification scope. The right answer is not “one barrier fits all”; it is the barrier that matches the food, delivery time, temperature, and disposal objective.For oily foods, request practical testing with the actual oil level and holding period. For sauces, test seam edges, corners, bottom panels, and lid interfaces. For hot steam, evaluate both the internal surface and the exterior carton strength after closure. The final assessment should include delivery movement, stacking, and exposure to condensation.var ctxBarrier=document.getElementById('barrierDemandChart').getContext('2d');new Chart(ctxBarrier,{type:'bar',data:{labels:['Dry bakery','Cold salad','Fried foods','Saucy meals','Noodles','Steam-held rice'],datasets:[{label:'Relative barrier requirement',data:[25,55,82,92,88,78],backgroundColor:['#b7d7a8','#8fc9b3','#f6c66c','#ef8c75','#72a8d8','#9d91d4']}]},options:{responsive:false,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:100,title:{display:true,text:'Requirement index'}}}}});The chart shows an indicative purchasing priority rather than a laboratory standard. Saucy meals, noodles, fried foods, and steam-held rice generally require more demanding barrier and structure validation than dry bakery packaging.Food ConditionPrimary RiskSuitable EvaluationTypical Wholesale RecommendationDry pastriesCrushing and moisture pickupStacking and compression testUncoated or lightly protected paperboard boxCold saladDressing seepage and condensationLeak test with acidic dressingCoated paper or molded fiber with matching lidFrench fries and fried chickenOil penetration and heat retentionGrease holdout and steam trialGrease-resistant fiber or coated kraft structureCurry and stewHot liquid leakageCorner, seam, and bottom soak testHigh-barrier box or separate lidded containerNoodlesHot broth, steam, and lid deformationThirty-to-sixty-minute service testHeat-appropriate coated paper containerRice meal boxCondensation and softeningClosed-lid steam retention testMolded fiber or vented paperboard meal boxFood-contact documentation should be reviewed according to destination market, food type, contact duration, and intended temperature. Buyers shipping into the European Union commonly assess compliance against relevant EU food-contact framework requirements, including EC 1935/2004 where applicable. Buyers supplying the United States may request documentation supporting applicable FDA food-contact requirements. Other destinations may have national rules, importer obligations, or retailer-specific approval standards.A declaration should identify the product, material, intended use conditions, and supplier or manufacturer. It should not be treated as a universal document valid for every product. For example, a declaration supporting room-temperature dry-food contact may not cover hot, fatty food contact. Printing inks, adhesives, coatings, and colorants should also be evaluated as part of the finished packaging system.For regulated food-service programs, keep a document pack for each approved SKU: product drawing, material specification, food-contact declaration, relevant test summaries, certificate copies where claimed, carton label approval, and production batch reference. This approach is particularly valuable for distributors in Hamburg, Antwerp, Jebel Ali, Singapore, Melbourne, and Long Beach, where customer audits and customs documentation can create delays if files are incomplete.Laboratory data is useful, but real-use trials are essential. A wholesale buyer should test samples with the foods that create the highest risk, not only with water. A robust test plan may include hot oil, tomato sauce, coconut curry, vinegar dressing, broth, fried food, rice steam, and freezer-to-room-temperature condensation.Define the actual service window. A quick-service restaurant that hands food directly to the customer may need a twenty-minute performance window. A delivery platform serving a large city such as Jakarta, New York, Riyadh, or Paris may require forty-five to ninety minutes because meals travel farther and remain closed longer. Include courier movement and stacked-bag pressure where possible.Test MethodSuggested ConditionWhat to ObserveAcceptance ExampleHot-fill trialFood packed at intended serving temperatureWarping, odor, coating change, lid fitNo structural failure during defined holding periodGrease holdoutOily food or oil contact on base panelStaining, penetration, exterior transferNo visible exterior grease breakthroughSauce leakage testHot or cold sauce at normal fill volumeCorner leaks, seam opening, bottom seepageNo leakage after agreed transport simulationSteam retention testClosed container with hot rice or noodlesSoftening, collapse, condensation damageBox remains functional and stackableCompression testFilled packs stacked in delivery configurationCrushed walls, lid release, product deformationMaintains closure at defined stack loadFreezer-condensation testChilled or frozen food brought to ambient conditionsWet-out, delamination, loss of rigiditySuitable for stated chilled-use profileThe acceptance criteria should be agreed before purchase order confirmation. Photographs, retained samples, and written observations make it easier to resolve disputes if later production differs from the approved sample.Environmental wording requires precise control. “Compostable,” “industrially compostable,” “home compostable,” “biodegradable,” “plastic-free,” “recyclable,” and “renewable” are not interchangeable claims. A buyer should use only the wording supported by the specific product, coating, ink system, certification scope, and destination-market advertising rules.If a product is certified under a recognized program such as BPI or OK Compost, verify the certificate number, scope, current status, product construction, and approved claim language. Certification for a raw material does not necessarily certify the finished printed box. Similarly, a paper-based box may be recyclable in theory but unacceptable in recycling streams when heavily contaminated with food or combined with a barrier that local facilities cannot process.For the global market, the most responsible communication is practical: explain the material, state the applicable composting condition, and direct end users to local collection guidance. Do not promise that a package will enter every municipal composting system. This is especially important where city programs differ between neighborhoods or commercial waste contractors.var ctxTrend=document.getElementById('trendShiftChart').getContext('2d');new Chart(ctxTrend,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Conventional plastic-lined formats',data:[64,58,51,45,39,33],fill:true,backgroundColor:'rgba(211,110,100,0.18)',borderColor:'#d36e64',tension:0.3},{label:'Verified fiber-based alternatives',data:[22,29,37,45,53,61],fill:true,backgroundColor:'rgba(86,166,128,0.22)',borderColor:'#56a680',tension:0.3}]},options:{responsive:false,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:70,title:{display:true,text:'Indicative sourcing share (%)'}}}}});This area chart illustrates an expected sourcing shift rather than a guarantee of market-wide adoption. The strongest growth is likely where buyer specifications, municipal infrastructure, food-service legislation, and consumer expectations develop together.Minimum order quantity and pricing depend on box style, material, coating, printing, tooling, packing configuration, and shipping method. Plain stock items may support lower MOQs, while custom-printed boxes, special compartments, unique lid systems, and certified material programs generally require larger production runs.Buyers should compare total landed cost instead of unit price alone. A cheaper container that leaks during delivery can create food replacement costs, customer complaints, reputational damage, and higher operational waste. Similarly, a premium compostable construction may be commercially justified if it supports a restaurant chain’s brand position and meets a retailer’s documented packaging policy.For global import planning, container utilization is significant. A buyer importing through Ningbo, Qingdao, Shanghai, Rotterdam, Felixstowe, Jebel Ali, or Los Angeles should calculate carton dimensions, pallet requirement, container fill rate, and local warehousing cost. Consolidating cups, bowls, trays, and takeaway boxes from a single manufacturer can reduce freight complexity.Cost DriverEffect on PriceHow Buyers Can Manage ItPotential Trade-OffFiber typePremium or certified fibers may increase costMatch material grade to end-use needLower-cost fiber may affect finish or strengthBarrier coatingFunctional coatings add processing costUse food-specific test criteriaOver-specification can raise unit price unnecessarilyCustom printingArtwork setup and color control affect pricingStandardize artwork across SKUsFewer colors may limit brand expressionMOQSmall runs have higher conversion costCombine orders or select stock sizesHigher MOQ requires inventory planningBox structureCompartments and complex folds use more materialReview whether every feature is necessarySimplification may reduce meal separationFreight modeAir freight has a much higher landed costPlan sea freight replenishment earlySea freight requires longer forecasting horizonThe most reliable buying method is to request quotations in comparable terms: identical size, material, coating, print coverage, carton quantity, Incoterm, lead time, and documentation package. This prevents a low quotation from hiding a thinner board, different barrier, or reduced quality-control scope.Supplier change control protects buyers from unapproved changes in paper source, coating type, grammage, adhesive, ink, structure, tooling, or production location. This is especially important for compostable takeaway packaging because minor material substitutions can change grease resistance, food-contact status, compostability scope, appearance, and packing strength.A supplier should notify the customer before any material or process change that may influence performance or compliance. The buyer should then review revised documentation, test samples where needed, and issue written approval before the changed product is shipped. Approved samples should be retained by both parties with a clear date, SKU, and specification reference.Batch traceability is also useful. Cartons can carry production date, order number, batch code, quantity, and product reference. When a problem occurs, this information helps identify whether the issue is isolated or system-wide. Independent pre-shipment inspection may be appropriate for major orders, launch programs, or high-risk branded packaging.var ctxSupplier=document.getElementById('supplierComparisonChart').getContext('2d');new Chart(ctxSupplier,{type:'bar',data:{labels:['Documentation','Custom development','Batch control','Testing support','Export service','Lead-time visibility'],datasets:[{label:'Integrated manufacturer',data:[90,88,92,85,91,86],backgroundColor:'#4f8fbd'},{label:'Trading-only source',data:[62,55,58,49,67,60],backgroundColor:'#d4a65a'}]},options:{responsive:false,maintainAspectRatio:false,scales:{y:{beginAtZero:true,max:100,title:{display:true,text:'Illustrative capability index'}}}}});This comparison chart is an illustrative sourcing framework. Buyers should score each candidate supplier using verified evidence, sample results, audit findings, and communication quality rather than relying solely on a supplier category.Fude Packaging supports overseas B2B buyers seeking compostable and paper-based takeout packaging for restaurants, distributors, retailers, takeaway platforms, and food brands. The company’s technical capability includes material selection support, coating recommendations, structural development, artwork and dieline review, Pantone color matching, rapid prototypes, and functional sample testing. Buyers can evaluate white samples, printed samples, or food-application prototypes before mass production.Its manufacturing capability is based on a self-owned 30,000 m² factory in Shandong with automated production lines and an in-house laboratory. Fude Packaging produces food-service packaging categories including paper cups, bowls, burger boxes, kraft lunch boxes, salad containers, noodle boxes, trays, and multi-compartment meal boxes. This allows buyers to consolidate packaging categories and improve brand consistency. Explore the company’s food container range for suitable formats.For kraft-focused programs, buyers can review disposable kraft paper lunch boxes or assess sustainable kraft paper takeout containers when building a broader packaging assortment.Fude Packaging’s service capability includes destination-market discussion, document coordination, OEM and ODM support, production scheduling, export-ready packing, third-party inspection cooperation, and shipment assistance for sea freight, air freight, full-container, less-than-container, and express samples. With export experience across more than 50 countries, the team can help buyers align product performance, documentation, branding, and logistics needs before ordering.Fude Packaging Support AreaPractical Buyer BenefitTypical DeliverableWhen It Is Most UsefulMaterial recommendationImproves fit between packaging and food menuSuggested fiber, paper, and barrier optionNew product launch or menu changePrototype developmentReduces risk before mass productionWhite sample, printed sample, or functional prototypeCustom size, shape, or lid designIn-house productionSupports process visibility and stable coordinationProduction schedule and inspection workflowMulti-SKU or repeat wholesale ordersQuality testingHelps validate practical performanceInspection records and performance checksHot, greasy, or liquid-containing foodsCompliance coordinationSupports destination-market purchasing filesAvailable material and food-contact documentsDistributor, chain, or retailer approvalsExport serviceSimplifies international order handlingPacking list, invoice, and shipment supportImports to global trade hubs and regional warehousesFor 2026 and beyond, packaging buyers are likely to prioritize verified material transparency, lower-plastic barrier technologies, simpler mono-material designs where practical, digital batch traceability, and packaging specifications aligned with regional waste infrastructure. Regulations and retailer standards will continue to move from broad sustainability language toward documented, use-specific claims. The most resilient procurement programs will combine technical testing, compliant documentation, realistic disposal communication, and reliable repeat supply.var ctxMarket=document.getElementById('marketGrowthChart').getContext('2d');new Chart(ctxMarket,{type:'line',data:{labels:['2022','2023','2024','2025','2026','2027'],datasets:[{label:'Global demand index for fiber-based takeaway boxes',data:[100,113,128,145,163,181],borderColor:'#3c9d7a',backgroundColor:'rgba(60,157,122,0.12)',fill:false,tension:0.3,pointBackgroundColor:'#3c9d7a'}]},options:{responsive:false,maintainAspectRatio:false,scales:{y:{beginAtZero:false,title:{display:true,text:'Demand index (2022 = 100)'}}}}});The line chart presents a realistic directional outlook for global demand, driven by food delivery growth, corporate sustainability targets, single-use packaging restrictions, and restaurant demand for stronger branded takeaway presentation.Ask for the finished-product material specification, applicable compostability certificate or test evidence, certificate scope, current validity, food-contact documentation, and approved environmental claim wording. Also verify that printing, coatings, and product construction match the certified or documented version.The suitable barrier depends on the food, temperature, contact time, and delivery route. Greasy fried foods need strong grease holdout; sauces need reliable seam and bottom protection; steam-heavy meals need resistance to moisture softening. Approve the barrier only after testing filled samples under realistic conditions.Confirm the destination market, whether food is dry, aqueous, acidic, alcoholic, or fatty, the maximum serving temperature, and expected contact duration. The supplier’s documentation should correspond to the intended use, not simply state a general food-contact claim.It depends on local collection and processing infrastructure. A package may be industrially compostable but not accepted by a local municipal program. Check local commercial composting providers, city guidance, and food-service waste contracts before making disposal instructions part of the packaging design.Use a written change-control process requiring advance notification of changes to fiber, paper grammage, coating, adhesive, ink, tooling, or manufacturing process. Require updated documents and sample approval when a change could affect performance, compliance, or environmental claims.A first order should include an approved sample reference, detailed SKU specification, artwork approval, carton packing requirement, production lead time, inspection standard, document list, Incoterm, payment terms, and procedure for handling confirmed quality issues.Not always, but certified materials, specialized barriers, custom printing, and lower order quantities can add cost. Buyers should compare total landed cost, including product failures, waste, freight utilization, compliance risk, and customer experience, rather than comparing unit price alone.